In this guide 6 sections
Laser, plasma and waterjet each need different job records. Track material and thickness limits first, then cut time, consumables, edge finish and nesting yield. Laser is judged on gas and lens wear, plasma on consumables and bevel, waterjet on abrasive and slow cutting speed. Quote each method on its own numbers.
One shared record, three different drivers
Every cutting job needs the same core fields. Material grade, thickness, sheet size, quantity, cut length and pierce count. Those fit all three methods.
The cost drivers differ. A laser job runs on assist gas, power and nozzle life. A plasma job runs on electrodes, nozzles and shields. A waterjet job runs on abrasive garnet, pump hours and orifice wear.
If one quote template treats them alike, one method will always be priced wrong.
Material and thickness limits decide the method first
Laser handles thin and medium sheet cleanly, and it struggles with highly reflective metals unless the machine is built for them. Plasma cuts thick conductive plate quickly and rough. Waterjet cuts nearly anything, including stone, glass and composites, without heat.
So the job record must show the material and thickness before any price appears. A planner who sees thirty millimetre plate on a fibre laser job should get a warning, not a quote.
Keep a table of each machine’s limits. Maximum thickness by material, bed size and any gas needed. Check the job against it at order entry.
- Material grade and thickness
- Maximum thickness per machine
- Bed size against sheet size
- Assist gas or abrasive needed
Cut time and consumables set the real cost
Cut time is not cut length divided by a speed. Pierces add time, corners slow the head, and thick sections slow everything. Record the actual machine time per job and compare it with the estimate.
Consumables wear with use, so log them against the job. Count lens or nozzle changes on a laser, electrode and nozzle sets on plasma, and garnet by the kilo on a waterjet. After a month the average cost per hour is no longer a guess.
Waterjet is slow, so machine hours dominate its quote. Plasma is fast, so consumables and rework dominate.
- Pierce count and cut length
- Actual machine hours against estimate
- Nozzle, electrode or garnet used
- Gas or water consumption
Edge finish and nesting yield change what the customer gets
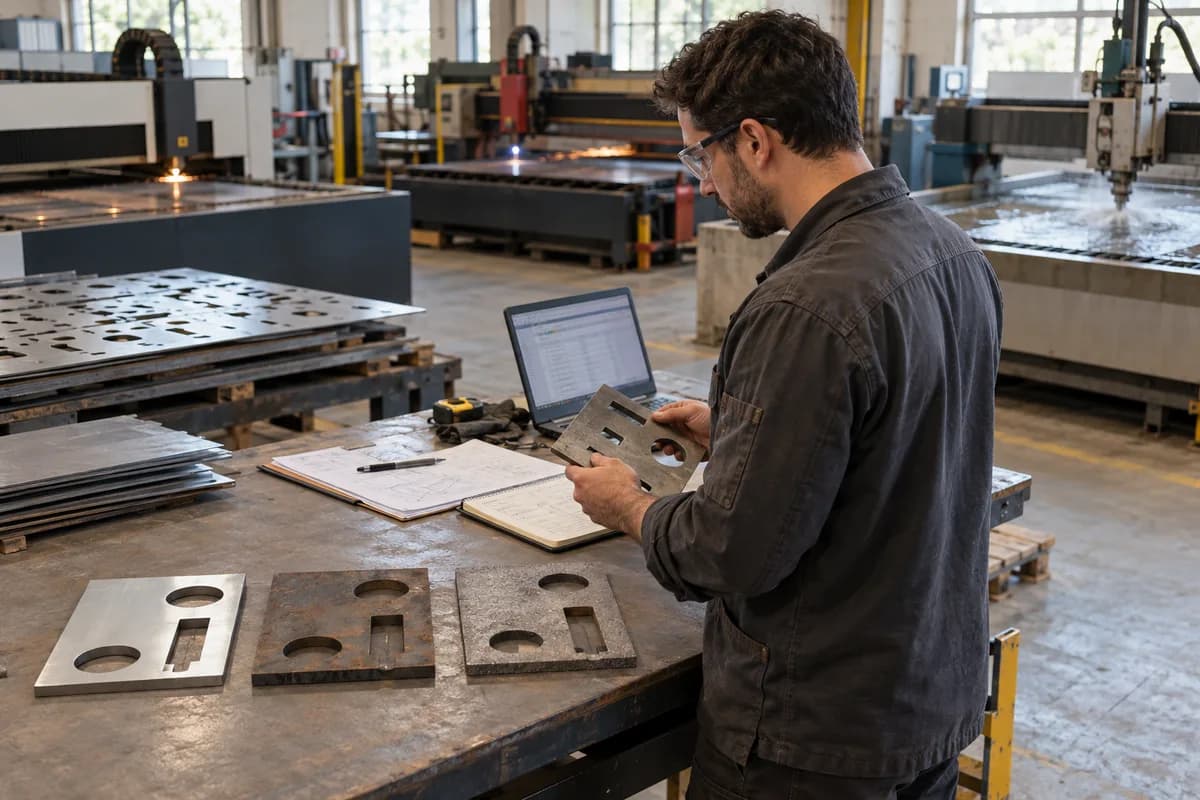
Each method leaves a different edge. Laser gives a narrow kerf and a clean edge. Plasma leaves a bevel and dross that may need grinding. Waterjet gives a matte, frosted edge with no heat-affected zone.
Record the finish the customer expects and any secondary operation, such as deburring or edge grinding. That time belongs on the job card, not in the shop’s overhead.
Nesting yield is the other lever. A tight nest saves sheet, but plasma needs wider spacing for its kerf and bevel. Log the yield per sheet and the offcuts returned to stock.
Quote with the numbers you tracked
Once each method has its own history, quoting changes. You stop quoting a flat rate per metre and start quoting machine time, consumables, material at the nested yield and finishing.
Compare the quote with the actual on every job for a month. The gap tells you which method you underprice.
Next step. Pull the last ten finished jobs and check whether their records hold pierce count, machine hours and consumable use.
Cutting method comparison sheet
One sheet split into laser, plasma and waterjet columns. Rows cover maximum thickness, bed size, assist gas or abrasive, typical edge finish, consumables to log, secondary operations and quoting basis. The last row is left blank for any job where the method was changed, and the reason.
Open a blank worksheet to printQuestions owners ask
Which cutting method is cheapest per part?
It depends on thickness, material and quantity. Thin sheet in volume usually suits laser, thick plate suits plasma and mixed or heat-sensitive material suits waterjet. Compare actual job costs, not machine prices.
Do all three methods need the same job card?
They need the same core fields, but consumables and finishing differ. Keep one card with method-specific blocks so the right wear items are logged for each machine.
How do I track consumables per job?
Log a change event when a nozzle, electrode, lens or garnet batch is replaced, and tie it to the machine hours since the last change. Then spread the cost over the jobs in that period.
Why does nesting yield matter for quotes?
Material is often the largest cost on a cut job. If your quote assumes a better yield than the nest delivers, the shortfall comes straight out of margin.