In this guide 6 sections
Split press waste into three counts per job: make-ready, trim and rejects. Have the operator log each at the machine with a reason code. Compare against the allowance in the estimate while the job runs, so a bad start is caught before it becomes a month-end write-off.
One waste number hides three problems
Most plants record a single spoilage figure. It sits in the stock ledger and is reconciled at month end. By then the operator, the job and the cause have all been forgotten. Nobody remembers.
That one figure mixes three different things. Make-ready is material used to set colour, register and tension before good product flows. Trim is edge material cut off by design. Rejects are finished product that fails a check.
Make-ready belongs to the setup routine. Trim belongs to the estimator who chose the web width. Rejects belong to whoever watches viscosity, register and the doctor blade during the run. Lumping them together hides all three. Split them.
Define each count so everyone means the same
Agree the definitions in writing and post them beside the press, next to the changeover checklist and the sample board. Make-ready ends when the first approved sample is signed. Everything before that is make-ready. Simple. Everything after, if scrapped, is a reject.
Trim is the planned difference between the web or sheet width and the finished width. It should come from the estimate, not from the operator’s guess. Rejects need a reason from a short fixed list.
A short list beats a long one. Operators will pick the first reason on the list if there are twenty. Keep it short.
- Make-ready: start to first signed sample
- Trim: planned edge or slit loss
- Reject: failed after approval
- Returned: caught at finishing or by the customer
Capture counts at the machine
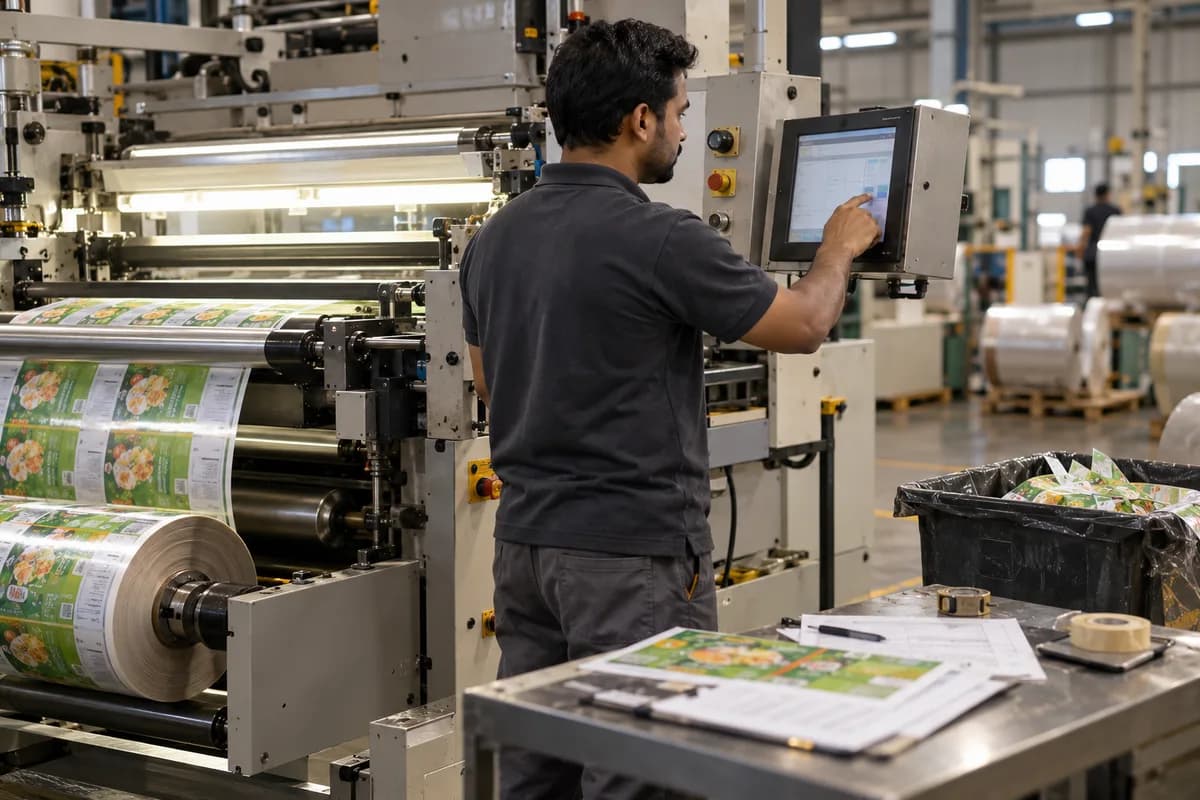
Counts must be entered as they happen. A tablet bolted near the press works if it takes only a few taps, even with ink on the operator’s gloves. A paper sheet keyed in when the crew hands over is better than nothing, but the entries get rounded to tidy numbers.
Record metres, sheets or kilograms, whichever the plant buys by. Link every entry to the job number, the machine and the operator. Add the reason code for rejects and the colour or unit that caused the stop.
On slitter rewinders and laminators, counting metres of scrap is awkward, so weigh the bin. A weight per job per shift is crude but comparable.
- Job, machine and operator
- Quantity in the unit you buy by
- Reason code from a short list
- Time of entry
Compare to the estimate while the job runs
The estimate included a waste allowance. Put it on the job card as a number the operator can see. If make-ready on a flexo job has already passed the allowance by the third colour, the supervisor knows now. That is the point. Anilox, plate mounting and ink viscosity can all be checked before the run ends.
Review make-ready by job type, not by machine alone. A seven colour pouch job on laminated film cannot be compared with a two colour paper label. Over time you will see which structures, substrates and customers consume more.
Use the data in quotes. If a particular film always needs extra setup, the allowance was wrong and the job lost money before it began.
Review weekly and act on the top reason
Hold a short weekly review with the press supervisor. Take the single largest reason code and decide one action. It might be a registration check, a new anilox roll, a viscosity routine or a change in how reels are loaded.
Check the result next week. Keep the report layout fixed. One action, one owner.
Stop writing waste off as a lump at the month end. Post it to the job, so the margin on every order shows what really happened.
Press waste log
A one-page log for each shift. Columns are job number, machine, operator, make-ready quantity, trim quantity, reject quantity, reason code and time. A top block lists the estimate allowance for the job and a bottom block totals the three counts and shows the largest reason for the shift.
Open a blank worksheet to printQuestions owners ask
Is some make-ready waste unavoidable?
Yes. Every job needs setup material. The aim is to know how much each job type uses and to stop it creeping up unseen.
Who should enter the counts?
The operator at the machine, at the time. A supervisor keying them later tends to round them.
How many reason codes are enough?
Keep to about six to eight. Fewer is better. A short list gets used. A long one gets ignored.
What if we weigh scrap instead of counting?
Weigh by bin per job per shift. Crude, but comparable. It is less exact but still lets you compare jobs and spot a rise.