In this guide 6 sections
Give every rejected piece one reason code, picked from a short list grouped by stage: setup, tool wear, material, handling and inspection. Record it with the machine, tool and lot at the bin. Within weeks, the counts show which cause deserves action first.
A scrap count tells you how much, not why
Most plants record rejection as one number, written down when the shift closes. Forty pieces went to the red bin. The figure goes into a register. Nobody reads it again. Over a quarter, the same dull question comes back each time scrap rises: was it the setup, the tool, the bar or the trolley?
At the monthly review the quality head holds a total and no cause, while operators blame the material, stores blame the operators and the tool crib blames the setter. Everyone has a story. Nobody has a record. That is the gap.
A reason code fixes this by forcing one decision at the bin. The answer is a code, not a sentence, so it can be counted and sorted when the review comes round.
- Scrap quantity by shift and machine
- Reason for each rejection, picked from a list
- Operation where the fault was found
- Operation where the fault was caused
Group the codes by stage, then keep the list short
Start with five groups and no more than six codes under each. Sixty codes never get used. Operators tick the first one that looks close, and the data turns to noise. Name codes in the shop’s own words, such as offset drift or chipped insert, not in abstract labels like process error.
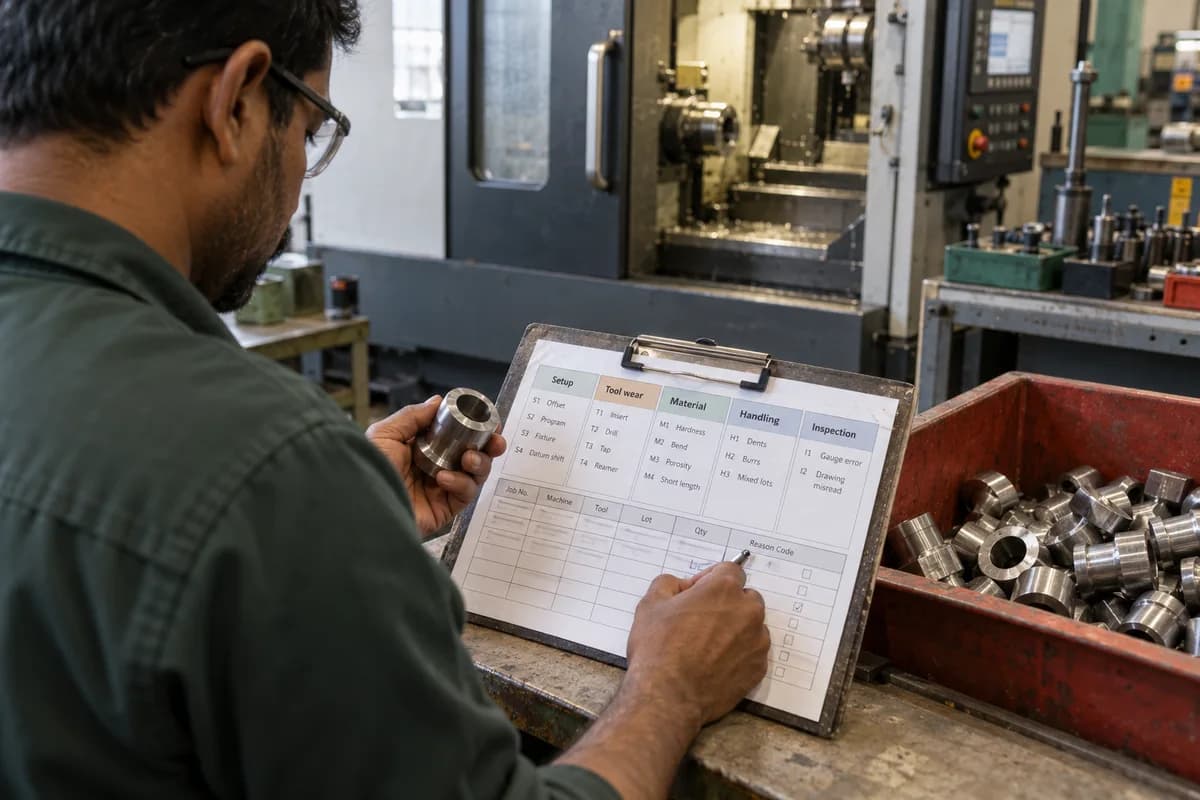
Setup covers first-piece offset, wrong program, wrong fixture and datum shift after a restart. Tool wear covers a worn insert, a broken drill and an undersize tap. Material covers hardness out of range, bent bar, short length and casting porosity.
Handling covers trolley dents, deburring burrs and mixed lots in one tray. Inspection covers a gauge out of calibration or a drawing misread. That is the whole list.
- Setup: offset, program, fixture, datum shift
- Tool wear: insert, drill, tap, reamer
- Material: hardness, bend, porosity, short length
- Handling: dents, burrs, mixed lots
- Inspection: gauge error, drawing misread
Capture the code where the piece is rejected
Write the code at the bin, never from memory in the evening. A tick sheet clipped to the machine works. So does a tablet with six large buttons. A rejected piece that sits in a mixed bin is a lost clue, so keep one bin per machine and empty it at every shift change.
Each entry carries job number, machine, operator, tool number, material lot and quantity. That is a lot for gloved hands, so let the job card fill in machine and job automatically. Keep tool number and lot as ticks.
Add one code nobody should use often: unknown. If it climbs, either the list is missing a cause or the operator is being rushed.
Read the pattern weekly, not monthly
Sort the week’s rejection by reason code, then by machine, then by tool. Two or three combinations usually carry most of the loss. One tired boring bar on one lathe can explain a full page of the register.
Show the chart to setters and operators, because they often know the fix already and what they lacked was proof that the problem repeats. A good week of data may need only fifteen minutes with the setter and the inspector at the machine.
Mark the cause by where it was created. A burr found at final inspection but made at deburring belongs to deburring.
- Top three codes this week
- Machine and tool behind each code
- Supplier lot behind each material code
- Change made and next week’s result
Review the codes every quarter
Codes drift. A new vendor brings a new defect, and a retired machine leaves behind codes nobody touches. Once a quarter, delete the dead ones and split any code that catches too much.
Keep retired codes readable. Last year’s chart must still make sense. Print the list on one page and fix it beside every rejection bin this week. Ask the purchase team to join the review when material codes lead the chart, because a hardness problem often traces to one mill certificate or one supplier lot.
Rejection reason code sheet
One printed page with five columns, one per stage: setup, tool wear, material, handling and inspection. Each column lists up to six codes with a short number and a plain label. Below sits a tick table with rows for job number, machine, tool, lot and quantity, plus a weekly summary strip for the top three codes.
Open a blank worksheet to printQuestions owners ask
How many reason codes are enough?
Start with about twenty-five across five stage groups. Fewer hides causes. More than thirty leads operators to guess, and a code nobody understands is worse than none. Review the list after one quarter with the setters present.
Who should choose the code?
The person who rejects the piece, usually the operator or the inspector. A supervisor can correct obvious errors later, but the first choice must come from the bin, where the piece and its fault are still in front of someone.
Can this work on paper?
Yes. A tick sheet beside the bin is enough to start. Software helps once the weekly sorting by machine, tool and lot becomes too slow by hand.
What if two causes apply?
Pick the one that happened first. If a worn insert and a loose fixture both contributed, record the earlier fault and mention the second in a note field.