In this guide 6 sections
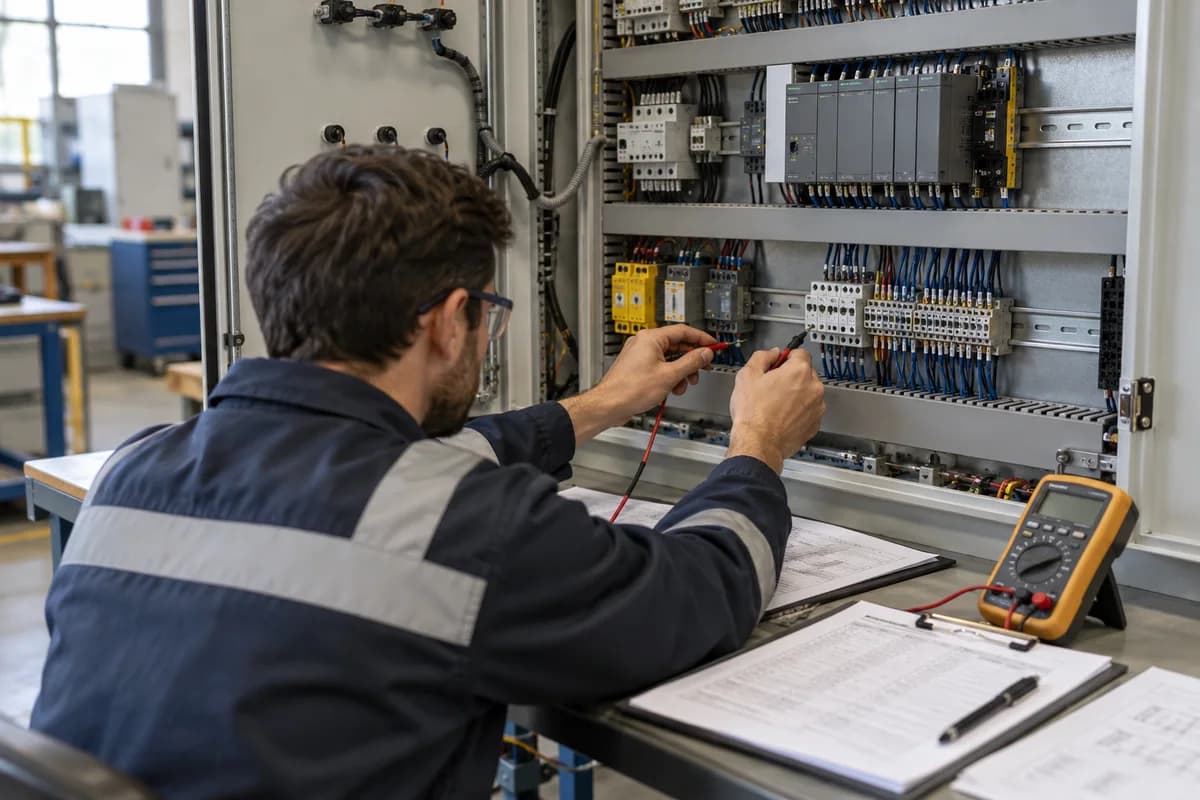
A factory acceptance test checks a PLC panel against its drawings, then earth continuity, insulation resistance, every I/O point and every safety function, with every reading recorded. Record deviations before anyone signs. Keep the instrument serial numbers and calibration dates with the readings, because an auditor may ask for them long after the panel ships.
Start with the visual and document check
Before any power goes on, compare the panel with the released drawings, check the enclosure rating and cable entries, then read part codes against the BOM.
Sample wire numbers, ferrules and terminal labels, then inspect crimps and torque marks on power terminals, where a loose lug on a main breaker overheats under load. Easy to miss. Shut doors hide loose lugs.
Have the paperwork ready, meaning schematics at the correct revision, the I/O list and the programme backup, all laid out on the test bench before the first reading. A test that starts without the right drawing revision wastes the witness’s day, so confirm every document is present before anyone opens a meter.
- Enclosure rating, finish and nameplate
- Device part codes against the BOM
- Wire numbers, ferrules and torque marks
- Door lock, gland plates and gaskets
- Drawing revision on the test sheet
Test protective earth and insulation
Measure earth continuity between the main earth bar and each exposed metal part, including the door, back plate and gland plate, recording every reading against the instrument used.
Run the insulation resistance test between live conductors and earth after you disconnect or protect the PLC power supply and analogue cards, since the megger voltage can damage them. Note the test voltage on the sheet.
Write the result, not a tick. A tick tells the customer’s auditor nothing about whether the value sat close to the limit, and the auditor may ask for the numbers a year later.
Power up and check every I/O point
Power up in stages. Check the incoming supply, then the control supply, then the PLC, and read the diagnostic buffer, since a module can show green while logging a configuration warning. Fault lights mean stop.
Go point by point through the I/O list, forcing each input with a switch until it changes in the programme, then drive each output and watch its relay.
Analogue channels need a signal source, so inject low, middle and high values and read the scaled result on the HMI to confirm the range matches the transmitter datasheet.
- Each digital input against the I/O list
- Each output with relay or lamp response
- Analogue scaling at low, middle and high
- Communication links to drives and HMI
- Drive start, stop and fault reset
Prove the safety functions
Safety circuits deserve their own pass. Test each emergency stop and confirm the contactors drop out, then test the door interlocks, light curtain inputs and the safety relay reset, skipping none of them. Press each emergency stop while the drives are running, because a stop that works on an idle panel proves little about the loaded machine.
Try to break them. A reset held down while a stop is pressed should restart nothing, and one channel pulled from a dual channel input must fault the safety relay. Perfect-day circuits are not safe.
Record who ran each test and what the result was, because an inspector asks for safety records first after an incident and will read them as a stranger. Exact entries protect you.
Record deviations and collect the signature
Every failed point gets a line in the deviation list, noting the fault, the fix, who fixed it and the retest result. Never erase a failure. Retest each failed point only after the fix is dated and initialled by the person who made it, so the sheet shows the whole story from fault to clearance.
When the list is clear, the customer’s witness and your quality lead sign the sheet, and you attach readings, the I/O sheet and programme backup as one pack.
Turn this list into a printable sheet with columns for expected, actual and initials, run it on the next panel off the line, and refine it afterwards.
PLC panel FAT record sheet
Page one of this two page sheet holds the job header, drawing revision, and instrument list with calibration dates, plus space for the customer’s witness name. Page two is a table of check, expected result, actual result, pass or fail and initials, grouped as visual, earth, insulation, I/O, safety and communications. Signatures close the sheet.
Open a blank worksheet to printQuestions owners ask
What is a factory acceptance test?
It is a formal check at the builder’s works, where the panel must match its drawings and work as specified before it ships, often with the customer watching. Nothing ships before it passes.
Who should attend the FAT?
The test engineer, the quality lead and the customer’s witness attend, and you add a controls programmer when the test includes the programme logic or communications.
How is FAT different from site acceptance?
FAT runs at your workshop with simulated loads, while site acceptance runs after installation with the real machine, field wiring and process, so it finds problems FAT cannot.
Which standards apply to panel testing?
That depends on the country and panel type, so check the assembly standard, such as IEC 61439 for low-voltage assemblies, and ask your quality lead which test values apply.