In this guide 6 sections
Auditors ask a machine shop for calibration records, inspection results, nonconformance reports with corrective action, and traceability from material cert to shipped part. AS9100 adds configuration control and stricter record retention. Capturing these on the job as it runs is easier than rebuilding them before the audit.
Calibration and measuring equipment
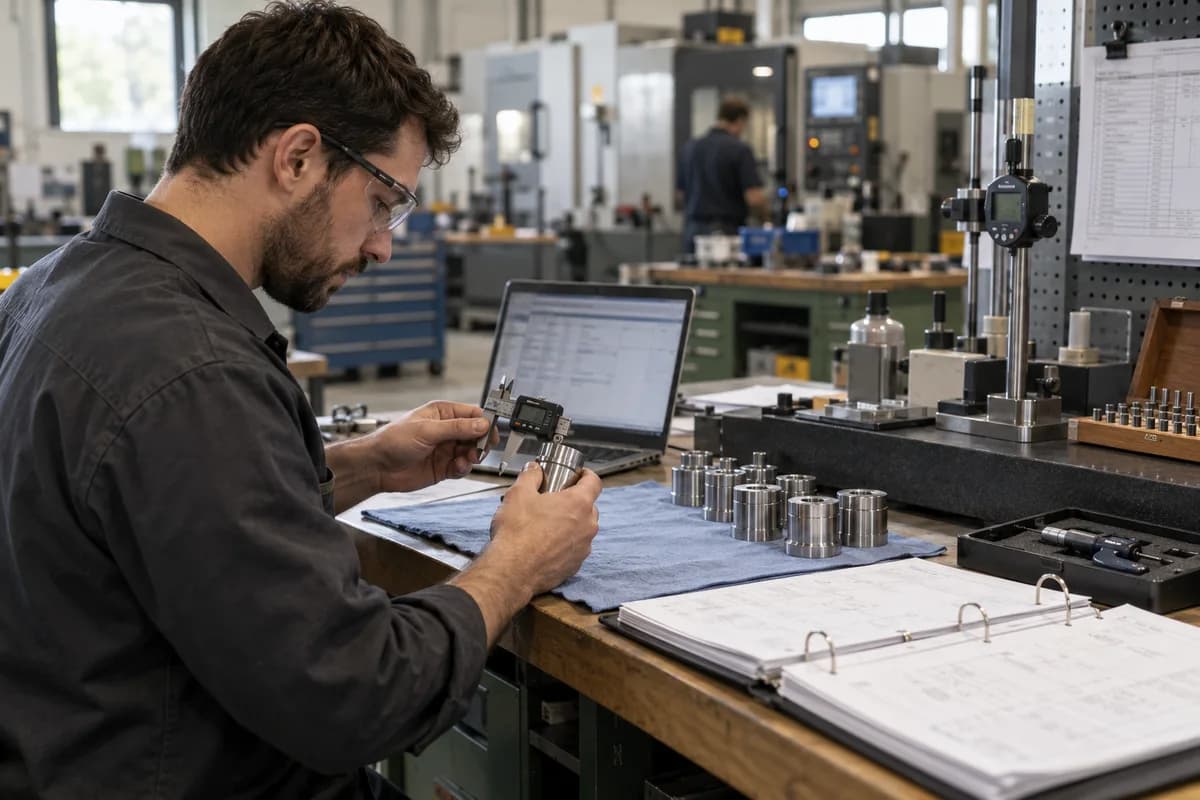
Every gauge that accepts or rejects a part needs an identity, a calibration due date and a certificate. Micrometers, bore gauges, thread rings, height gauges and the CMM all count, and so do torque wrenches used in assembly.
The auditor will pick a gauge from the inspection bench and ask for its record. They will also ask what you did about parts measured with a gauge later found out of tolerance. Shops forget that one.
- Gauge ID, type, range and location
- Last and next calibration dates
- Certificate with traceable reference
- Out of tolerance action and parts affected
Inspection and process records
Records of first article inspection, in-process checks and final inspection show that the drawing was met. For each one the auditor wants the drawing revision, the measured values, who measured them, and with which gauge.
AS9100 customers often add first article reports in a set format. Keep dimensional results as numbers, not ticks, so a trend appears before parts drift out of tolerance and into the scrap bin.
Link every sheet to the job. Add the part serial or batch. Gauge selection matters as well. A caliper cannot prove a tolerance of a few microns, and an auditor will notice the mismatch between the drawing and the instrument named on the sheet.
Nonconformance and corrective action
When a part fails, a nonconformance report records what, where, how many and the decision: scrap, rework, use as is with approval, or return to supplier. Whoever made that decision signs it and dates it.
Corrective action goes further, because it asks why the fault happened and what stops it recurring. A report that says operator error and closes is the kind an auditor reopens.
Check that each report links to the job, the machine, the program and the material lot. Customer complaints and supplier rejects follow the same path. Keep them in one register, so repeat faults on one material or one vendor stand out.
Traceability from material to shipment
For each shipped lot the shop should show the material certificate, the heat number, the operations performed, the people and machines involved, and any outside processing with its certificate. Aerospace customers may ask years later.
Retention periods vary by customer and by standard, so read your contract clauses and your certification body’s guidance rather than assuming. Records must stay readable and retrievable for the whole period.
Paper travellers fade. Files saved to a desktop vanish with the machine.
- Material cert and lot number per job
- Special process certificates for plating or heat treatment
- Operator and machine per operation
- Certificate of conformance and delivery note
Let the job supply the records
Most of these records are by-products of work already happening. A job record that holds the drawing issue, routing, bookings, measurements and material lot gives the auditor a single trail.
Software helps by forcing fields at the right step, such as refusing a booking without a gauge ID. It also keeps closed records locked, with every edit logged against a name.
Run a mock trace before the audit. Pick a shipped part and time how long its full history takes to produce. Fix the gaps, then trace a different part.
Audit records readiness checklist
A checklist on one page, in four blocks: calibration, inspection, nonconformance and traceability. Each row names a record, where it is kept, who owns it, the retention period you have set and the date you last sampled it. A final row logs the result of a mock trace on one shipped part, including how long the trace took and which record was missing.
Open a blank worksheet to printQuestions owners ask
Is AS9100 just ISO 9001 with extras?
It builds on the same quality management base and adds aerospace requirements such as configuration management, risk handling and product safety. Check the standard text for the exact clauses.
Can electronic records satisfy an auditor?
Generally yes, if they are controlled, backed up, access limited and retrievable. Ask your certification body how it treats signatures and edits to closed records.
How far back must records go?
It depends on the standard, your customer contracts and local law. Ask each key customer, then write the longest period into your procedure.
What do auditors find most often?
Out of date calibration, inspection sheets not linked to a job, and nonconformances closed without a root cause. A monthly sample check catches all three.