In this guide 6 sections
Give every jig, die and fixture its own ID and a card that holds usage count, rated life, repair history, location and the customer who owns it. Update the count at each job close, set a review trigger before the limit, and record every move out of the shop.
Treat each tool as an asset with a life
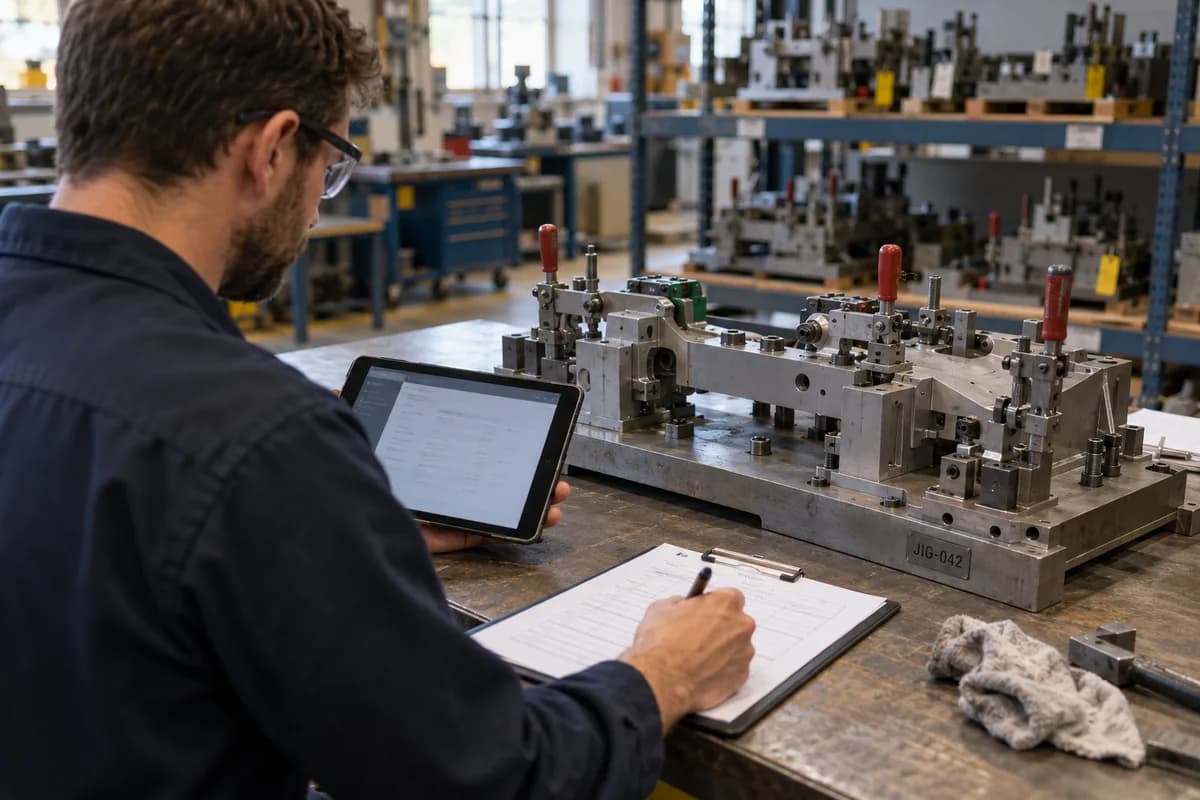
A drilling jig for a wing rib bracket has a bush wear limit, a last inspection date and a customer who paid for it. It is not a consumable. Yet many shops know it only by a rack number and a name on masking tape, with no wear count and no owner recorded anywhere.
Give each tool a permanent engraved ID or riveted metal tag, and link it to the part number it makes, its drawing revision and the funding purchase order.
Then decide what ends its life: for a stamping die it might be hit count, for a fixture a flatness drift, and for a gauge a calibration due date. Write that limit on the card.
- Tool ID and engraved tag
- Part number and drawing revision served
- Customer owner and funding PO
- Rated life and the wear signal that ends it
Count usage where the work is closed
Do not rely on memory. The reliable place is the job close, where a finished batch of two hundred brackets on the progressive die raises the die’s hit count by two hundred.
Do the same for fixtures with a cycle count, and for tools tied to hours, such as a form block in an oven. Never mix units on one card.
Set a warning at a fixed share of rated life, so the regrind or replacement is planned before a die cracks mid-order and costs a delivery date. Plan the regrind early.
Keep repair and rework history on the same card
Note the date, the fitter, what was changed and the first-off inspection result for every regrind, bush change, shim adjustment or weld repair. Be exact every time.
History answers the question of why a part started drifting, because a locating pin replaced three jobs ago and an out-of-tolerance first-off point straight at the cause.
Repairs reveal weak tools. A fixture sent to the weld bay five times in a year is telling you to retire it, rebuild it or ask the airframe customer to fund a replacement.
- Date, repair type and who carried it out
- Dimensions checked after the repair
- Cost and whether the customer was billed
- Next inspection due
Know where every tool is and whose it is
Customer-owned tooling must be identified, protected and returned on request, so a fixture on loan from an airframe maker should never sit beside your own go/no-go gauges.
Use location codes such as rack and bay, on machine, out for repair, at customer and at subcontractor, and update the code at every single move. A die shown at a plating subcontractor for ninety days should raise a question about whether anyone is chasing it or has simply forgotten where it went.
Record every dispatch with a gate pass and a return date, so at audit you can show the tool, owner, count and last check on one page.
- Location code updated at each move
- Gate pass for every outward movement
- Customer ownership flag on the card
- Annual physical check against the register
A first step for your shop
Pick the ten tools that run the most revenue, build a card for each with the fields above and fill in whatever you know today. Write TBC, not a guess.
Add the count at job close for those ten, and after a month you will see which tools sit nearest their limit and which have vanished from their racks.
Then widen the register. Go one part family at a time.
Tool life and ownership card
A one-page card per tool. The top block holds tool ID, description, drawing revision, owner and funding PO. A middle table shows rated life, current count and warning level. A repair log has columns for date, work done, post-repair check and sign-off. A movement strip lists location, gate pass number and return date.
Open a blank worksheet to printQuestions owners ask
What is the difference between tool life and calibration due?
Tool life is wear from use, counted in hits, cycles or hours. Calibration due is a date-based check of a measuring device. A shop needs both on the record.
Who owns the tooling we build for a customer?
Ownership depends on the contract and purchase order. Record the answer on the card at the start, so storage, insurance and return rules follow the agreement.
How do we stop tools going missing?
Give each an ID, a location code and a gate pass for any outward move. A periodic physical check against the register catches strays early.
Can usage counts come from the machine?
Some machines report cycle counts directly. Where they do not, book the quantity at job close and add it to the tool’s count.