In this guide 6 sections
A good CNC shop ERP never retypes a job. It holds the drawing revision, programme, route, machine hours, inspection results and delivery note against one job number, so the invoice matches what was cut and checked. Quote to invoice is one chain. Everything hangs from one number.
A quote that becomes the job
Take a 6061 aluminium bracket. Forty pieces, drawing revision C. The quote already holds the bar size, the cycle time estimate, the anodising vendor and lead time, all of which should flow forward when the purchase order lands. Nothing gets retyped.
If the shop retypes it, the numbers drift. The job card shows a different quantity from the order, or a note about anodising never reaches the floor, and nobody finds out until the parts are late.
Store the customer’s drawing and purchase order number on the quote, since those two items settle most of the arguments that come later, and keep the email thread.
- Customer drawing with revision letter
- Material grade and bar or plate size
- Estimated setup and cycle time per operation
- Outside processes and the vendor for each
- Promised delivery date
Programme and route held together
Planning builds a route of saw cut, turning, milling, deburr, wash, inspection, anodise and final check, with each step naming a machine group and a planned time. Every step carries the job number.
The G-code programme belongs to that route, not to a folder on someone’s desktop, and a programmer posts each file against the job and the revision. At the Haas or the Doosan, the operator pulls that file and nothing else, so a stale programme cannot reach the spindle.
Fixture numbers and tool lists sit here too. A repeat job a year later should not begin with a hunt for the right vise jaws or the offsets written on a lost sticky note. Look it up.
Machine time recorded as it happens
The floor must report a job started, paused or finished, and either a tablet at the cell or a barcode scan on the traveller will do it.
Capture setup minutes apart from run minutes. Keep them separate. Capture scrap pieces with a reason code such as tool break or wrong offset, because those figures decide what the next quote should say about a similar part.
One report matters most. Planned against actual hours, operation by operation, shows the real bottleneck, whether that is the five axis machine, the wire cutter or the single inspector who is busy.
- Setup start and end
- Run start and end by operator
- Pieces good and pieces scrapped
- Scrap reason
- Machine or cell used
Inspection that releases the work
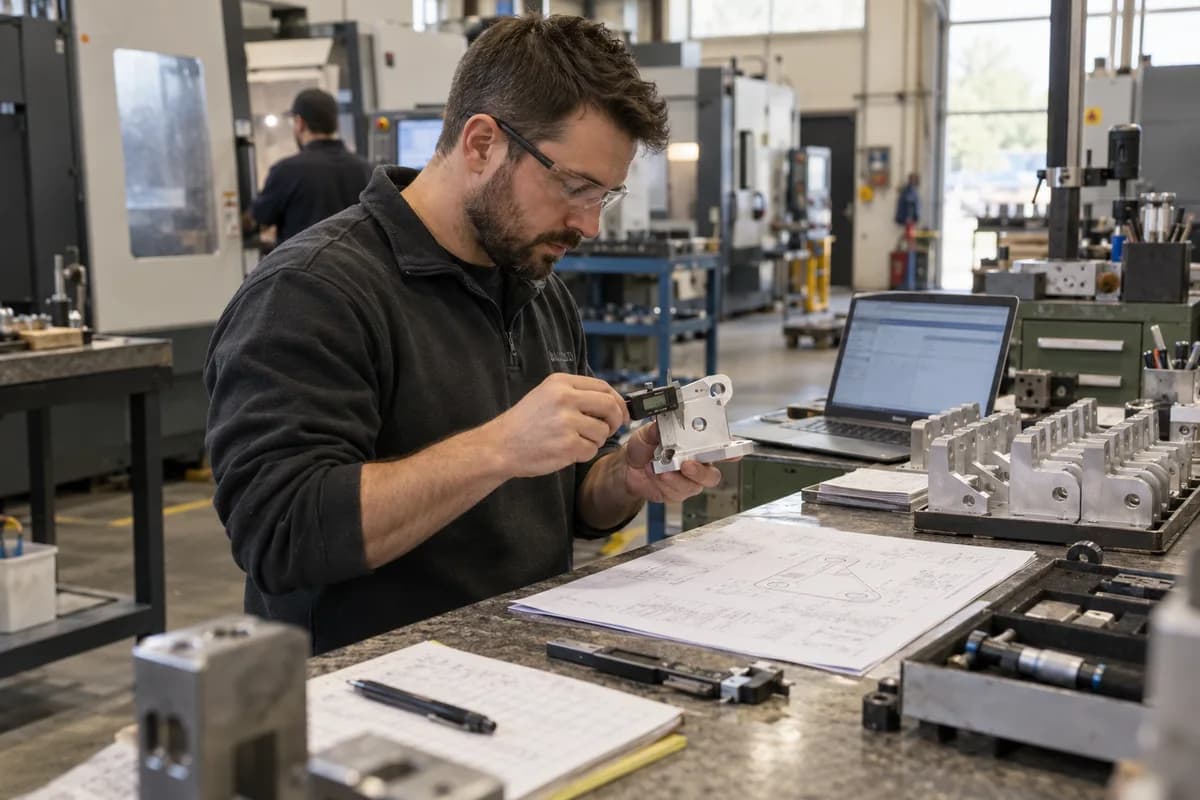
Every route carries at least one inspection step. Name the gauges and the sampling plan, measure the first piece against the balloons on the drawing, and key in results or read them from a CMM export.
A job must not leave for anodising, plating or packing until the inspector signs the release, and that rule belongs in the system, never in a supervisor’s memory.
Keep every certificate on the job. Aerospace and medical customers ask for the full pack of material, plating and heat treat certificates, and gathering it afterwards from three inboxes is slow, error-prone work.
Delivery note, invoice and the closing review
The delivery note should pull its quantity from the inspection release, not from the order, so if thirty eight of forty pieces passed, thirty eight ship. The balance stays open. Rework or a replacement lot closes it.
The invoice follows. It is built from the delivery note. Partial shipments, rework and extra operations show up as lines instead of phone calls, and the customer’s accounts team can match each line to a purchase order.
At close, compare quoted hours with actual hours. Write down the three biggest gaps, whether a tool break, a late fixture or a slow anodiser, and feed them into the next estimate.
Quote to delivery job record
The job record fits on one page. Six blocks cover quote, order, route, machine log, inspection and delivery, and each block lists its fields, such as drawing revision, programme file, setup minutes and scrap reason. Ticks show what you hold now.
Open a blank worksheet to printQuestions owners ask
Can a small CNC shop run an ERP without a planner?
Yes, when routes stay short. The owner or a lead hand releases each job from the morning list, and the machine log doubles as the schedule that shows which spindle is free. Add a planner only when work in progress outgrows a whiteboard and jobs start waiting unnoticed between the saw, the mill and the wash tank.
Does the ERP need to link to CNC machines?
Not at first. Start with scans. Manual start and stop scans give usable hours. Machine data links make sense later, once the job records are trusted, the floor scans out of habit, and controller hours can be checked against manual ones.
Where do tool life and tool cost belong?
On the operation, as a tool list. Add a changeover note for inserts and holders. Cost per tool then feeds the estimate, so a titanium job quotes differently from a mild steel one, because inserts wear faster and the cycle runs slower.
How do we handle rework on a closed job?
Reopen the job for rework. Do not clone it. Cloning splits the history. Open a rework operation on the same job number with its own scrap reason and hours, so the cost stays with the original order. Quote reviews stay honest.