In this guide 6 sections
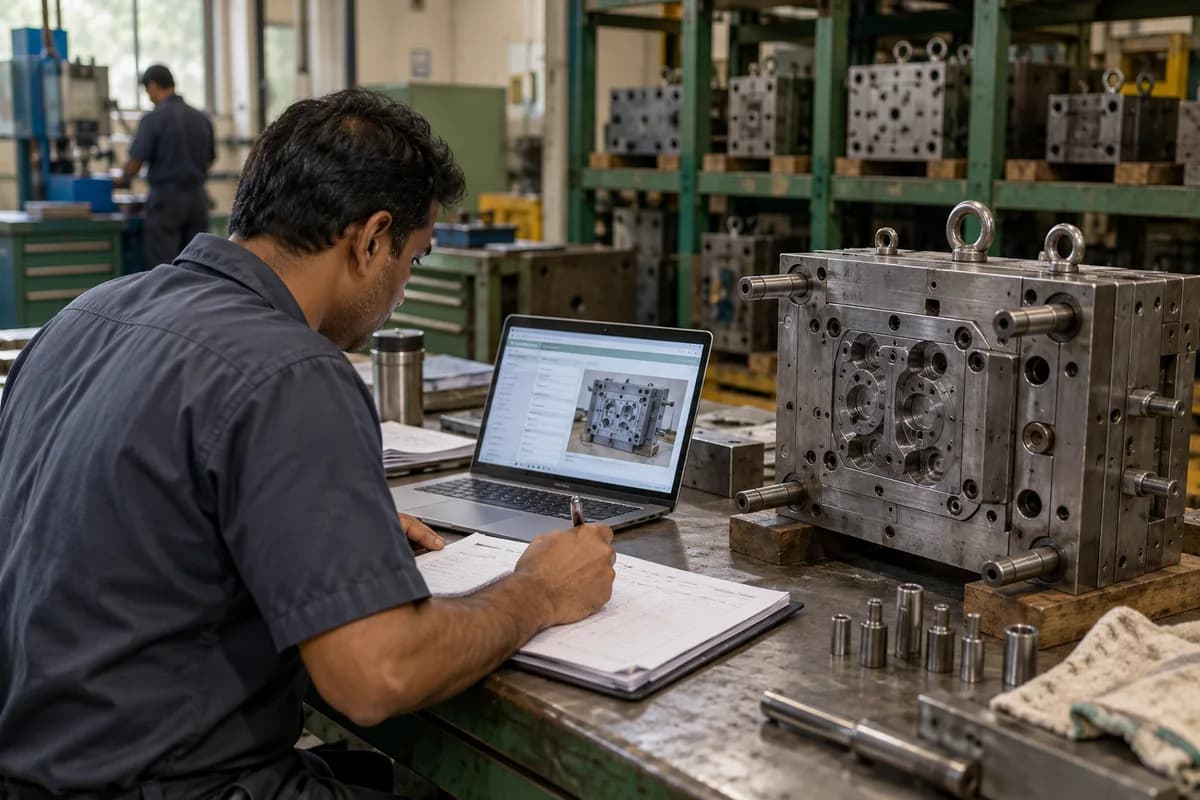
One tool gets one file. A mould master record holds cavities, steel and hardness, hot runner details, standard cycle and press tonnage, then adds shot weight, maintenance history, storage location and part numbers. That way planners, setters and the tool room all read one set of facts and stop arguing over which version of a cavity count is current.
One tool, one record
Every mould gets a permanent ID. Stamp it on the plate and write it on the record before the tool ever reaches a press, even when it arrives from a customer. Customers change part numbers. Tools move between presses. The mould ID stays put.
The record answers daily questions. Where is the tool? Which presses can run it? How many cavities are open? When was it last cleaned?
If those answers live in three notebooks, a spare drawer and a manager’s memory, then you have no master record yet, only a habit of asking around.
Physical details that never change
Start with the steel and the size. The planner needs these facts to pick a press, the setter needs them to choose a lifting method, and the tool room needs them to plan a repair.
Add the maker, the year, the quoted tool life, the customer who owns it and the drawing number, since ownership matters the day a customer asks to move it. Send history, spares and settings together.
- Cavity count and layout
- Core and cavity steel with hardness
- Hot runner brand, drops and zone count
- Gate type and runner weight
- Shut height, plate size and weight
- Clamp tonnage needed
Process facts that guide the planner
Record the standard cycle time, shot weight, resin grade and drying time, and note the approved press along with any press that is banned for the tool. A mould that fits a 150 tonne machine on paper may still flash on one with a worn tie bar, so the ban list matters.
Keep the setter’s notes here too, covering water line connections, ejector stroke and the core pull sequence, because a night shift setter would otherwise guess. Nobody enjoys that phone call.
Do not copy full process sheets into the record, but link to the latest approved one, so nobody runs the tool from an outdated copy.
Maintenance and life of the tool
Log every repair, polish, weld and replaced insert with the date and the shot count at that time, and note the preventive service interval and the next one due.
Shot count is the honest clock. Hot runner tips, ejector pins and slide wear all follow it, while calendar dates mislead when a tool sits idle for four months and then runs flat out.
Mould steel does not complain. A tool with a rising repair frequency and a falling cavity yield is telling you something, and the record shows that pattern before the customer does. It also gives the tool room a fair case for a rebuild budget, backed by repair dates and shot counts instead of opinion.
- Total shots and shots since last service
- Repair history with cause
- Cavity blocks and spare inserts on hand
- Rust prevention and storage condition
Links to parts, orders and your first record
Connect the mould to every part it makes, with the resin grade and the customer’s drawing revision for each, including family tools that mould several items at once. Link open orders too. A planner then sees the demand before the press is booked and can spot two orders that need the same tool in the same week.
Begin with your ten busiest tools. Walk to each one, read the plate, fill the form and photograph the cavity block, which takes a morning per tool, mostly spent hunting for the old drawing. Repair slips hide under wrong customers.
Once those ten are right, the habit spreads along the rack, and setters start asking why a tool has no record, which is exactly the change you wanted. Review the oldest tools last. Their paperwork is the thinnest.
Mould master record template
This is a two page form. Page one has blocks for identity, physical details, process facts and storage location, plus a photo box that holds a picture of the cavity plate. Page two has a repair log table with date, shot count, work done and who signed it off, plus a list of parts moulded and the presses approved. A sign-off line names the last checker.
Open a blank worksheet to printQuestions owners ask
Who owns the mould master record?
The tool room manager usually owns it. The planner reads it daily, and one person should approve every change so that two different versions of the cavity count never exist side by side.
Is a mould master record the same as a mould drawing?
No, they answer different questions. The drawing shows how the tool was built, while the record shows how it behaves in production, how often it needs work and which parts it makes. Keep the drawing number on the record.
Should customer owned tools sit in the same record?
Yes, with an ownership field. You need the same history for those tools, and the customer will ask for it when a tool is audited, repaired elsewhere or transferred to another moulder.
How do we count shots reliably?
Operators reset press counters. Capture the count at each setup and at each service, and let the system add up the difference so a reset never erases the tool’s history.