Business solutions for Medical device manufacturers
Explore software for work such as “Diagnostic imaging equipment”. Review each business function below, including when it fits and what to check before implementation.
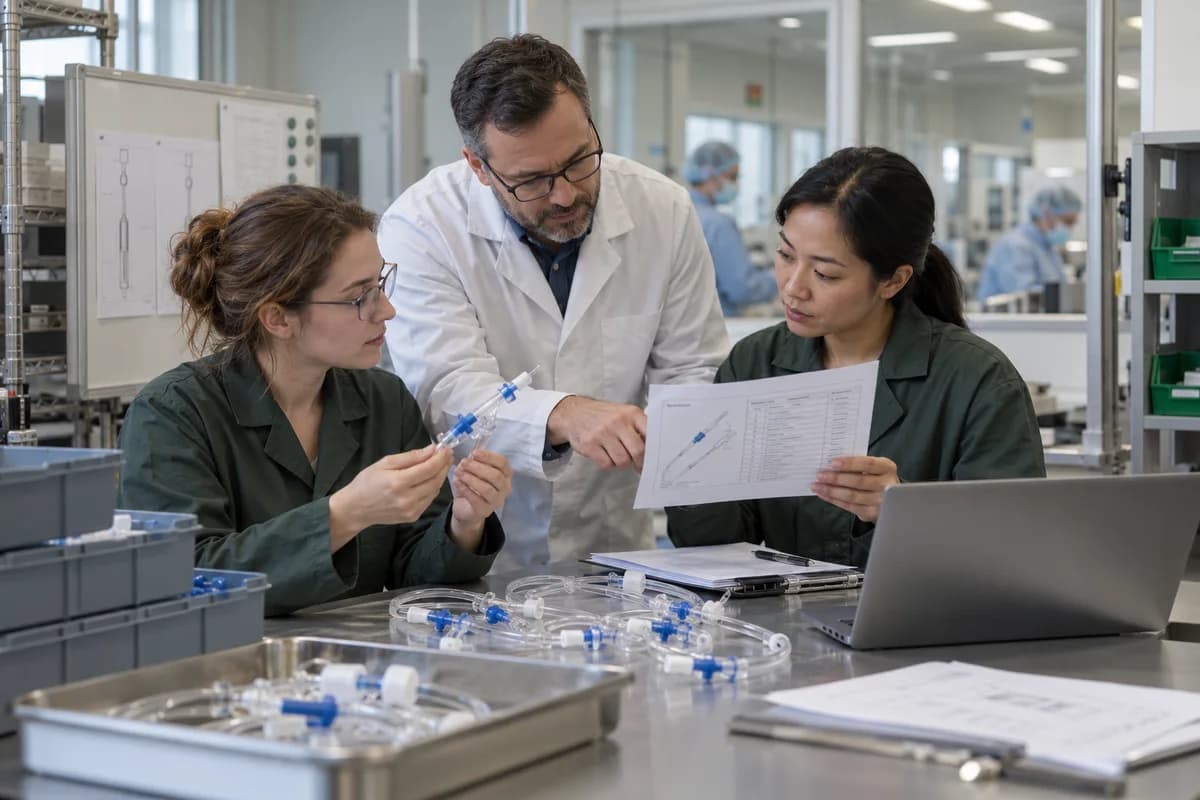
How the business operates.
Medical device plants make everything from single-use syringes and catheters to electronic patient monitors. The product differs, but the records they must keep look alike: component lots, routing steps, inspection results, UDI labels, sterilisation certificates, shipments and complaints.
The records that hold the operation together.
- Quotations and price lists. Build quotations for devices, accessories and contract runs from your own price lists, with quantity breaks, mould tooling charges and every revision kept for the customer file.
- Bills of materials with revision history. Hold each device as a list of components with quantities, a revision letter and an effective date. A new revision replaces the old one on the floor from that date.
- Production orders and routings. Release a production order for each lot with its routing, press, mould cavity, extrusion line, operator and planned date. Record each step as it finishes, with the cleanroom area and the equipment used.
- Lot, serial and UDI records. Number every component lot and finished lot, assign serial numbers where needed, and hold label data including UDI-DI and UDI-PI fields. Trace a device forwards to hospitals or backwards to resin. One search does both.
- Incoming, in-process and final inspection for device lots. Set an inspection plan for each part and device, with sampling levels, lumen and torque limits, particulate counts, seal peel strength and acceptance limits. Record measurements and pass or fail results. A failed lot is held from release.
- Complaints and corrective actions. Log each complaint with its lot and investigate it. Assign a corrective and preventive action with an owner, record any biocompatibility query, and close it with an approval and a trend by device and cause.
- Controlled documents and approvals. Keep procedures, work instructions, specifications and validation protocols with revision numbers, reviewers and approval dates. Floor staff open the current copy, while superseded sheets are withdrawn from every workstation.
- Supplier approval and purchasing. Hold the approved supplier list with audit dates, quality agreements and certificates. Raise purchase orders only to approved sources, and compare rates and delivery record across moulders, pouch printers and resin vendors.
Operational bottlenecks to check
Trace records live in separate files
Goods receipts, production sheets and shipping lists sit in different places, so a trace from one finished device to its resin batch or circuit board means opening each of them. An audit day stretches.
Old revisions stay in circulation
A device master record is updated, but a printed copy of the earlier bill of materials stays at a workstation. Parts are built to the wrong list. Rework follows.
Inspection forms are filed away from the lot
Signed torque, leak and dimensional checks are stored in binders by date, so finding the result for one lot months later takes a search through boxes.
Complaints and actions are tracked apart
A complaint arrives by email, while the investigation and the CAPA are written in other documents. Closure then depends on memory, and the nonconformance report is filed separately.
Supplier approval lapses unnoticed
Audit dates, quality agreements and sterilisation certificates sit with one person, so purchasing can raise an order to a source whose approval has expired. Nobody sees it until an auditor asks.
Follow the work across teams.
This is a planning flow. Confirm the steps, owners and approval rules against your actual operation.
Roles and responsibility boundaries.
Reports your managers need.
- Lot trace from finished device to component lots and shipments
- Production orders by status, machine and due date
- Inspection results and failures by part and supplier
- Complaints by device, cause and closure status
- Corrective actions open, overdue and closed
- Supplier approval status and certificate expiry
- Stock of components and finished goods by location
Connections to scope
- SMS
- WhatsApp and other messaging
- Barcode and label printers
- Accounting software export
- Spreadsheet import
Confirm data access, record ownership and the exchange method for each connection. Inclusion here does not mean every connection is available in a standard package.
Setup decisions and adoption risks.
Use these requirements to plan phases, data migration and user training. Agree the release sequence after reviewing your current systems.
Limitations to settle before implementation
- A distributor that only buys and resells finished devices needs stock and invoicing more than production records.
- A hospital or clinic that only uses devices, not makes them, is better served by Hospital Operations Management Software.
Modules to consider first.
These functions connect to the operating model above. Confirm each one against the work your business actually runs.
Choose the operation you want to improve.
Use these activities to explain your scope. Your business does not need every function in the directory.
- Diagnostic imaging equipment
- Surgical instruments
- Patient monitoring devices
- Disposable and single-use devices
- Hospital furniture and fixtures
- In-vitro diagnostic kits
- Export and international distributor deals
- Government and institutional tenders
Explore the business functions.
Production, stock, fleet and recurring billing functions apply only where your business runs those activities. Read the suitability conditions on each page.
Manufacturing
Batch and Serial Tracking
Trace goods using batch identifiers or individual serial numbers.
View workflow and suitability →Bill of Materials
Define the materials and quantities needed for a manufactured item.
View workflow and suitability →Job Work Management
Track material sent to an outside processor and returned after work.
View workflow and suitability →Quality Control
Record specified inspections and the disposition of checked goods.
View workflow and suitability →Work Order Management
Track a production job from material issue to completed output.
View workflow and suitability →
Human Resources
Helpdesk
Procurement
Start with the problem your team can describe.
Bring a sample record and show where information is copied, missed or waiting for approval. Scope the first useful change from there.
What happens after you share your requirements
- We review your brief and the systems you already use.
- We clarify the workflow, missing information and the work to consider first.
- The proposed scope sets out the deliverables, responsibilities and dependencies.
- Review the scope and commercial terms before deciding whether to proceed.
Start with your requirements
Describe your current process, the people involved and the change you need. Start with the details you know; we can clarify the rest together.
Share your requirements