Business solutions for Metal stamping companies
Explore software for work such as “Brackets, clips and covers for auto plants”. Review each business function below, including when it fits and what to check before implementation.
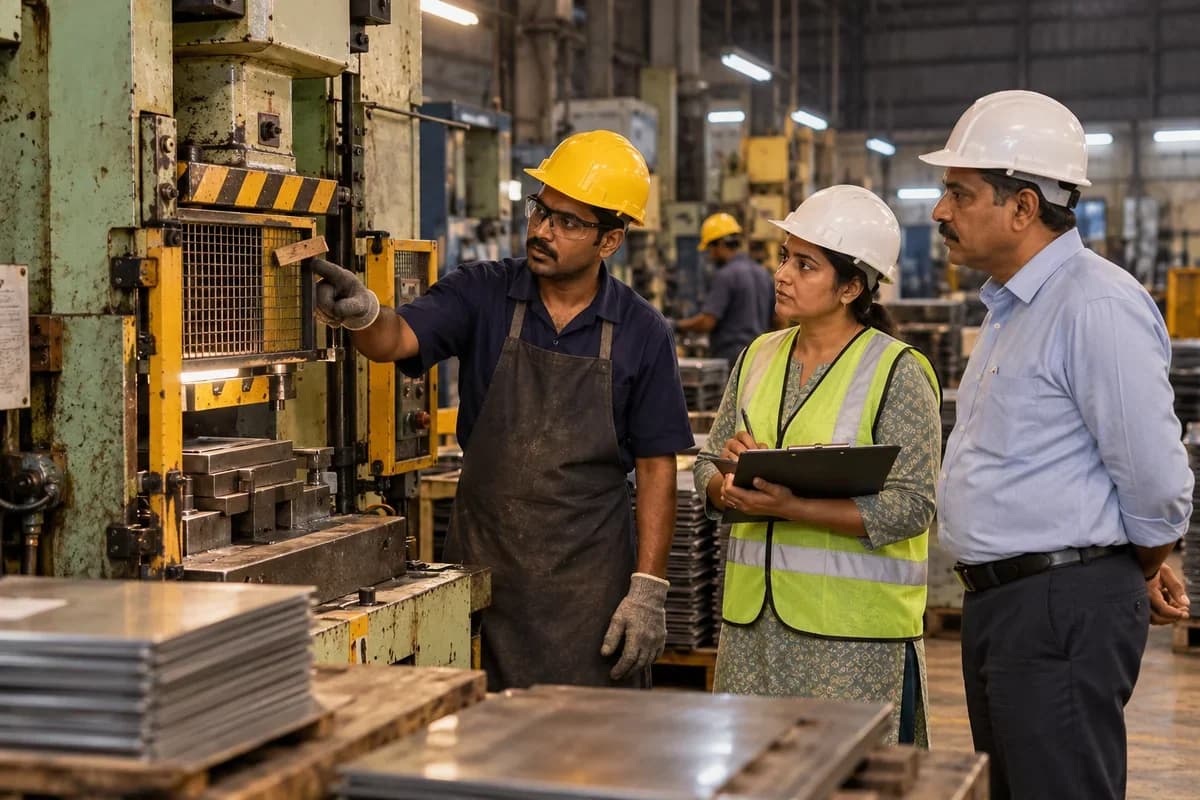
How the business operates.
A press stamps thousands of parts an hour using a die built for one part. A chipped punch leaves burrs on the bracket. A worn die button does the same. A coil from the wrong heat splits the flange of a deep drawn cup.
The records that hold the operation together.
- Enquiries and drawing revisions. Log each enquiry with drawing, material grade and annual volume. Keep drawing revisions with the part, and link each die to the revision it was cut for.
- Quotation by strip pitch and tonnage. Price from strip width, pitch, material weight and tonnage. A die funded by the customer is quoted as its own line, while one funded by you is spread across each blank sold.
- Blanket orders and call-offs. Hold the standing order with its total. Release each call-off against it, and read the open balance without adding up delivery notes by hand.
- Coil receipt and lot trace. Book coils in with grade, thickness, width, weight and heat number. Each coil links to the runs and bins that consumed it, so a cracked heat is chased to the exact bins.
- Die register and stroke counter. Hold every die with its bay, compatible presses, strokes since regrind and repair history, including punch, die button and spring changes. Dies close to the limit your toolroom set are flagged to the planner before the next run.
- Press schedule and changeover. Plan runs by press tonnage and bed size. Sequence them by die to cut changeovers, and keep every customer call-off covered while the bolster plates are swapped.
- First-off and in-process checks. The setter signs off the first piece. Later burr, hole and flatness readings sit under that same run, so an auditor reads one record instead of three clipboards.
- Tooling cost recovery. Track the die’s cost against parts shipped. A customer-paid or amortised tool is closed out on a date read from the shipments, with the surcharge per part shown on each invoice.
Operational bottlenecks to check
Die life is judged by sound and burr height
A punch is sharpened when the operator decides the burrs look bad. Nobody knows the stroke count. Wear is found late, mid run.
Coil lots are not tied to finished parts
A split appears in one bin of brackets and the mill names the coil, yet no record shows which other bins were blanked from it. The customer’s recall sweeps in far more parts than needed.
Call-offs and press time do not line up
The customer changes the weekly quantity by phone. The press already carries another die. The planner hears last.
Tooling cost recovery is untracked
A die was paid for in instalments added to every part shipped. Nobody checks whether recovery is complete, so the customer overpays or the shop absorbs the balance.
Scrap skeleton is sold by weight with no reconciliation
Strip offcuts leave the yard by weighbridge ticket. The weight is never compared to coil issued and parts shipped, so loss from pilot holes and carrier web goes unseen.
Follow the work across teams.
This is a planning flow. Confirm the steps, owners and approval rules against your actual operation.
Roles and responsibility boundaries.
Reports your managers need.
- Press hours and good parts per hour, by press and die
- Strokes since regrind, by die
- Coil lots consumed and the runs they fed
- Call-offs due, shipped and still open per customer
- Tooling cost recovered against parts shipped
- Skeleton and reject weight against coil issued
- Outside process lots with vendor and days away
Connections to scope
- SMS
- WhatsApp or other messaging
- Barcode scanner
- Accounting export
- Spreadsheet import
Confirm data access, record ownership and the exchange method for each connection. Inclusion here does not mean every connection is available in a standard package.
Setup decisions and adoption risks.
Use these requirements to plan phases, data migration and user training. Agree the release sequence after reviewing your current systems.
Limitations to settle before implementation
- A shop with a single small press and no dies of its own can manage with a job book.
- Sheet metal fabricators, laser cutting and CNC bending shops form flat parts differently and have their own products.
Modules to consider first.
These functions connect to the operating model above. Confirm each one against the work your business actually runs.
Choose the operation you want to improve.
Use these activities to explain your scope. Your business does not need every function in the directory.
- Brackets, clips and covers for auto plants
- Progressive die parts in high volume
- Deep drawn components
- Electrical terminals and laminations
- Appliance sheet metal parts
- Press parts with welding and plating added
- Second-vendor approval with auto buyers
- Die maintenance and repair as a service
- Export stamped components
Explore the business functions.
Production, stock, fleet and recurring billing functions apply only where your business runs those activities. Read the suitability conditions on each page.
Manufacturing
Batch and Serial Tracking
Trace goods using batch identifiers or individual serial numbers.
View workflow and suitability →Job Work Management
Track material sent to an outside processor and returned after work.
View workflow and suitability →Production Planning
Plan manufacturing quantities against demand, materials and capacity.
View workflow and suitability →Quality Control
Record specified inspections and the disposition of checked goods.
View workflow and suitability →
Assets and Fleet
CRM
Inventory Management
Start with the problem your team can describe.
Bring a sample record and show where information is copied, missed or waiting for approval. Scope the first useful change from there.
What happens after you share your requirements
- We review your brief and the systems you already use.
- We clarify the workflow, missing information and the work to consider first.
- The proposed scope sets out the deliverables, responsibilities and dependencies.
- Review the scope and commercial terms before deciding whether to proceed.
Start with your requirements
Describe your current process, the people involved and the change you need. Start with the details you know; we can clarify the rest together.
Share your requirements