In this guide 6 sections
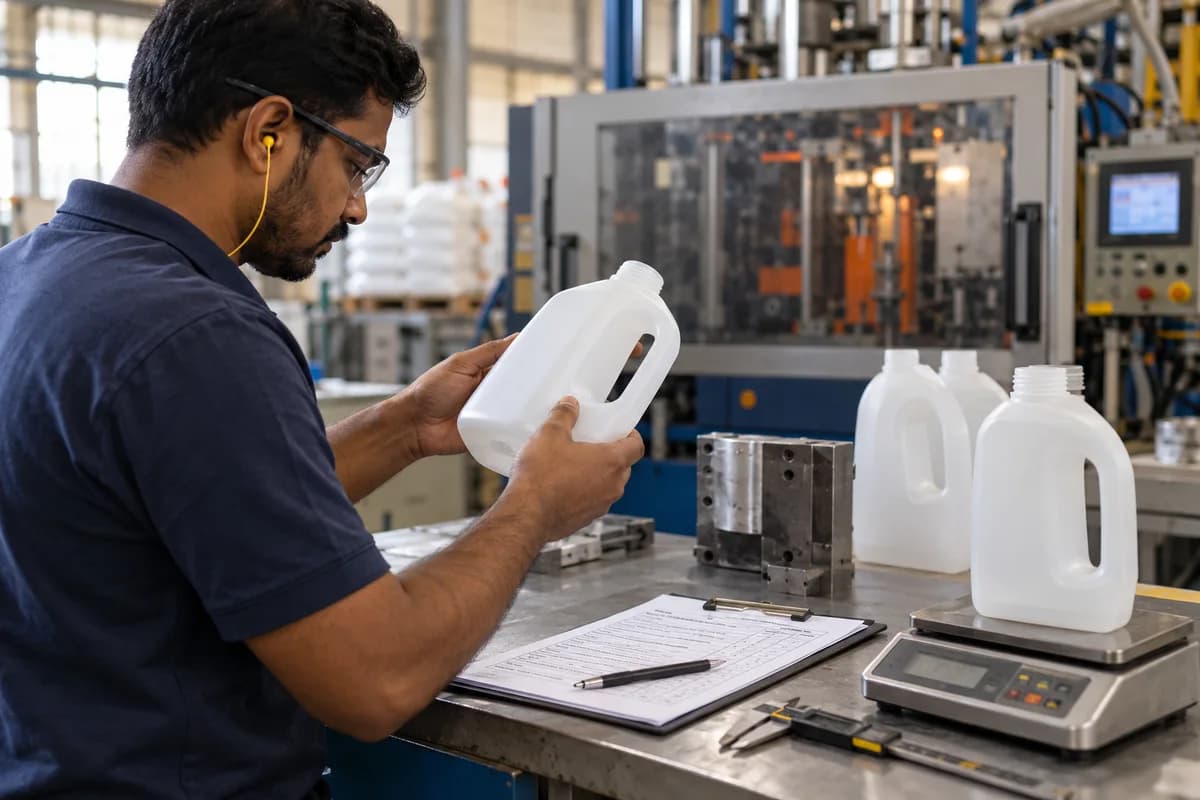
Log every blow moulding reject with its defect, mould cavity, parison setting and resin lot. Wall thinning, weight drift and handle defects each point to different settings. After a few weeks of entries, the repeat cause is usually visible without guessing.
Record the defect, not just the count
A tally of rejects per shift tells you the size of the problem. It does not tell you the cause. Ask the operator to pick a defect from a short list at the machine, and to note the mould and the cavity that made it.
Keep the list short enough to use at the machine. Ten or twelve entries cover most bottle, can and drum faults. A free text box invites vague notes. Avoid it.
Add the clock. A reject at the start of a run, after a colour change or near the end of a resin bag points in a different direction each time. The time belongs on the sheet.
- Thin wall or burst on drop test
- Weight high or low against spec
- Handle pinch off or hole
- Neck finish out of tolerance
- Parting line flash
- Pitting, streaks or black specks
Wall thickness and the parison programme
Wall thickness on a blown container depends on the parison. If the programme controller is set wrong, the shoulder or base thins while the middle is fine. Sectioning a sample and measuring at fixed heights shows the pattern.
Write down the die gap, mandrel position and the programme points used on the run. When a thin base returns two weeks later, you can compare the settings that were in place.
Melt temperature matters as well. A colder melt sags less but shows weld lines. A hotter melt sags and thins the top. Record barrel zones when you change them.
Weight drift and what it signals
Each bottle has a target weight and a tolerance. Weigh a few pieces every hour, and chart them against the shot. A slow drop usually points to a worn screw or a filter that is clogging, and a sudden step to a hopper or dryer change.
Heavy bottles waste resin. Light ones fail on drop or top load tests. Both are rejects, and both need the same log entry.
Check the resin lot against weight. Melt flow changes between lots, and a lot at the edge of the specification can move weight without any setting touched.
- Hourly weigh check by cavity
- Melt temperature and screw speed
- Resin lot and melt flow value
- Regrind ratio on the run
Handle defects and pinch off points
Handle bottles fail where the handle meets the body and at the pinch off. A weak handle weld, a hole at the pinch, or a handle that fills short each trace to cooling, blow pressure or mould wear.
Look at the mould before the settings. A worn pinch off blade or a blocked vent shows on one cavity only. If two cavities fail together, the cause is more likely upstream, in the melt or in the blow air supply.
Keep a photo of each handle defect against the entry. A photo of a short fill teaches a new operator faster than a paragraph. Keep them.
Turn the log into a weekly review
Once a week, sort rejects by defect, then by mould, then by resin lot. A defect that follows one cavity is a mould job. A defect that follows a lot is a supplier job. A defect that follows a shift is a training or setpoint job.
Bring the sorted page to the Monday meeting and name one cause for action. Fix it, then watch the next week’s log to see whether it moved.
Begin with a printed checklist at the machine this week. Review it every Friday with the shift leader and keep the sheets in a folder.
Blow moulding reject checklist
A one page checklist for the machine. The top block holds date, machine, mould, cavity, resin lot and regrind share. The middle block lists twelve defect boxes with a tick and a count. The lower block holds parison programme points, die gap, melt temperature and an hourly weight row for each cavity.
Open a blank worksheet to printQuestions owners ask
How often should we weigh bottles?
Hourly is common, and more often during a start up or after a change. Record the weight by cavity so one worn cavity does not hide in the average.
Why do rejects rise after a colour change?
Masterbatch and purge residue can alter melt flow and leave specks or streaks. Log the colour pair and the first hour after each change.
Can software spot the repeat cause for us?
It can sort the log by defect, cavity and lot in seconds. Someone still has to look at the mould or the setting and decide.
Where should the log sit, on paper or on a screen?
Use whichever the operator will fill in at the machine. Paper first is fine, as long as the sheets are keyed or scanned weekly.