In this guide 6 sections
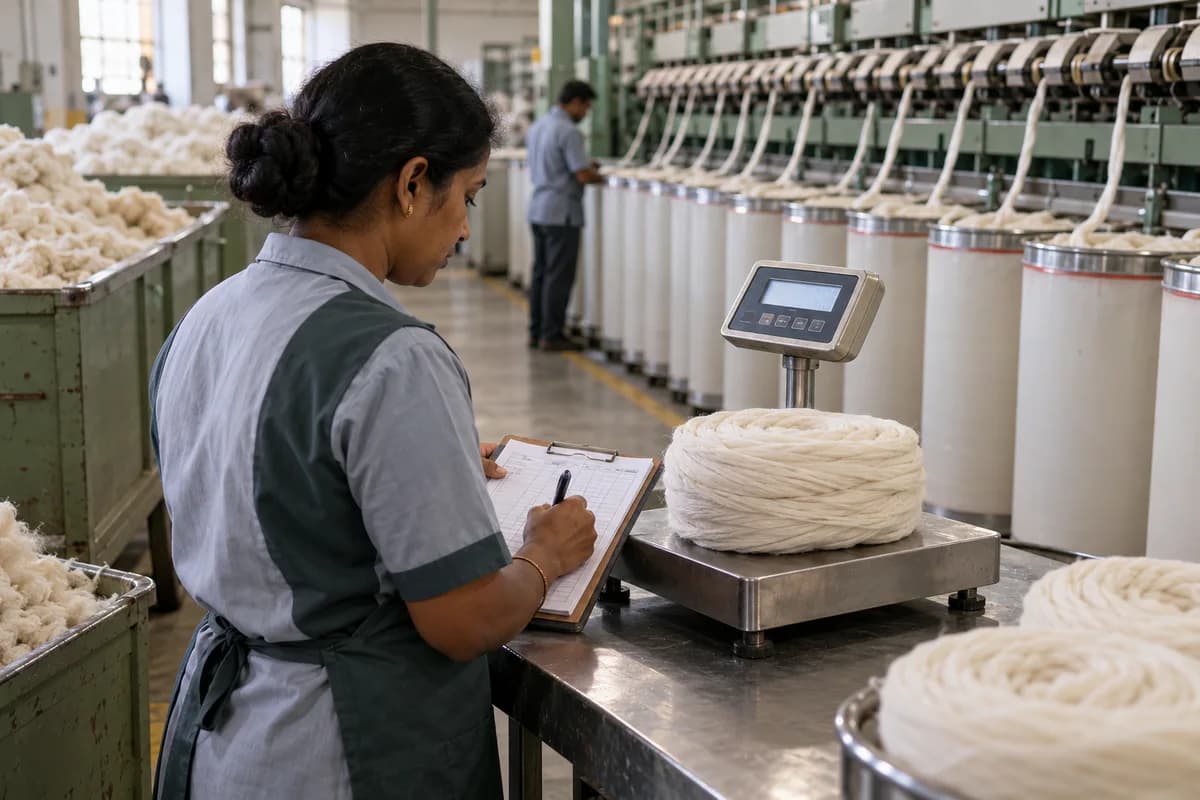
Weigh the material at every hand-off: bale opening, blowroom lap, card sliver, draw frame, roving, ring frame bobbin and cone. Compare each stage with the one before. Gaps that match recorded waste are normal. Gaps that match nothing are unrecorded transfers, wrong tare weights or counting errors.
Why the mill total hides the problem
Most mills compare cotton issued with yarn packed and call the difference process loss. That single figure mixes real waste, moisture change and plain mistakes. It tells you the loss is large. It never tells you where.
A blowroom that sells droppings, a card that makes flat strips and a comber that makes noil all lose weight honestly. A loose bobbin trolley or a misread scale loses weight dishonestly. Both land in the same number.
Split the mill into stages. Each stage gets its own opening weight, closing weight and recorded waste. Only then can you see which hand-off leaks. A mill that issues cotton by the bale but weighs yarn only at the packing table cannot tell a leaking card room from a careless winding shift.
- Bale weight on issue from the godown stack
- Lap or chute feed weight at the blowroom
- Card sliver cans, counted and weighed
- Roving bobbins with tare removed
- Cone weight after winding and clearing
Separate true waste from transfers and counting errors
True waste is material that leaves the line with a name: sweepings, droppings, flat strips, comber noil, roving ends, hard waste at winding. Each has a bin, a weight and a sale or reuse route. Record it the same shift it is made.
Transfers are different. Soft waste fed back into the mixing, sliver moved to another card line, or roving lent to a second shed are all real movements. When nobody records them, the receiving stage looks heavy and the sending stage looks short.
Counting errors come from tare. A bobbin with a wet core, a cone with a heavier paper tube or a can with a different spring plate can shift a whole shift’s weight. Fix the tare per package type and write it on the sheet. Ask the shed supervisors which movements they make by hand during a shift, because the transfers nobody writes down are usually the ones the supervisors remember first.
- Sweepings and droppings from the blowroom
- Flat strips and card fly
- Comber noil and draw frame waste
- Roving ends and bobbin stripping
- Soft waste fed back into the mixing
Weigh at the same points every shift
Pick fixed weighing points and keep them. A scale at the card delivery, one at the roving frame and one at the winding table is enough to start. Calibrate them with a test weight on a set day.
Record the count being run, the lot number and the shift with each weighing. A weight without a count cannot be compared with anything. It is a number, not evidence.
Keep the sheet short. Operators will fill four columns. They will not fill fourteen. Where an operator must carry a bobbin or can to a distant scale, the weighing gets skipped, so place the scale within a few steps of the machine delivery.
Read the stage gaps like a map
Take a single lot and line its stages up in order. Card sliver in, draw frame sliver out, roving out, ring frame yarn out, cone weight out. The gap at each step should sit close to the waste you recorded there.
A gap that is larger than recorded waste points to a transfer or a counting fault. A gap that is smaller can mean waste is being booked twice. Both are worth a walk to the floor.
Check hank roving against the ring frame as well. If the roving hank drifts, the same weight of roving makes less length of yarn, and the cone count looks wrong at the end. When the same gap shows on every lot of one count, suspect the draft or the standard hank. When it moves randomly, suspect tare or shift hand-offs.
- Gap larger than recorded waste: look for unrecorded transfers
- Gap smaller than recorded waste: look for double booking
- Gap that repeats on one shift: check tare and scale
- Gap that repeats on one count: check the draft and hank
Turn weekly weighing into a habit
Review one lot a week with the shed supervisors. Put the stage gaps on one page and ask each person to explain the biggest one. Within a few weeks the same causes show up, and you can fix them in order.
Software helps once the sheet is stable. A system that takes stage entries by lot and count can show every gap without hand calculation. Do not buy it before the weighing points are settled on paper.
This week, pick one lot and weigh it at every stage from blowroom to winding. Write each gap beside its recorded waste. Share the page with the people who run the machines, since they often explain a gap in one sentence that no report would have revealed.
Stage-wise yarn weight reconciliation sheet
A single sheet, one line for each stage: blowroom, card, drawing, roving, ring frame and winding. Columns hold lot number, count, shift, opening weight, closing weight, recorded waste by type, transfers in and out, tare used and the unexplained gap. A last block lists the three largest gaps for the weekly review.
Open a blank worksheet to printQuestions owners ask
What is a normal gap between stages in a spinning mill?
It depends on the fibre, the count and the machines. Your own history by count is the best guide. Track the gap for several lots and treat anything well above your usual range as a prompt to investigate.
Does moisture change explain missing weight?
Partly. Cotton gains or loses moisture with the weather and the humidification setting. Weigh at similar conditions where you can, and note the regain when a sudden shift appears.
Who should do the weighing?
The operator or doffer at each stage, with the supervisor checking one reading per shift. People closest to the material catch mistakes sooner than a clerk reading the sheet the next day.
Can a ledger replace stage weighing?
No. A stock ledger shows what moved between stores. It cannot see inside the process rooms, where most of the unexplained loss sits.