In this guide 6 sections
Casting defects surface late because they are noticed at fettling, machining or the customer’s gate, far from the heat that caused them. Log each defect where it is found, with a cause code such as shrinkage, porosity or sand inclusion, plus heat, pattern and shift. Trends then show within days.
Why a defect appears so far from its cause
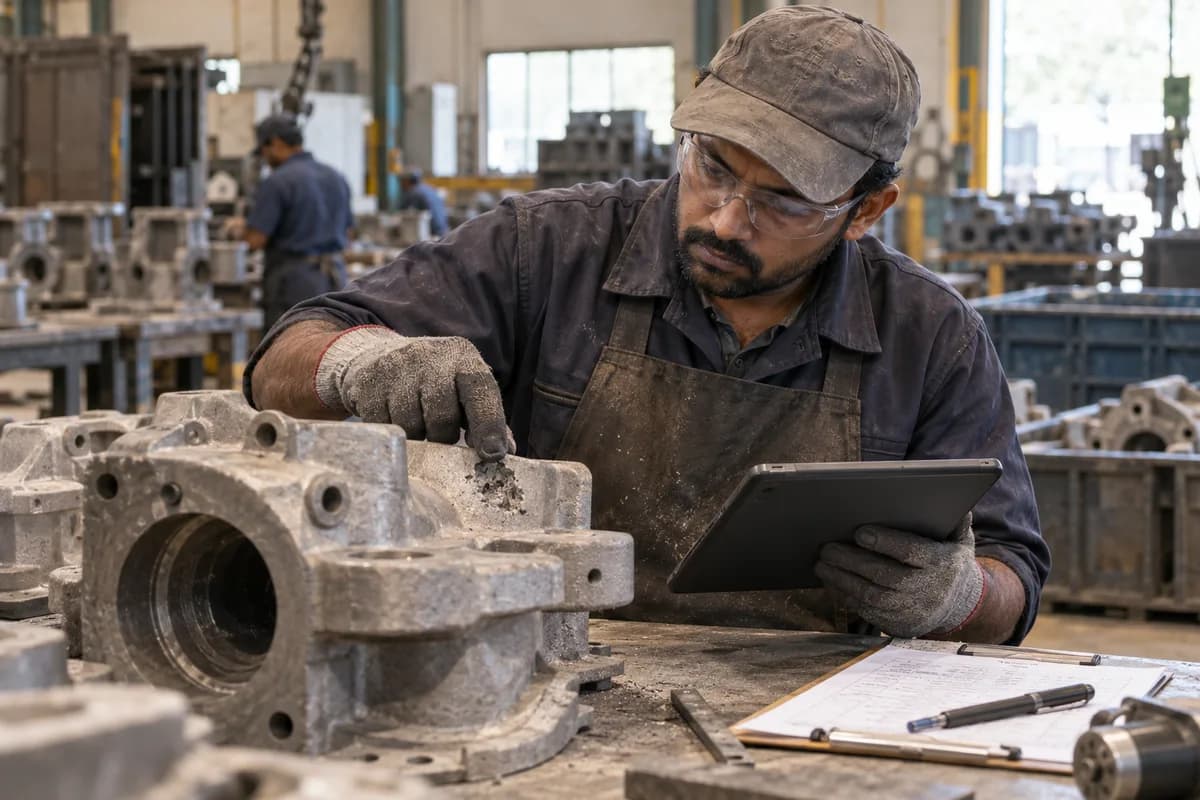
A shrinkage cavity is born in the mould, yet nobody sees it there. It opens when the fettler grinds off a gate, or when the machinist cuts into a boss. Sometimes it waits for the customer’s pressure test.
By then the heat is long finished. The sand has been reclaimed, the melter has changed shift and the pattern is back on the rack. The rejection slip says only bad casting and a part number. Nothing on it points back to a ladle, a mould or a furnace.
Memory fills the gap. The production manager recalls a rough week and blames the sand. Nobody can prove it either way. The next defect then gets the same shrug, and the cause stays buried.
- Pouring and shakeout
- Fettling and grinding
- Machining
- Pressure test or final inspection
- Customer receipt
Log the cause code at the bench where it is found
The person who finds the defect knows most about it. Give that person a short code list: shrinkage, gas porosity, sand inclusion, cold shut, misrun, crack, core shift and dimensional error. Eight or nine codes are enough.
Each entry also carries the casting tag, heat number, pattern or die number, moulding line and shift. The weight of the rejected piece goes in too. Without these fields the code floats free of any cause.
A scanner, a tablet or a laminated card beside the keypad all work. A slip carried to the office for typing later does not. Details are lost on the walk, and the heat number is the first to go. A rejected piece without one is nearly useless for diagnosis.
- Cause code from a fixed list
- Heat number cast on or tagged to the piece
- Pattern, die or core box number
- Station where it was found
- Rejected quantity and weight
Tie every defect to a heat, a pattern and a sand batch
Once entries carry a heat number, pattern number and date, the questions answer themselves. Do porosity rejects cluster on one furnace? Does one pattern throw shrinkage on its thick boss every time? Did inclusions rise after the new binder lot arrived?
Start with a Pareto chart by cause. Then cut it by pattern, by heat and by moulding line. One chart of cause against pattern often exposes a riser or gating fault that shop talk has missed for years. Pair it with the pouring temperature recorded for each heat.
Sand casting, gravity die casting and pressure die casting each show a different mix. Sand work gives inclusions and mould wall movement. Die work gives cold shuts and gas porosity. Match the code list to your process. Aluminium die casters add flash and soldering, while steel foundries add hot tears and arc-gouging damage.
Move the first look earlier in the route
Logging at the point of finding helps only if that point comes sooner. Add a visual check at shakeout, where surface sand and misruns are plain. Add another on the first piece after fettling.
For critical parts, record dye penetrant or radiography results against the same heat and pattern. A hidden shrinkage found by X-ray then joins the same trend as the visible ones.
Let the data set the sampling. If one pattern has a history of porosity, inspect every piece for a while. Relax the plan when its trend falls. Sampling that follows evidence costs less than blanket inspection and catches more.
- Visual check at shakeout
- First-off check after fettling
- Dye penetrant or radiography on critical parts
- Pressure or leak test before machining
- Dispatch check against the drawing
Review one trend a week and change one thing
A log nobody reads is only a diary. Hold a short weekly review with the production manager, the melter, the moulding lead and quality. Show the top three causes by pattern for the last four weeks.
Pick one cause and one change. It might be a pouring temperature, a larger riser or a closer look at a sand additive. Record the change with its date and watch the next heats. If the cause code drops, keep the change. If not, undo it and try the next suspect. One variable at a time is slow but honest.
Start this week. Print the code list, hang it at fettling and shakeout, and note every reject by code and heat number on one sheet for two weeks.
Casting defect log sheet
A single-page log with one row per rejected piece. Columns hold date, station, casting tag, heat number, pattern or die number, shift, cause code, quantity and weight. A code key runs down the right edge with a one-line description of each defect. A tally box at the foot counts causes by pattern for the week.
Open a blank worksheet to printQuestions owners ask
Which casting defects should be coded first?
Start with the ones that cost most: shrinkage, porosity, sand inclusion, cold shut and misrun. Add more codes only when a defect turns up often enough that a general code hides it.
Who should log the defect?
Whoever finds it, at the bench. A supervisor retyping slips at day end loses the heat number and the exact spot on the casting, which are the details that matter. Train the fettlers and machinists to use the codes in one short session.
Is a spreadsheet enough for this?
For one line and a handful of patterns, yes. When several stations log entries and cutting by heat and pattern takes hours each week, a shared system saves the effort. Look for one that keeps heat number, pattern number and cause code as fields you can filter, not free text.
How do we trace a defect to a heat if castings are not marked?
Cast a heat or batch mark onto the piece, or keep castings in tagged bins from shakeout to fettling. Without a mark or a bin tag the link to the heat breaks.