Quality Control for Conveyor manufacturers
Record specified inspections and the disposition of checked goods.
Does this function belong in your operation?
Use when goods or production stages require documented checks before release.
Material or output reaches an agreed inspection stage.
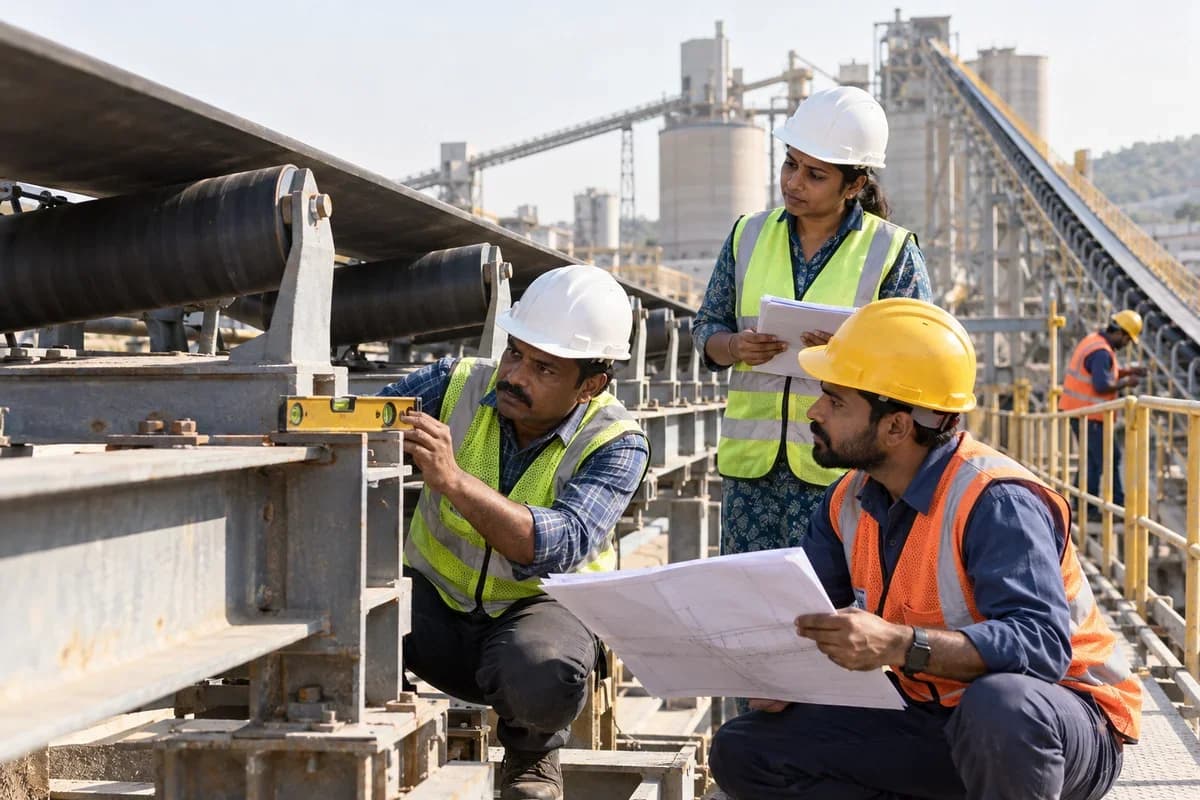
Checks cover incoming steel, weld inspection on frames and roller spin before despatch. Failures are logged against the section number. Trial fit results are kept on the same record.
Bring the records the workflow depends on.
- Inspection specifications
- Sampling and acceptance rules
- Authorised reviewers
Outputs to check
- Inspection readings and evidence
- Hold, release or rejection record
- Nonconformance follow-up list
Follow the quality control workflow.
Use this sequence to compare your current process with the proposed module. Agree the owner, permission and exception at each step.
Who uses the module, and who approves?
Keep responsibilities distinct even when one person holds more than one role.
Decide how exceptions are handled.
These business rules belong in configuration and testing. A normal transaction alone does not demonstrate that the workflow is ready.
Can this work independently?
Quality records can be maintained independently against identifiable receipts or jobs. Inventory and production connections must enforce any hold or release decision. The module records authorised checks; it does not select a regulatory standard or replace a qualified inspector's judgement.
Systems and records it connects with
- Work orders: Released production jobs, material issues and output records.
- Goods receipt: Counted, accepted and rejected supplier-delivery quantities.
- Purchase returns: Approved supplier-return quantities and adjustment references.
- Batch and serial tracking: Lot or unit identifiers carried through stock movements.
Configure, test and introduce the workflow.
- Show us where checks happen now. A note names the checkpoints and the parameters to record.
- Provide limits and your list of rejection reasons. A test lot can then be checked on the trial screen. Checkers use it at a station for a trial run. Their remarks return as changes.
- Checkers, production and purchase each practise their part. Each group gets a printed card. Other stations join as the trial station settles. The team reviews rejection reasons together.
Check the result before rollout.
Apply these checks to a sample from the agreed workflow, then repeat with an exception. Keep the expected result beside the test record.
- Failed items follow the agreed hold rule.
- Results retain the specification version.
- Release decisions identify the reviewer.
How the business operates.
A conveyor is rarely one machine. It is a run of frames, rollers, belts, drives and guards that must meet on a customer’s floor at the right height. Errors show up only when the last section is bolted. By then it is expensive.
The records that hold the operation together.
- Enquiries and duty capture. Log each enquiry with product, belt speed, incline and route, and keep the photographs and sketches sent by the buyer beside the duty details so nothing is asked twice.
- Site survey records. Enter dimensions, column positions, floor openings and elevation marks from the visit, and attach them to the project and quotation so the drawing office redraws nothing from paper. Numbers travel.
- Layout quotations. Price runs from your tables for belt width, roller diameter, drive and guards, and keep every revision shown to the buyer so the final price can be traced back.
- Section drawings and numbering. Release numbered section drawings and parts lists under a revision letter, so the workshop and the crew work from the same list. Old sheets are retired.
Operational bottlenecks to check
The site survey is separate from the quote
Dimensions are taken on a pad and typed later. A frame is cut to a length that was misread. It is scrapped.
Sections are not numbered against the layout
Frames leave the workshop without a clear order. On site the crew spends a morning sorting what goes where.
How work flows across this business
This module sits within a wider operating process. Use the sequence to identify the other teams and records affected by a change.
1. Enquiry and survey
The enquiry records product, duty and route. A survey visit is booked and its dimensions are entered as measured.
2. Layout and quotation
A layout is drawn and priced, with troughed or flat belt, roller type, geared motor, guards and pull-cord switches, and every revision is kept for the buyer. Nothing is overwritten.
3. Order and section release
A confirmed order opens a project, and numbered section drawings and parts lists are released to the workshop under a revision letter. The crew reads the same list.
4. Fabrication and trial fit
Frames are cut, welded and painted, then trial fitted in the yard. Remarks are logged before dispatch.
5. Loading and erection
Sections are loaded in reverse erection order, and the crew fits them from the head end while noting every change made on site. Nothing is lost.
6. Handover and spares
The conveyor is run and signed off, and the as-built layout is saved so that belt, idler and drive orders can be quoted from it years later. History stays.
Industry reports to connect with
- Projects in build by stage
- Sections fabricated, fitted and loaded, by project
- Belt, roller and idler issues against each run
- Quotations won, lost and open, by conveyor type
Questions before implementation.
When should conveyor manufacturers consider quality control?
Use when goods or production stages require documented checks before release. Material or output reaches an agreed inspection stage.
What should we bring to the requirements discussion?
Bring anonymised examples of Inspection specifications; Sampling and acceptance rules; Authorised reviewers. Show who creates, checks and changes each record. Use only records from an activity that meets the suitability conditions above.
Does this replace our existing business software?
The starting point is your current system and the gap you need to close. Record specified inspections and the disposition of checked goods. Configuration, a connected module or a custom build are evaluated against that gap before a replacement is proposed.
What is outside this module?
The software records your inspection process and does not certify product safety or regulatory conformity.
How are scope, price and rollout decided?
The proposal follows a review of your records, user roles, branches and existing software. Data migration, connections, training and support are scoped separately where needed. Failed items follow the agreed hold rule. Use this check when reviewing the first working version.
Related functions for conveyor manufacturers.
Discuss quality control for your business.
Tell us which workflow needs attention and which systems your team uses. The next step is a requirements discussion and a written scope.
What happens after you share your requirements
- We review your brief and the systems you already use.
- We clarify the workflow, missing information and the work to consider first.
- The proposed scope sets out the deliverables, responsibilities and dependencies.
- Review the scope and commercial terms before deciding whether to proceed.
Start with your requirements
Describe your current process, the people involved and the change you need. Start with the details you know; we can clarify the rest together.
Share your requirements