Quality Control for Plastic packaging manufacturers
Record specified inspections and the disposition of checked goods.
Does this function belong in your operation?
Use when goods or production stages require documented checks before release.
Material or output reaches an agreed inspection stage.
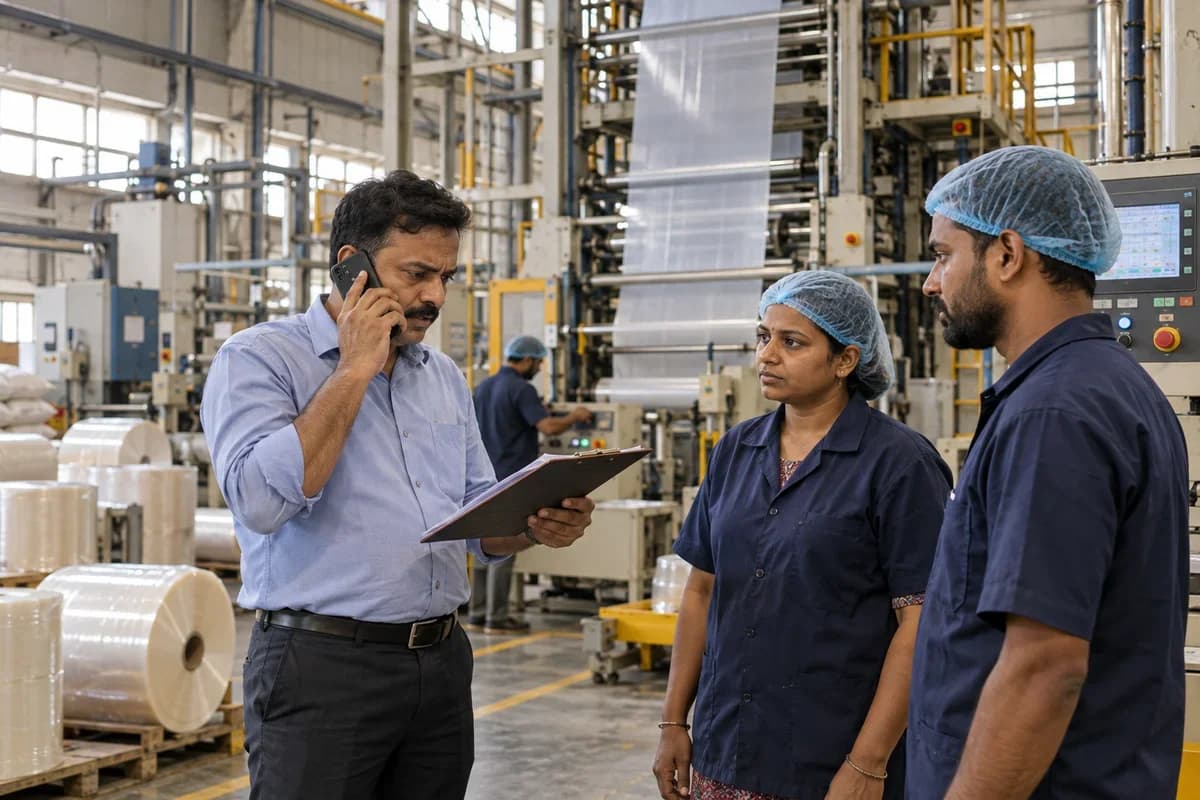
Print registration, bond strength, seal strength and treatment level are recorded per reel. A laminate failing peel strength is held. Inspectors link results to the adhesive batch used.
Bring the records the workflow depends on.
- Inspection specifications
- Sampling and acceptance rules
- Authorised reviewers
Outputs to check
- Inspection readings and evidence
- Hold, release or rejection record
- Nonconformance follow-up list
Follow the quality control workflow.
Use this sequence to compare your current process with the proposed module. Agree the owner, permission and exception at each step.
Who uses the module, and who approves?
Keep responsibilities distinct even when one person holds more than one role.
Decide how exceptions are handled.
These business rules belong in configuration and testing. A normal transaction alone does not demonstrate that the workflow is ready.
Can this work independently?
Quality records can be maintained independently against identifiable receipts or jobs. Inventory and production connections must enforce any hold or release decision. The module records authorised checks; it does not select a regulatory standard or replace a qualified inspector's judgement.
Systems and records it connects with
- Work orders: Released production jobs, material issues and output records.
- Goods receipt: Counted, accepted and rejected supplier-delivery quantities.
- Purchase returns: Approved supplier-return quantities and adjustment references.
- Batch and serial tracking: Lot or unit identifiers carried through stock movements.
Configure, test and introduce the workflow.
- Show us where checks happen now. A note names the checkpoints and the parameters to record.
- Provide limits and your list of rejection reasons. A test lot can then be checked on the trial screen. Checkers use it at a station for a trial run. Their remarks return as changes.
- Checkers, production and purchase each practise their part. Each group gets a printed card. Other stations join as the trial station settles. The team reviews rejection reasons together.
Check the result before rollout.
Apply these checks to a sample from the agreed workflow, then repeat with an exception. Keep the expected result beside the test record.
- Failed items follow the agreed hold rule.
- Results retain the specification version.
- Release decisions identify the reviewer.
How the business operates.
A stand-up pouch is built in layers. Film is blown, reverse printed, laminated to a cast polypropylene sealant web and slit to width before a bag machine sees it. Every step leaves a narrower reel.
The records that hold the operation together.
- Pouch quotations. Convert a pouch size and quantity into film metres, kilograms, ink and adhesive, then price with the expected scrap of each stage.
- Film structure and recipe. Keep every layer’s polymer, micron and web width beside the adhesive, ink and sealant it takes, so a repeat order begins from an identical build.
- Artwork approvals. Log artwork revisions, proof approvals and the customer’s signed Pantone match, and stop a run if the approved revision differs from the cylinder.
- Cylinder and plate register. Hold each gravure cylinder or flexo plate with owner, rack position, impressions run and the artwork revision it was made from.
Operational bottlenecks to check
Waste is lost between stages
Each machine reports its own scrap. Nobody adds extruder trim, press start-up film, laminator mismatch and slitter edge together, so the plant never learns the kilograms of resin bought to deliver one finished pouch order.
Reels lose their identity
A printed reel is slit into narrower child reels that go to different laminators and bag machines, and nobody writes down which went where. Numbers sit on masking tape. It peels.
How work flows across this business
This module sits within a wider operating process. Use the sequence to identify the other teams and records affected by a change.
1. Specification and quote
The brand owner’s pouch size, gusset, zipper and film structure are recorded together with the colour count. The quotation converts pouches into film metres and kilograms.
2. Artwork and cylinders
Artwork revisions are logged and the proof is approved. Cylinders or flexo plates are then made and entered with their owner and rack location.
3. Extrusion and print
Base film reels are numbered and weighed. Corona treatment is checked, and print runs record the Pantone match approval and the waste at start-up.
4. Lamination and slitting
Printed reels are laminated to the sealant film with solventless or solvent adhesive and slit to width. Each child reel is numbered under its mother reel.
5. Conversion
Pouch and bag machines make the finished goods. Counts, bottom seal checks and rejects are logged by reel.
6. Packing and delivery
Pouches are counted into cartons and pallets. Labels and delivery notes carry the film lot.
Industry reports to connect with
- Total scrap per order, split by stage
- Reel genealogy from film lot to carton
- Artwork proofs awaiting approval
- Cylinders by owner, rack position and impressions
Questions before implementation.
When should plastic packaging manufacturers consider quality control?
Use when goods or production stages require documented checks before release. Material or output reaches an agreed inspection stage.
What should we bring to the requirements discussion?
Bring anonymised examples of Inspection specifications; Sampling and acceptance rules; Authorised reviewers. Show who creates, checks and changes each record. Use only records from an activity that meets the suitability conditions above.
Does this replace our existing business software?
The starting point is your current system and the gap you need to close. Record specified inspections and the disposition of checked goods. Configuration, a connected module or a custom build are evaluated against that gap before a replacement is proposed.
What is outside this module?
The software records your inspection process and does not certify product safety or regulatory conformity.
How are scope, price and rollout decided?
The proposal follows a review of your records, user roles, branches and existing software. Data migration, connections, training and support are scoped separately where needed. Failed items follow the agreed hold rule. Use this check when reviewing the first working version.
Related functions for plastic packaging manufacturers.
Discuss quality control for your business.
Tell us which workflow needs attention and which systems your team uses. The next step is a requirements discussion and a written scope.
What happens after you share your requirements
- We review your brief and the systems you already use.
- We clarify the workflow, missing information and the work to consider first.
- The proposed scope sets out the deliverables, responsibilities and dependencies.
- Review the scope and commercial terms before deciding whether to proceed.
Start with your requirements
Describe your current process, the people involved and the change you need. Start with the details you know; we can clarify the rest together.
Share your requirements