Business solutions for Switchgear manufacturers
Explore software for work such as “LT panels and motor control centres”. Review each business function below, including when it fits and what to check before implementation.
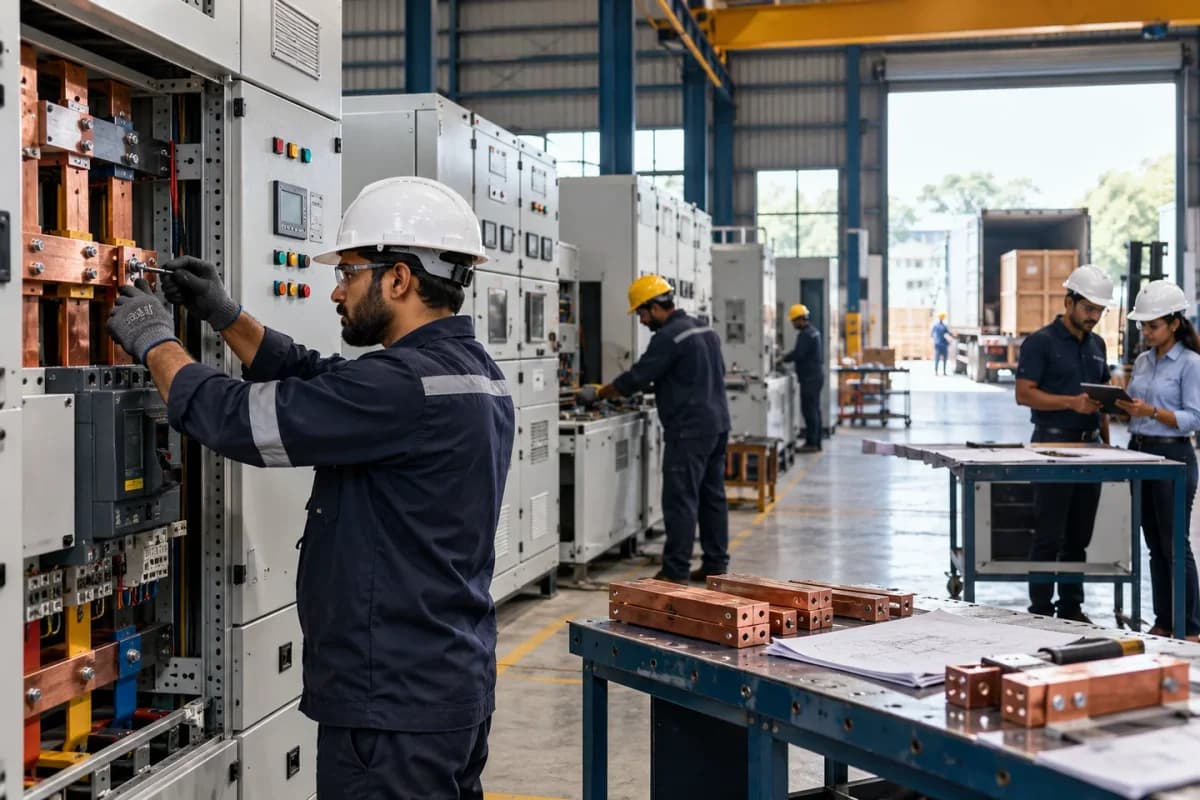
How the business operates.
A switchboard maker takes sheet steel, copper bar and bought-in breakers, and hands over a lineup of panels that a client’s consultant has already approved on paper. The drawing revision decides what gets built. That is the rule. One late change to a feeder can alter the breaker, the busbar rating and the nameplate.
The records that hold the operation together.
- Tender and panel templates. Price a lineup from stored incomer, coupler and feeder templates, then adjust ratings and accessories. Every tender revision is kept.
- Feeder schedule. List each feeder with its rating, breaker type, metering and protection, so the schedule matches the single-line diagram.
- Drawing revision control. Hold general arrangement drawings, consultant comments and the approved revision. Only the released revision reaches the floor.
- Panel bill of materials. Break each panel into enclosure, busbar, breaker, relay and wiring items, with the quantity reserved for that feeder.
- Bought-in components. Track purchase orders for breakers, relays and instrument transformers, with promised dates and the panel each is held for.
- Busbar and fabrication stages. Record cutting, punching, bending and plating per panel, including pieces out for outside processes and their return.
- Wiring and assembly board. See which panels are in the wiring bay, which await components and which are ready for the test bay.
- Routine test records. Enter insulation, wiring and functional test results per panel serial number, with witness inspector details.
Operational bottlenecks to check
Drawing revisions drift from the floor
The consultant approves revision C, but the fabrication team still holds revision B on a printout. A feeder is built with the wrong breaker frame, and the fault shows at the witness test.
Bought-in breakers set the schedule
Breakers, relays and current transformers come from several makers on different lead times. A lineup waits for one missing relay while the finished frames take up bay space.
Busbar work is hard to trace
Copper bar is cut and bent against a drawing, then sent out for plating. Nobody can say which bar length belongs to which panel once it returns in a crate.
Test reports sit in loose files
Insulation readings and functional checks get pencilled onto paper beside the test set. Finding one panel’s report months later means a shelf search. It is slow.
Variations pile up after approval
A client asks for an extra feeder or a changed meter. The cost change travels by phone, and the invoice does not match the order.
Follow the work across teams.
This is a planning flow. Confirm the steps, owners and approval rules against your actual operation.
Roles and responsibility boundaries.
Reports your managers need.
- Lineups by stage, with panels held for missing components
- Drawing revisions awaiting consultant approval
- Bought-in items on order against the panel they are reserved for
- Busbar pieces out for plating and their expected return
- Routine test results by panel serial number
- Variations raised against each order
- Dispatches and invoices by client
Connections to scope
- Accounting export
- Drawing file storage
- Label printer
Confirm data access, record ownership and the exchange method for each connection. Inclusion here does not mean every connection is available in a standard package.
Setup decisions and adoption risks.
Use these requirements to plan phases, data migration and user training. Agree the release sequence after reviewing your current systems.
Limitations to settle before implementation
- An electrician who wires a few boards on site can work from drawings and a notebook.
- Makers of cables or lighting fittings will find Cable and Wire Manufacturer Management Software or Industrial Lighting Manufacturer Management Software closer.
Modules to consider first.
These functions connect to the operating model above. Confirm each one against the work your business actually runs.
Choose the operation you want to improve.
Use these activities to explain your scope. Your business does not need every function in the directory.
- LT panels and motor control centres
- HT switchgear and ring main units
- Air and moulded case circuit breakers
- Distribution boards for buildings
- Busbar trunking
- Switchgear for solar and wind plants
- Retrofit and refurbishment
- Spares and breaker servicing
- Utility and PSU rate contracts
Explore the business functions.
Production, stock, fleet and recurring billing functions apply only where your business runs those activities. Read the suitability conditions on each page.
Manufacturing
Batch and Serial Tracking
Trace goods using batch identifiers or individual serial numbers.
View workflow and suitability →Bill of Materials
Define the materials and quantities needed for a manufactured item.
View workflow and suitability →Job Work Management
Track material sent to an outside processor and returned after work.
View workflow and suitability →Quality Control
Record specified inspections and the disposition of checked goods.
View workflow and suitability →Work Order Management
Track a production job from material issue to completed output.
View workflow and suitability →
Human Resources
Inventory Management
CRM
Start with the problem your team can describe.
Bring a sample record and show where information is copied, missed or waiting for approval. Scope the first useful change from there.
What happens after you share your requirements
- We review your brief and the systems you already use.
- We clarify the workflow, missing information and the work to consider first.
- The proposed scope sets out the deliverables, responsibilities and dependencies.
- Review the scope and commercial terms before deciding whether to proceed.
Start with your requirements
Describe your current process, the people involved and the change you need. Start with the details you know; we can clarify the rest together.
Share your requirements