Business solutions for Auto parts manufacturers
Explore software for work such as “Engine and drivetrain components”. Review each business function below, including when it fits and what to check before implementation.
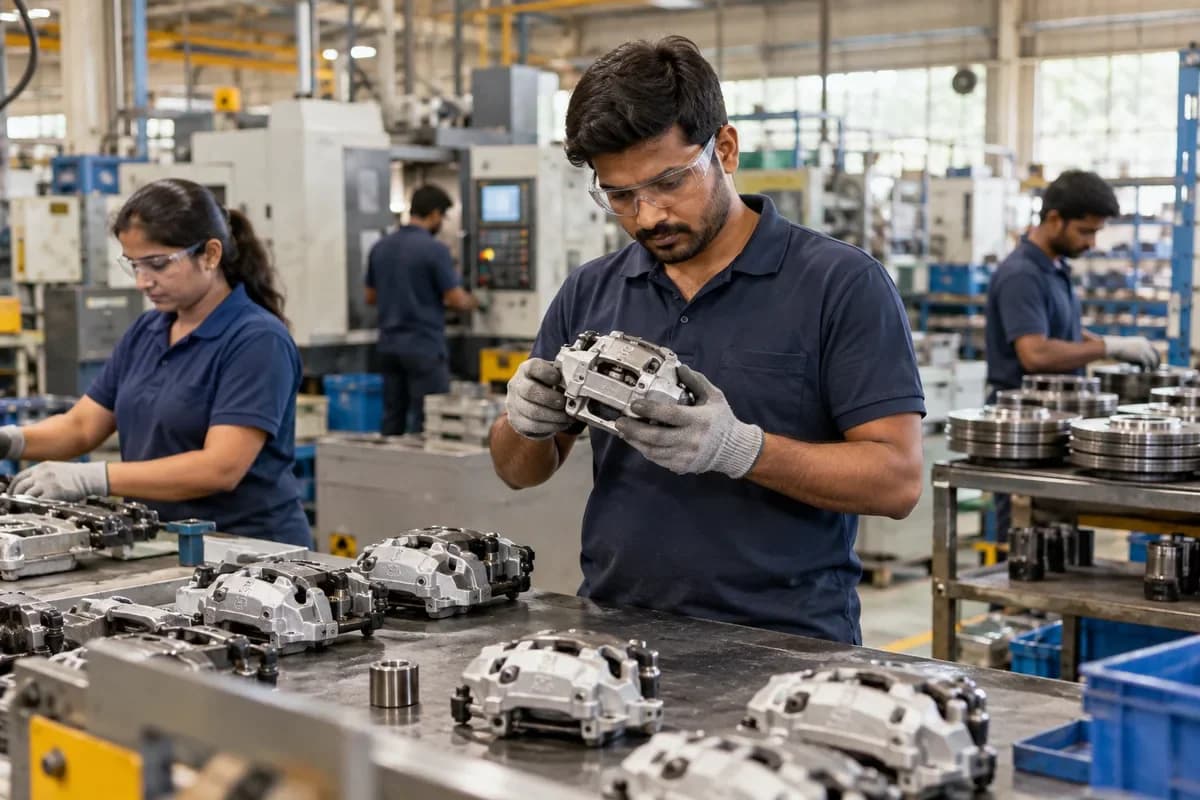
How the business operates.
An auto parts plant makes components to a customer’s drawing, such as a stamped bracket, a rubber bush, a cast housing or a moulded clip. The buyer is a vehicle maker. Each part number carries a drawing revision, a control plan, a failure-mode analysis (FMEA) and, where the buyer asks, a first-sample approval file (PPAP) before volume begins. Releases change without notice.
The records that hold the operation together.
- Customer part master. Hold each part number with revision, material grade, die list, control plan and label format, so a setup never starts from a loose spreadsheet.
- Revision control. Release a new drawing revision to the operator terminal and the gauge list together, and the earlier print is blocked at the machine.
- Approval package files. Attach ballooned drawings, dimensional reports, material certificates and Cpk studies to the part and revision, so a first-article submission is assembled in one place.
- Customer release planning. Load the forecast and daily call-offs from each customer plant, then compare them with the previous schedule before the planner sequences the week.
- Material and tooling plan. Check coil, bar, resin, inserts and die availability against planned runs before a press or machining centre is booked.
- Lot records. Capture press or machine number, die, shift, heat or resin lot and operator for each production lot, then print the lot number on the box label.
- In-process and final inspection. Log gauge and CMM readings by lot against the control plan, with a hold on failed lots and a recorded reason for any release from hold.
- Outside process orders. Follow brackets and shafts out to the plater, heat treater or powder coater, then match the counts on return and flag short or rejected pieces.
Operational bottlenecks to check
Customer releases change the plan daily
Weekly and daily schedules arrive from several vehicle plants, each in its own file layout, and the planner retypes them into a sheet. A late amendment is missed until a truck is short. The line stops at the customer.
Drawing revisions reach the shop floor late
A customer revises a drawing and the quality department updates the gauge, but the press operator still works from the earlier sheet at the machine. The lot is made to the old print. It is rejected on arrival at the dock.
First-sample approval files are scattered
Dimensional layouts, material certificates, the control plan and capability data for a new part sit in different folders, and volume production waits while somebody gathers the pieces. Sign-off drifts week by week.
Lot traceability stops at the pallet
A returnable box carries a label, yet the shift, press, die and coil lot behind it sit in a notebook. A defect found at the customer cannot be contained to a few boxes, so the pallet is sorted by hand.
Returnable boxes and labels go astray
Customer-owned boxes, dunnage and barcode label formats are tracked by memory, so boxes pile up at the customer and a label format is wrong. A truck is refused at the dock. Cost lands on the supplier.
Follow the work across teams.
This is a planning flow. Confirm the steps, owners and approval rules against your actual operation.
Roles and responsibility boundaries.
Reports your managers need.
- Release changes by customer plant and part
- Lots by inspection result and die
- Parts shipped against each release
- Plating and heat treatment returns, short and rejected
- Crates and racks held by customer plant
- Complaints by part and root cause
Connections to scope
- Customer release files
- Label printer
- Barcode scanner
- Accounting export
Confirm data access, record ownership and the exchange method for each connection. Inclusion here does not mean every connection is available in a standard package.
Setup decisions and adoption risks.
Use these requirements to plan phases, data migration and user training. Agree the release sequence after reviewing your current systems.
Limitations to settle before implementation
- A small workshop making one-off repairs for local garages, with no scheduled call-offs to plan against, does not need release planning.
- Aftermarket retailers need stock and billing.
Modules to consider first.
These functions connect to the operating model above. Confirm each one against the work your business actually runs.
Choose the operation you want to improve.
Use these activities to explain your scope. Your business does not need every function in the directory.
- Engine and drivetrain components
- Braking system parts
- Suspension and steering parts
- Electrical and wiring components
- Body and sheet metal parts
- Filters and consumables
- Bearings and fasteners
- Two-wheeler specific parts
- Export-grade OEM components
Explore the business functions.
Production, stock, fleet and recurring billing functions apply only where your business runs those activities. Read the suitability conditions on each page.
Retail and POS
Manufacturing
Batch and Serial Tracking
Trace goods using batch identifiers or individual serial numbers.
View workflow and suitability →Job Work Management
Track material sent to an outside processor and returned after work.
View workflow and suitability →Production Planning
Plan manufacturing quantities against demand, materials and capacity.
View workflow and suitability →Quality Control
Record specified inspections and the disposition of checked goods.
View workflow and suitability →
Human Resources
Inventory Management
Platform
Start with the problem your team can describe.
Bring a sample record and show where information is copied, missed or waiting for approval. Scope the first useful change from there.
What happens after you share your requirements
- We review your brief and the systems you already use.
- We clarify the workflow, missing information and the work to consider first.
- The proposed scope sets out the deliverables, responsibilities and dependencies.
- Review the scope and commercial terms before deciding whether to proceed.
Start with your requirements
Describe your current process, the people involved and the change you need. Start with the details you know; we can clarify the rest together.
Share your requirements