Quality Control for Auto parts manufacturers
Record specified inspections and the disposition of checked goods.
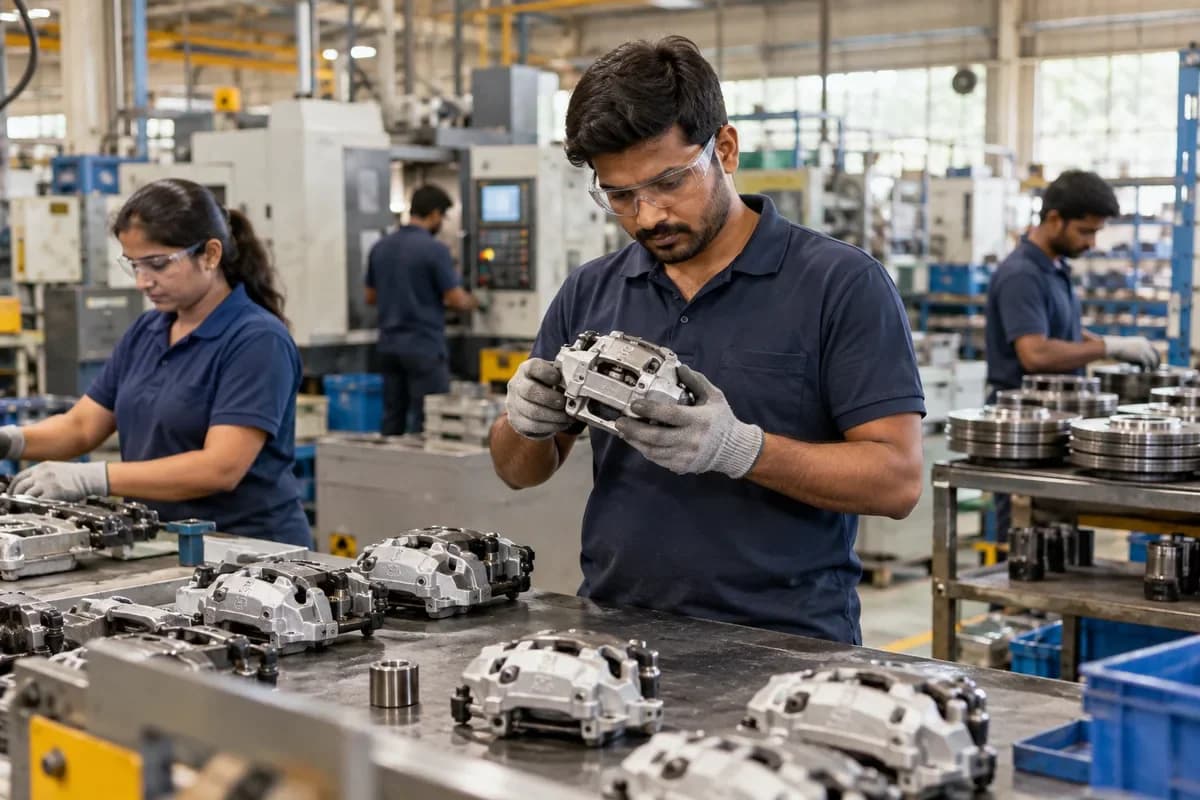
Does this function belong in your operation?
Use when goods or production stages require documented checks before release.
Material or output reaches an agreed inspection stage.
Inspection plans list dimensions, gauges and sample sizes for each part and each process step. Rejections are counted by cause. Hold tags stay on suspect bins until a supervisor releases them.
Bring the records the workflow depends on.
- Inspection specifications
- Sampling and acceptance rules
- Authorised reviewers
Outputs to check
- Inspection readings and evidence
- Hold, release or rejection record
- Nonconformance follow-up list
Follow the quality control workflow.
Use this sequence to compare your current process with the proposed module. Agree the owner, permission and exception at each step.
Who uses the module, and who approves?
Keep responsibilities distinct even when one person holds more than one role.
Decide how exceptions are handled.
These business rules belong in configuration and testing. A normal transaction alone does not demonstrate that the workflow is ready.
Can this work independently?
Quality records can be maintained independently against identifiable receipts or jobs. Inventory and production connections must enforce any hold or release decision. The module records authorised checks; it does not select a regulatory standard or replace a qualified inspector's judgement.
Systems and records it connects with
- Work orders: Released production jobs, material issues and output records.
- Goods receipt: Counted, accepted and rejected supplier-delivery quantities.
- Purchase returns: Approved supplier-return quantities and adjustment references.
- Batch and serial tracking: Lot or unit identifiers carried through stock movements.
Configure, test and introduce the workflow.
- Show us where checks happen now. A note names the checkpoints and the parameters to record.
- Provide limits and your list of rejection reasons. A test lot can then be checked on the trial screen. Checkers use it at a station for a trial run. Their remarks return as changes.
- Checkers, production and purchase each practise their part. Each group gets a printed card. Other stations join as the trial station settles. The team reviews rejection reasons together.
Check the result before rollout.
Apply these checks to a sample from the agreed workflow, then repeat with an exception. Keep the expected result beside the test record.
- Failed items follow the agreed hold rule.
- Results retain the specification version.
- Release decisions identify the reviewer.
How the business operates.
An auto parts plant makes components to a customer’s drawing, such as a stamped bracket, a rubber bush, a cast housing or a moulded clip. The buyer is a vehicle maker. Each part number carries a drawing revision, a control plan, a failure-mode analysis (FMEA) and, where the buyer asks, a first-sample approval file (PPAP) before volume begins. Releases change without notice.
The records that hold the operation together.
- Customer part master. Hold each part number with revision, material grade, die list, control plan and label format, so a setup never starts from a loose spreadsheet.
- Revision control. Release a new drawing revision to the operator terminal and the gauge list together, and the earlier print is blocked at the machine.
- Approval package files. Attach ballooned drawings, dimensional reports, material certificates and Cpk studies to the part and revision, so a first-article submission is assembled in one place.
- Customer release planning. Load the forecast and daily call-offs from each customer plant, then compare them with the previous schedule before the planner sequences the week.
Operational bottlenecks to check
Customer releases change the plan daily
Weekly and daily schedules arrive from several vehicle plants, each in its own file layout, and the planner retypes them into a sheet. A late amendment is missed until a truck is short. The line stops at the customer.
Drawing revisions reach the shop floor late
A customer revises a drawing and the quality department updates the gauge, but the press operator still works from the earlier sheet at the machine. The lot is made to the old print. It is rejected on arrival at the dock.
How work flows across this business
This module sits within a wider operating process. Use the sequence to identify the other teams and records affected by a change.
1. Part set-up
A customer part number is entered with drawing revision, material grade, die list, control plan and label format, and the PPAP documents attach to that same revision.
2. Release received
Load the schedule from the plant and the system compares it with the previous release, highlighting each part whose quantity or ship date moved. The planner then re-sequences the press line.
3. Plan and material
Machines, dies and material are planned against the release, so a shortfall in coil, bar stock, resin pellet or threaded inserts shows before the run is booked. No press starts short.
4. Production lots
Operators scan the press number, die or mould, shift and heat or resin lot at start-up, and first-off and patrol checks are logged against the lot as it runs.
5. Final check and dispatch
Final inspection against the control plan puts a failed lot on hold, then labels print in the VDA or AIAG layout the customer asks for and ship notice leaves. A held lot cannot ship.
6. Complaints and returns
A complaint opens against the lot. Containment, root cause and corrective action are written into an 8D reply, and returnable boxes are reconciled with the customer plant afterwards.
Industry reports to connect with
- Release changes by customer plant and part
- Lots by inspection result and die
- Parts shipped against each release
- Plating and heat treatment returns, short and rejected
Questions before implementation.
When should auto parts manufacturers consider quality control?
Use when goods or production stages require documented checks before release. Material or output reaches an agreed inspection stage.
What should we bring to the requirements discussion?
Bring anonymised examples of Inspection specifications; Sampling and acceptance rules; Authorised reviewers. Show who creates, checks and changes each record. Use only records from an activity that meets the suitability conditions above.
Does this replace our existing business software?
The starting point is your current system and the gap you need to close. Record specified inspections and the disposition of checked goods. Configuration, a connected module or a custom build are evaluated against that gap before a replacement is proposed.
What is outside this module?
The software records your inspection process and does not certify product safety or regulatory conformity.
How are scope, price and rollout decided?
The proposal follows a review of your records, user roles, branches and existing software. Data migration, connections, training and support are scoped separately where needed. Failed items follow the agreed hold rule. Use this check when reviewing the first working version.
Related functions for auto parts manufacturers.
Discuss quality control for your business.
Tell us which workflow needs attention and which systems your team uses. The next step is a requirements discussion and a written scope.
What happens after you share your requirements
- We review your brief and the systems you already use.
- We clarify the workflow, missing information and the work to consider first.
- The proposed scope sets out the deliverables, responsibilities and dependencies.
- Review the scope and commercial terms before deciding whether to proceed.
Start with your requirements
Describe your current process, the people involved and the change you need. Start with the details you know; we can clarify the rest together.
Share your requirements