Business solutions for Blow moulding companies
Explore software for work such as “Stock bottle sales to small and new brands”. Review each business function below, including when it fits and what to check before implementation.
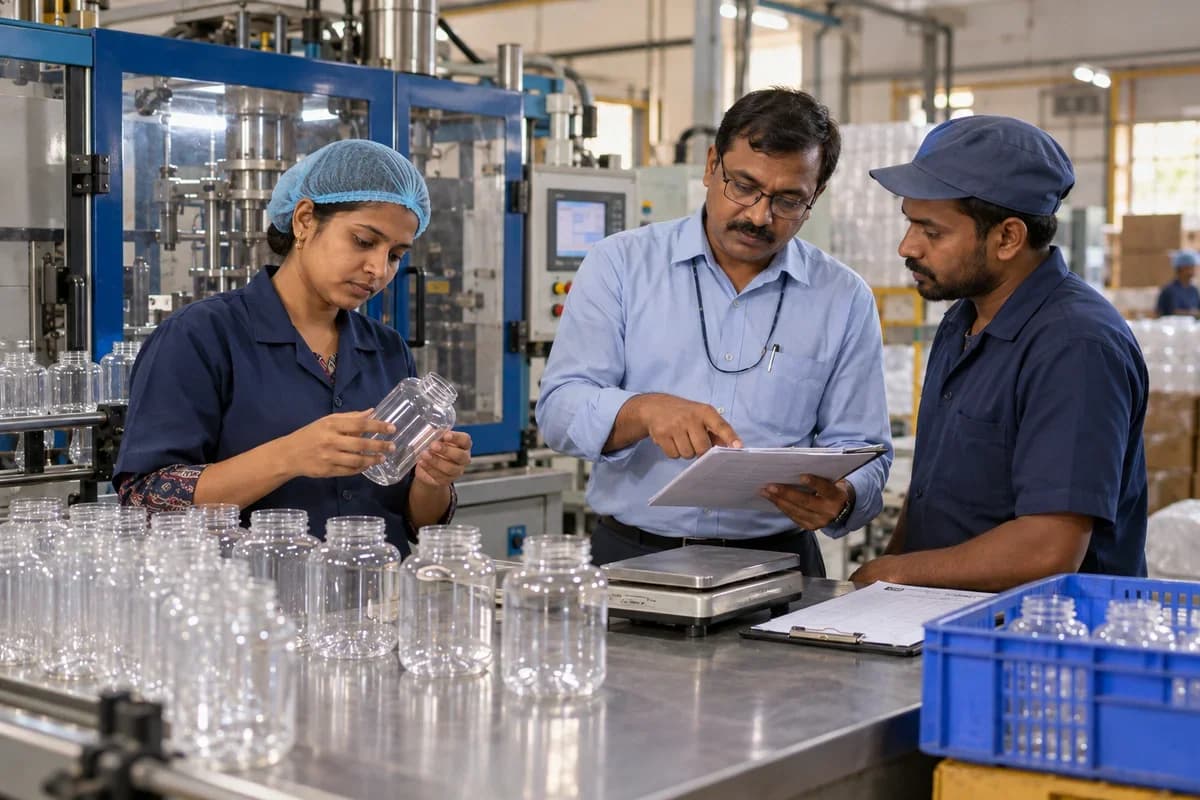
How the business operates.
Hollow containers hide faults. Thin walls are the usual culprit. A bottle with a thin shoulder looks fine on the line and then splits in a filler’s warehouse, weeks after the shift that made it ended. The record that explains it, such as parison programme, resin lot or cooling time, is rarely near the pallet.
The records that hold the operation together.
- Container quotations. Price a bottle, jerry can or drum from shot weight, cavities, cycle rate, and resin and masterbatch cost, then keep every revision beside the accepted price. Lost quotes stay searchable.
- Container design register. Store volume, neck finish, target weight, allowed wall range, handle style, mould number and test requirements for each design, together with the customer’s drawing revision. Old revisions remain readable.
- Machine set-up sheets. Keep parison programme, blow pressure, cooling time and cycle target for every mould and machine pairing, so a setter sees which settings a run really used. Good days become repeatable.
- Resin, preform and masterbatch stock. Receive HDPE and PET granule lots, bought-in preforms and colour masterbatch, then draw them down against runs, with a low-colour warning raised before the hopper is loaded. Shortfalls show before start-up.
- Regrind control. Weigh pinch-off flash into the granulator, book it as regrind stock, and set the allowed ratio per container so each run notes what was blended back. Virgin and regrind stay separate.
- Weight and wall checks. Log bottle weight and wall thickness at set points through the shift, by cavity, with limits drawn from the customer’s specification and shown against each reading. Weight drift shows early.
- Leak, drop and top-load tests. Enter leak, drop and top-load results with the sample’s cavity and run, so a failure holds the lot and lists blow pressure, cooling time and resin lot behind it. Causes surface in one view.
- Mould and cavity record. List each mould with its cavities, cleaning dates and repairs such as vent clearing, pinch-off blade regrinding or neck insert replacement, and flag the next planned service. Tired tools get pulled.
Operational bottlenecks to check
Weight and wall thickness drift unseen
Weight is checked on paper at the machine, once an hour at best. The sheet goes into a folder nobody opens until a customer complains about a thin shoulder. No record shows how bottle weight moved over the shift.
Flash regrind is blended blindly
Pinch-off trim goes into the grinder and then into the next hopper, and no run carries its blend ratio. A later complaint has nothing to hold on to.
Preform and resin stocks are separate
PET preforms, HDPE granules and colour masterbatch are counted in different books. A missing blue masterbatch turns up late, after the mould is fitted, the heaters are hot, the setter is idle and the filler’s truck is booked.
Test failures lose their context
A drop or leak test fails, and the result sits on a bench sheet with no link to the cavity, the parison programme or the resin lot. Nobody can say why. The next shift repeats it.
Pallet counts disagree at the gate
Cartons per layer and layers per pallet are agreed by phone. The pallet at the dock rarely matches the paperwork, so the filler recounts bottles as the truck unloads.
Follow the work across teams.
This is a planning flow. Confirm the steps, owners and approval rules against your actual operation.
Roles and responsibility boundaries.
Reports your managers need.
- Bottle weight trend by cavity and shift
- Rejects by defect such as thin shoulder, pinhole or flash, by mould and resin lot
- Regrind used against virgin resin by container
- Leak and drop test results by customer and cavity
- Resin, preform and masterbatch stock against open runs
- Machine output against mould cycle target
- Pallets dispatched by filler with run references
Connections to scope
- Tablet entry at the machine
- Barcode label printer
- Accounting export
Confirm data access, record ownership and the exchange method for each connection. Inclusion here does not mean every connection is available in a standard package.
Setup decisions and adoption risks.
Use these requirements to plan phases, data migration and user training. Agree the release sequence after reviewing your current systems.
Limitations to settle before implementation
- A small shop that blows a single jerry can for one customer on one machine can manage with a weight sheet, a mould list and a pallet list.
- Companies whose main product is moulded solid parts or extruded profiles will find Injection Moulding Company Management Software or Plastic Extrusion Company Management Software closer.
Modules to consider first.
These functions connect to the operating model above. Confirm each one against the work your business actually runs.
Choose the operation you want to improve.
Use these activities to explain your scope. Your business does not need every function in the directory.
- Stock bottle sales to small and new brands
- Custom mould projects for mid-sized packers
- Lubricant and edible oil pack supply
- Agrochemical bottle supply before the sowing season
- Pharma and nutraceutical container supply
- Contract moulding for brands that own their moulds
- Export packaging enquiries
Explore the business functions.
Production, stock, fleet and recurring billing functions apply only where your business runs those activities. Read the suitability conditions on each page.
Assets and Fleet
Retail and POS
Manufacturing
Batch and Serial Tracking
Trace goods using batch identifiers or individual serial numbers.
View workflow and suitability →Production Planning
Plan manufacturing quantities against demand, materials and capacity.
View workflow and suitability →Quality Control
Record specified inspections and the disposition of checked goods.
View workflow and suitability →
Finance & Accounting
Inventory Management
Start with the problem your team can describe.
Bring a sample record and show where information is copied, missed or waiting for approval. Scope the first useful change from there.
What happens after you share your requirements
- We review your brief and the systems you already use.
- We clarify the workflow, missing information and the work to consider first.
- The proposed scope sets out the deliverables, responsibilities and dependencies.
- Review the scope and commercial terms before deciding whether to proceed.
Start with your requirements
Describe your current process, the people involved and the change you need. Start with the details you know; we can clarify the rest together.
Share your requirements