Business solutions for Machine tool manufacturers
Explore software for work such as “CNC lathes and turning centres”. Review each business function below, including when it fits and what to check before implementation.
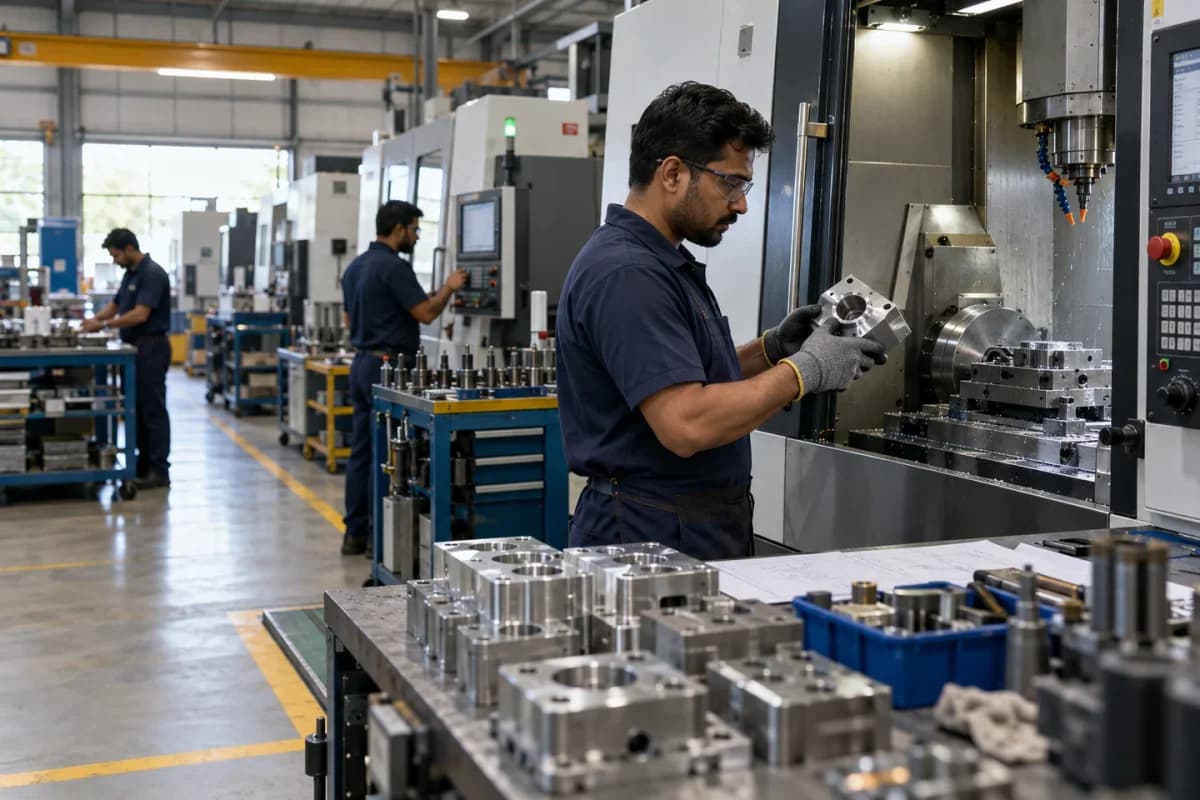
How the business operates.
A lathe or machining centre is a long chain of small tolerances. A bed is machined, guideways are ground or scraped, a spindle is fitted, and every step either keeps or loses accuracy.
The records that hold the operation together.
- Enquiries and application capture. Log the parts to be machined, material, tolerance and batch size with each enquiry, and keep the part drawings sent by the buyer.
- Quotations and option lists. Price machines from your tables for bed length, table size, spindle, turret or tool changer and controller, with every revision kept.
- Drawing and bill of materials control for machine tools. Release machine drawings and parts lists with a revision letter, so assembly builds the version that was ordered.
- Casting and bed machining. Receive castings by pattern and heat number and record stress relief, machining setups and fixtures for each bed.
- Guideway grinding and scraping. Log ways ground and scraped, the checks made and the fitter responsible, against the serial.
- Spindle, screw and guide records. Link spindle cartridges, ball screws, linear guides, motors and controllers to the machine by serial.
- Assembly stages. Move each machine through machining, scraping, assembly, wiring and run-in, with each stage signed off.
- Run-in and accuracy tests. Save spindle run-in logs and geometric and positioning results for each serial, in your engineers’ format.
Operational bottlenecks to check
Casting and bed history is lost
A bed is machined on a given date with a given fixture. An axis drifts later. The maker cannot trace what was done.
Spindle and screw serials are not tied to the machine
The supplier’s spindle cartridge number is on a delivery paper. The machine nameplate carries something else.
Run-in and test results are scattered
A spindle run-in log is kept by one fitter. Geometric and positioning results are saved by another. A buyer’s question reaches neither.
Options change the build late
A buyer adds a four-axis table or a tool changer after the order. The assembly bay learns too late.
Installation notes never return
The commissioning engineer adjusts levelling and parameters on site, yet the factory file still shows the test bay results recorded before the crate was closed.
Follow the work across teams.
This is a planning flow. Confirm the steps, owners and approval rules against your actual operation.
Roles and responsibility boundaries.
Reports your managers need.
- Machines in build, by stage and model
- Castings received and machined by pattern
- Spindles and screws issued by serial
- Accuracy tests done, passed and awaiting
- Open, won and lost quotations, by machine type
- Installations booked and completed
- Spares quoted, by model and machine age
Connections to scope
- SMS
- Accounting export
- Drawing file links
Confirm data access, record ownership and the exchange method for each connection. Inclusion here does not mean every connection is available in a standard package.
Setup decisions and adoption risks.
Use these requirements to plan phases, data migration and user training. Agree the release sequence after reviewing your current systems.
Limitations to settle before implementation
- A dealer that only resells imported machines should look at Heavy Equipment Dealer Management Software.
- A job shop that only uses machines may prefer Manufacturing Production Management Software.
Modules to consider first.
These functions connect to the operating model above. Confirm each one against the work your business actually runs.
Choose the operation you want to improve.
Use these activities to explain your scope. Your business does not need every function in the directory.
- CNC lathes and turning centres
- Vertical machining centres
- Horizontal machining centres
- Surface and cylindrical grinding machines
- Press brakes and shearing machines
- Dealer network in industrial towns
- Demo room and trial cuts on customer parts
- Spares and service engineer coverage
- Bank and NBFC finance for buyers
Explore the business functions.
Production, stock, fleet and recurring billing functions apply only where your business runs those activities. Read the suitability conditions on each page.
Manufacturing
Batch and Serial Tracking
Trace goods using batch identifiers or individual serial numbers.
View workflow and suitability →Bill of Materials
Define the materials and quantities needed for a manufactured item.
View workflow and suitability →Job Work Management
Track material sent to an outside processor and returned after work.
View workflow and suitability →Quality Control
Record specified inspections and the disposition of checked goods.
View workflow and suitability →Work Order Management
Track a production job from material issue to completed output.
View workflow and suitability →
Finance & Accounting
Field Service
Start with the problem your team can describe.
Bring a sample record and show where information is copied, missed or waiting for approval. Scope the first useful change from there.
What happens after you share your requirements
- We review your brief and the systems you already use.
- We clarify the workflow, missing information and the work to consider first.
- The proposed scope sets out the deliverables, responsibilities and dependencies.
- Review the scope and commercial terms before deciding whether to proceed.
Start with your requirements
Describe your current process, the people involved and the change you need. Start with the details you know; we can clarify the rest together.
Share your requirements