Quality Control for Machine tool manufacturers
Record specified inspections and the disposition of checked goods.
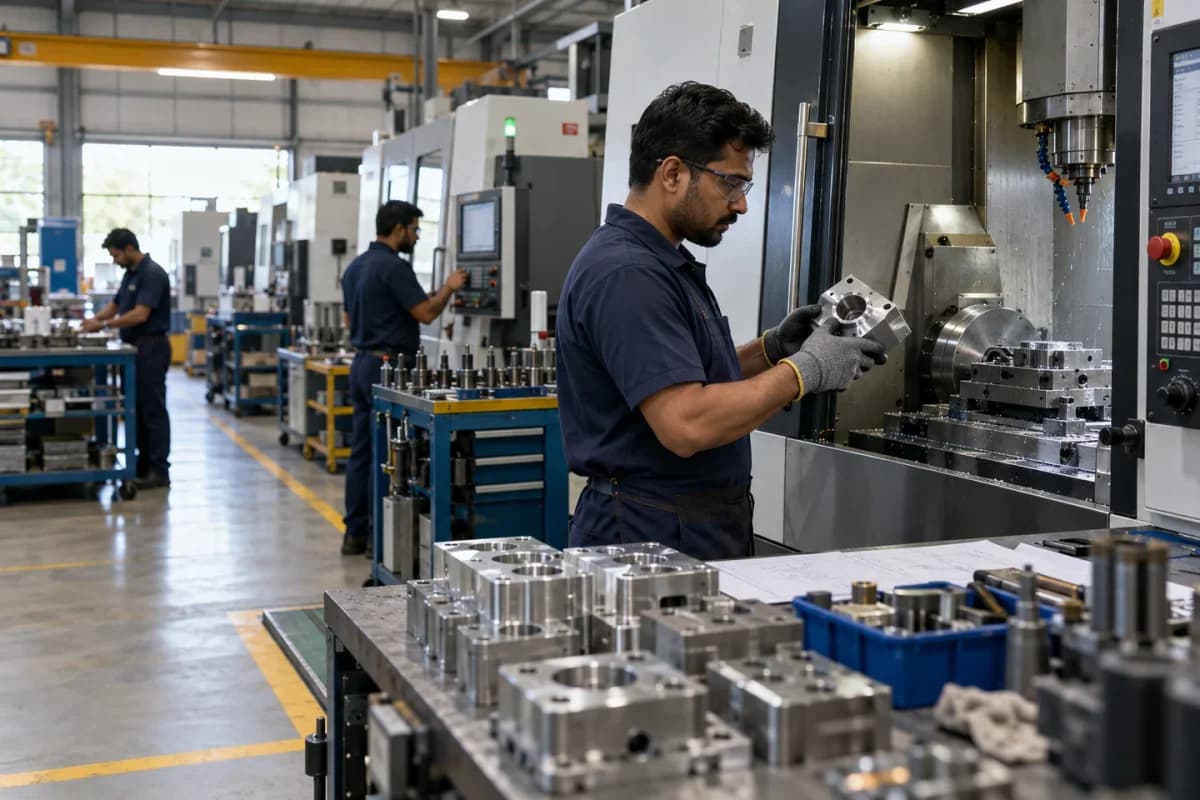
Does this function belong in your operation?
Use when goods or production stages require documented checks before release.
Material or output reaches an agreed inspection stage.
Records geometric tests such as straightness, spindle runout and positioning accuracy, with the instrument used. A machine that fails a run-in test stays in the shop. Results print with the certificate.
Bring the records the workflow depends on.
- Inspection specifications
- Sampling and acceptance rules
- Authorised reviewers
Outputs to check
- Inspection readings and evidence
- Hold, release or rejection record
- Nonconformance follow-up list
Follow the quality control workflow.
Use this sequence to compare your current process with the proposed module. Agree the owner, permission and exception at each step.
Who uses the module, and who approves?
Keep responsibilities distinct even when one person holds more than one role.
Decide how exceptions are handled.
These business rules belong in configuration and testing. A normal transaction alone does not demonstrate that the workflow is ready.
Can this work independently?
Quality records can be maintained independently against identifiable receipts or jobs. Inventory and production connections must enforce any hold or release decision. The module records authorised checks; it does not select a regulatory standard or replace a qualified inspector's judgement.
Systems and records it connects with
- Work orders: Released production jobs, material issues and output records.
- Goods receipt: Counted, accepted and rejected supplier-delivery quantities.
- Purchase returns: Approved supplier-return quantities and adjustment references.
- Batch and serial tracking: Lot or unit identifiers carried through stock movements.
Configure, test and introduce the workflow.
- Show us where checks happen now. A note names the checkpoints and the parameters to record.
- Provide limits and your list of rejection reasons. A test lot can then be checked on the trial screen. Checkers use it at a station for a trial run. Their remarks return as changes.
- Checkers, production and purchase each practise their part. Each group gets a printed card. Other stations join as the trial station settles. The team reviews rejection reasons together.
Check the result before rollout.
Apply these checks to a sample from the agreed workflow, then repeat with an exception. Keep the expected result beside the test record.
- Failed items follow the agreed hold rule.
- Results retain the specification version.
- Release decisions identify the reviewer.
How the business operates.
A lathe or machining centre is a long chain of small tolerances. A bed is machined, guideways are ground or scraped, a spindle is fitted, and every step either keeps or loses accuracy.
The records that hold the operation together.
- Enquiries and application capture. Log the parts to be machined, material, tolerance and batch size with each enquiry, and keep the part drawings sent by the buyer.
- Quotations and option lists. Price machines from your tables for bed length, table size, spindle, turret or tool changer and controller, with every revision kept.
- Drawing and bill of materials control for machine tools. Release machine drawings and parts lists with a revision letter, so assembly builds the version that was ordered.
- Casting and bed machining. Receive castings by pattern and heat number and record stress relief, machining setups and fixtures for each bed.
Operational bottlenecks to check
Casting and bed history is lost
A bed is machined on a given date with a given fixture. An axis drifts later. The maker cannot trace what was done.
Spindle and screw serials are not tied to the machine
The supplier’s spindle cartridge number is on a delivery paper. The machine nameplate carries something else.
How work flows across this business
This module sits within a wider operating process. Use the sequence to identify the other teams and records affected by a change.
1. Enquiry and application
The enquiry records parts, material, tolerance and batch. A model and options are shortlisted.
2. Quotation
The machine, accessories, installation and training are priced from your tables. Revisions are kept.
3. Order and drawing release
A confirmed order opens a serial. Drawings and parts lists are released with a revision letter.
4. Machining and assembly
Castings are machined, ways are ground and scraped, and the spindle, screws and guides are fitted.
5. Run-in and accuracy test
The spindle is run in and the machine is tested. Readings are saved against the serial.
6. Installation, training and spares
The machine is crated, installed and handed over. Operators are trained, and spares orders open from the record.
Industry reports to connect with
- Machines in build, by stage and model
- Castings received and machined by pattern
- Spindles and screws issued by serial
- Accuracy tests done, passed and awaiting
Questions before implementation.
When should machine tool manufacturers consider quality control?
Use when goods or production stages require documented checks before release. Material or output reaches an agreed inspection stage.
What should we bring to the requirements discussion?
Bring anonymised examples of Inspection specifications; Sampling and acceptance rules; Authorised reviewers. Show who creates, checks and changes each record. Use only records from an activity that meets the suitability conditions above.
Does this replace our existing business software?
The starting point is your current system and the gap you need to close. Record specified inspections and the disposition of checked goods. Configuration, a connected module or a custom build are evaluated against that gap before a replacement is proposed.
What is outside this module?
The software records your inspection process and does not certify product safety or regulatory conformity.
How are scope, price and rollout decided?
The proposal follows a review of your records, user roles, branches and existing software. Data migration, connections, training and support are scoped separately where needed. Failed items follow the agreed hold rule. Use this check when reviewing the first working version.
Related functions for machine tool manufacturers.
Discuss quality control for your business.
Tell us which workflow needs attention and which systems your team uses. The next step is a requirements discussion and a written scope.
What happens after you share your requirements
- We review your brief and the systems you already use.
- We clarify the workflow, missing information and the work to consider first.
- The proposed scope sets out the deliverables, responsibilities and dependencies.
- Review the scope and commercial terms before deciding whether to proceed.
Start with your requirements
Describe your current process, the people involved and the change you need. Start with the details you know; we can clarify the rest together.
Share your requirements