Job Work Management for Rubber gasket manufacturers
Track material sent to an outside processor and returned after work.
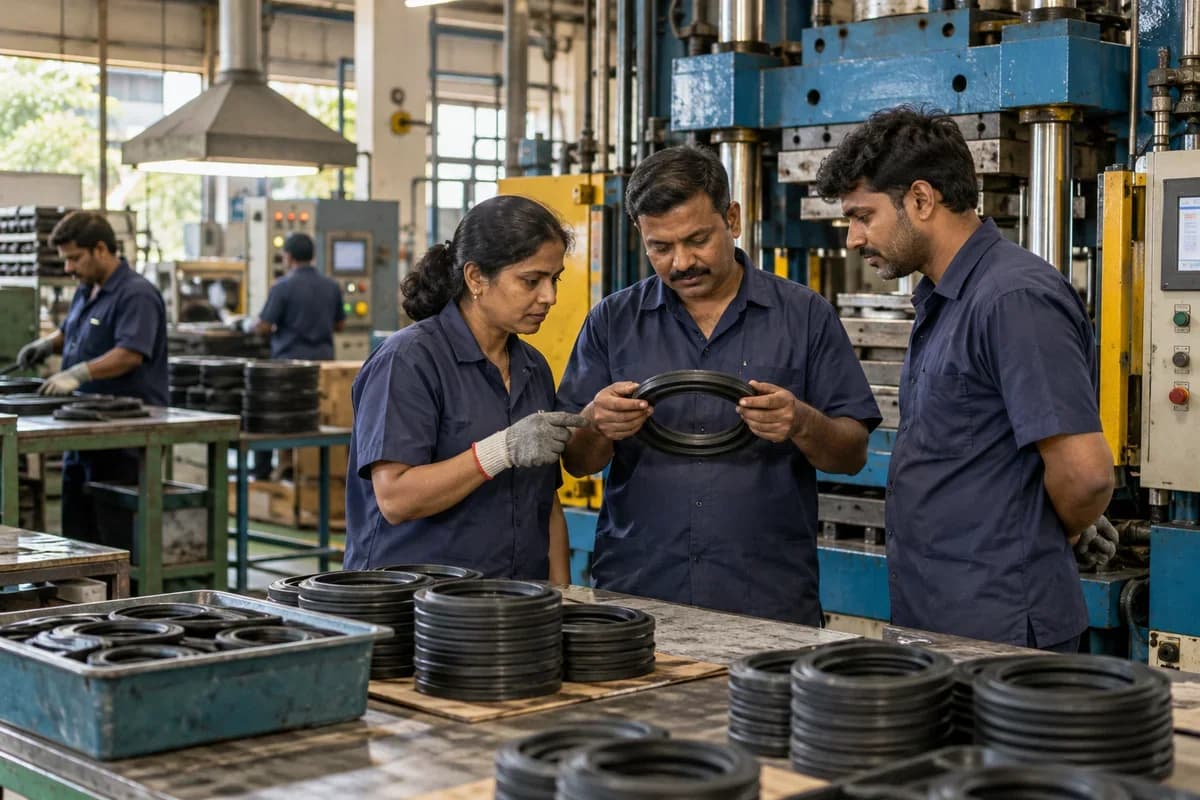
Does this function belong in your operation?
Use when your materials leave for processing and must be reconciled on return.
A production stage is subcontracted with material supplied by your business.
Parts sent to an outside shop for bonding, or sheets cut for another fabricator, leave with a note of count and weight. The store sees what is still out. Returns are checked against it.
Bring the records the workflow depends on.
- Vendor and process details
- Material quantities
- Return and wastage terms
Outputs to check
- Subcontract dispatch and return register
- Processor-held material balance
- Job-work charge reconciliation
Follow the job work management workflow.
Use this sequence to compare your current process with the proposed module. Agree the owner, permission and exception at each step.
Who uses the module, and who approves?
Keep responsibilities distinct even when one person holds more than one role.
Decide how exceptions are handled.
These business rules belong in configuration and testing. A normal transaction alone does not demonstrate that the workflow is ready.
Can this work independently?
This can track outside processing with entered dispatch and receipt records. Stock and accounting connections reconcile material ownership and processing charges; quality control decides acceptance. A vendor's completion message is not a physical return or proof that the returned output meets specification.
Systems and records it connects with
- Work orders: Released production jobs, material issues and output records.
- Stock: Item-location quantities and authorised stock movements.
- Vendor bills: Supplier invoice lines and authorised posting status.
- Purchase returns: Approved supplier-return quantities and adjustment references.
Configure, test and introduce the workflow.
- We list the outside processes you use and the vendors for each. You describe how notes and returns are handled today. A flow diagram comes back for your approval.
- Rates, process names and wastage allowances are entered. You confirm them with the production team. Material currently lying outside is loaded from your registers. The store team checks balances with the vendors. Mistakes surface early.
- New outward notes are made on the screen while the old book continues. Returns are booked and compared. The team is trained. The paper book is retired. The oldest balances are reviewed at the next meeting.
Check the result before rollout.
Apply these checks to a sample from the agreed workflow, then repeat with an exception. Keep the expected result beside the test record.
- Sent and returned quantities reconcile.
- Material held by each processor remains visible.
- Charges link to the relevant job.
How the business operates.
A rubber gasket shop supplies the flat ring, the full-face gasket, the door seal and the sump gasket. Each sits between two parts. Its job is to keep a fluid or a gas where it belongs. Some are cut from sheets of nitrile, EPDM, neoprene or silicone with steel rule dies, a water jet or a knife cutter. Others are moulded or extruded and joined into loops. Each type needs its own record.
The records that hold the operation together.
- Part numbers, drawings and patterns. Hold sketch, rubbing, DXF and revision under one part number, with compound, Shore hardness and tolerance band.
- Quotations by sheet yield. Price a gasket from sheet cost, expected nesting yield, knife time and finishing, then set the figure beside the yield the job actually returned.
- Sheet and profile stock. Receive sheets by compound, hardness, thickness and size, and extruded profile by section and coil length, then issue each against jobs.
- Offcut register. Return leftover sheet with its dimensions to stock, so the next small order is cut from a remnant before a full sheet leaves the rack.
Operational bottlenecks to check
Drawings arrive in whatever form the buyer sends
A hand sketch, a photo of an old gasket and a drawing file all arrive for the same part. With no revision on record, a repeat order is cut from whichever copy turns up first, and the buyer sees the difference.
Nesting waste is invisible
Operators nest parts on a sheet by eye, and the offcut goes on a pile. The yield of each job is unknown, so quotes ignore it. Waste is money on a pile.
How work flows across this business
This module sits within a wider operating process. Use the sequence to identify the other teams and records affected by a change.
1. Enquiry and pattern
A buyer sends a sketch, a drawing or a worn gasket. The estimator records inside diameter, outside diameter, bolt circle, hole count, thickness and compound, and files the rubbing.
2. Cutting file or die
A knife file or steel rule die is made and filed under the part number. A first piece is cut and checked against the drawing with a vernier caliper.
3. Sheet issue
Stores issue sheets by compound, Shore hardness and thickness. The operator nests the parts on the plotter bed, and the sheet area used is written to the order.
4. Cutting and finishing
Parts are cut by clicker press, oscillating knife or water jet. Bolt holes are punched, edges cleaned and pressure sensitive backing applied where the drawing asks.
5. Splicing and inspection
Extruded profile is mitred to length and bonded into loops. Inspectors check bolt hole positions, thickness and the corner bond with a pull test.
6. Kit, pack and deliver
Parts are counted into labelled bags or kits, and a delivery note naming the compound travels with the carton. The invoice follows.
Industry reports to connect with
- Orders by stage with sheet area used
- Nesting yield by job, compound and operator
- Offcut stock by compound and size
- Dies and blades past their impression limit
Questions before implementation.
When should rubber gasket manufacturers consider job work management?
Use when your materials leave for processing and must be reconciled on return. A production stage is subcontracted with material supplied by your business.
What should we bring to the requirements discussion?
Bring anonymised examples of Vendor and process details; Material quantities; Return and wastage terms. Show who creates, checks and changes each record. Use only records from an activity that meets the suitability conditions above.
Does this replace our existing business software?
The starting point is your current system and the gap you need to close. Track material sent to an outside processor and returned after work. Configuration, a connected module or a custom build are evaluated against that gap before a replacement is proposed.
What is outside this module?
This concerns outsourced physical processing, not general professional-services subcontracting.
How are scope, price and rollout decided?
The proposal follows a review of your records, user roles, branches and existing software. Data migration, connections, training and support are scoped separately where needed. Sent and returned quantities reconcile. Use this check when reviewing the first working version.
Related functions for rubber gasket manufacturers.
Discuss job work management for your business.
Tell us which workflow needs attention and which systems your team uses. The next step is a requirements discussion and a written scope.
What happens after you share your requirements
- We review your brief and the systems you already use.
- We clarify the workflow, missing information and the work to consider first.
- The proposed scope sets out the deliverables, responsibilities and dependencies.
- Review the scope and commercial terms before deciding whether to proceed.
Start with your requirements
Describe your current process, the people involved and the change you need. Start with the details you know; we can clarify the rest together.
Share your requirements