Business solutions for Adhesive manufacturers
Explore software for work such as “A mason and tiler register with training sessions”. Review each business function below, including when it fits and what to check before implementation.
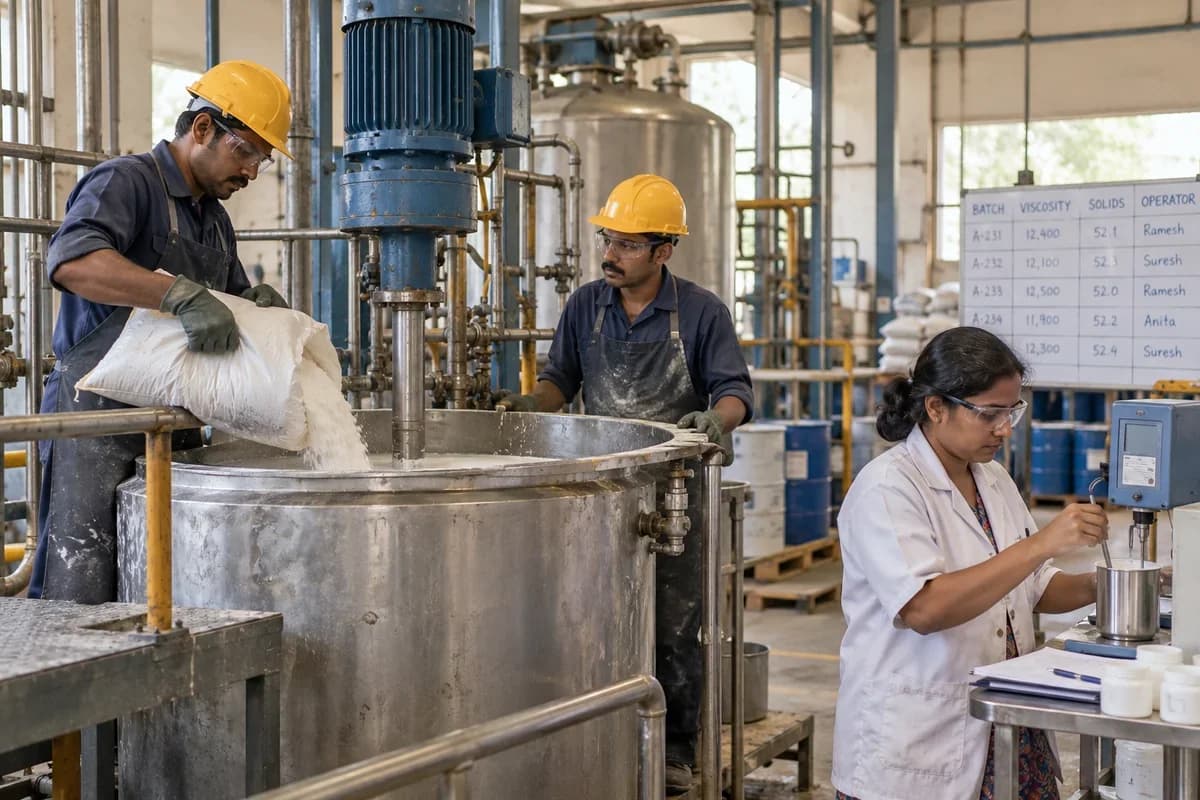
How the business operates.
Adhesives are judged by whether they hold. A carton maker wants a glue that sets at line speed, a footwear factory wants a bond that survives flexing, and a woodworker wants an open time that fits the press. Each need leads to a different formulation. None is interchangeable.
The records that hold the operation together.
- Grades and formulations. Hold recipe revisions for every grade, with allowed substitutions of tackifier or plasticiser and quantities scaled to the kettle size.
- Raw material lots. Record resin, polymer, solvent and additive lots with incoming viscosity and solids. Each lot links to every batch that drew from it.
- Kettle batch records. Capture charging order, jacket temperature, dispersion blade speed, mixing time and the operator for each kettle batch.
- Viscosity and solids. Save Brookfield viscosity, solids content and pH against the batch. Readings are compared with each grade’s limits before release.
- Bond strength tests. Record T-peel, lap shear, open time and pot life with the substrate, press load and curing conditions used on the test strip.
- Filling lines and changeovers. Log fill weights, container counts, purge steps, nozzle swaps and first-off checks on pail, drum, tube and cartridge lines.
- Lot codes and shelf life. Print batch codes and use-by dates on every container. List batches by remaining life so slow hot melt slugs surface early.
- Customer approvals. Hold the grade each customer approved, their peel and viscosity limits and the data sheet revision they were sent.
Operational bottlenecks to check
Viscosity drifts between batches
The same recipe gives a thicker batch when a resin lot changes. Readings sit in a notebook. The pattern is never seen.
Bond tests are not tied to the batch
A peel strength result is written on a test strip. Weeks on, nobody can say which pail in the customer’s store it describes.
Pot life and open time are guesses
The customer’s line needs a set open time. The plant relies on memory.
Shelf life runs out in the warehouse
Slow-moving grades sit in pails past their use-by date. Without an expiry list, they are found by chance.
Filling lines change over without a record
A cartridge line moves from one grade to another. Cleaning and first-off checks are done but not written down.
Follow the work across teams.
This is a planning flow. Confirm the steps, owners and approval rules against your actual operation.
Roles and responsibility boundaries.
Reports your managers need.
- Brookfield viscosity and solids by kettle batch and grade
- Peel and lap shear results against customer limits
- Resin and polymer lots used in a chosen batch
- Pails, drums and cartridges filled by batch code
- Grades by remaining shelf life
- Changeovers and purge steps logged on filling lines
- Orders open by customer and grade
Connections to scope
- SMS
- Label printer
- Laboratory instrument import
- Accounting export
Confirm data access, record ownership and the exchange method for each connection. Inclusion here does not mean every connection is available in a standard package.
Setup decisions and adoption risks.
Use these requirements to plan phases, data migration and user training. Agree the release sequence after reviewing your current systems.
Limitations to settle before implementation
- A company that only buys glue to run its own gluing machines is better served by Manufacturing Production Management Software.
- A maker of paints and coatings may prefer Specialty Chemical Manufacturer Management Software.
Modules to consider first.
These functions connect to the operating model above. Confirm each one against the work your business actually runs.
Choose the operation you want to improve.
Use these activities to explain your scope. Your business does not need every function in the directory.
- A mason and tiler register with training sessions
- A tile dealer and hardware list by town with the brand each carries
- A usage guide by surface: vitrified, stone, wall tile, plywood
- A coverage comparison that shows cost per square foot
- A bag and batch check so duplicates can be spotted
- A project pack for builders and consultants
- A dealer scheme for towns where tile shops lead recommendations
Explore the business functions.
Production, stock, fleet and recurring billing functions apply only where your business runs those activities. Read the suitability conditions on each page.
Retail and POS
Manufacturing
Batch and Serial Tracking
Trace goods using batch identifiers or individual serial numbers.
View workflow and suitability →Bill of Materials
Define the materials and quantities needed for a manufactured item.
View workflow and suitability →Production Planning
Plan manufacturing quantities against demand, materials and capacity.
View workflow and suitability →Quality Control
Record specified inspections and the disposition of checked goods.
View workflow and suitability →
Inventory Management
Product Management
Maintain the item definitions used by sales, purchasing and stock.
View workflow and suitability →Purchase Order Management
Record authorised supplier orders and track what remains due.
View workflow and suitability →Stock Tracking and Alerts
Record stock movements and flag items reaching configured levels.
View workflow and suitability →
Start with the problem your team can describe.
Bring a sample record and show where information is copied, missed or waiting for approval. Scope the first useful change from there.
What happens after you share your requirements
- We review your brief and the systems you already use.
- We clarify the workflow, missing information and the work to consider first.
- The proposed scope sets out the deliverables, responsibilities and dependencies.
- Review the scope and commercial terms before deciding whether to proceed.
Start with your requirements
Describe your current process, the people involved and the change you need. Start with the details you know; we can clarify the rest together.
Share your requirements