Business solutions for Automation equipment manufacturers
Explore software for work such as “Servo and frequency drives”. Review each business function below, including when it fits and what to check before implementation.
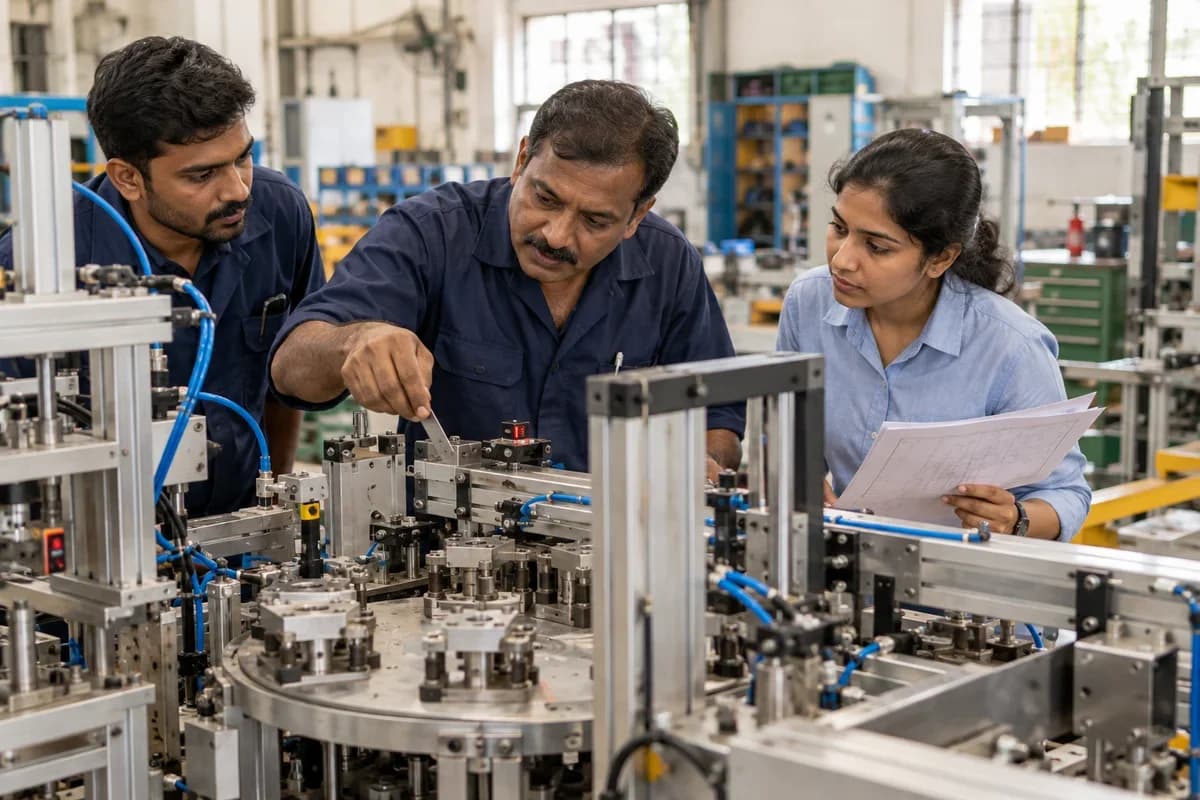
How the business operates.
These machines are one-offs or short runs. The buyer describes a product and a target cycle time, and the maker designs a station that assembles, tests or packs it. Parts come from machine shops, catalogue suppliers and the maker’s own workshop. Weeks before delivery go on chasing a few late items. A frame cannot be closed until one bracket arrives.
The records that hold the operation together.
- Machine enquiry and estimate. Estimate design hours, machined parts, bought-in components, assembly and test time on one sheet, and keep the figure as the project budget that posted cost is compared with later. No second copy.
- Parts list with revision. Hold each assembly, machined part and catalogue item with its revision letter, and after release a change shows what moved and which open orders still carry the old drawing. Nothing is overwritten.
- Machined part orders. Release a drawing set to the workshop or to an outside machinist, with the due date and the stock material named per plate. Returned shafts and brackets are booked in line by line. Short deliveries stay open.
- Component purchasing and receipt. Order catalogue items straight from the released list, follow promised dates, and receive each pneumatic cylinder, proximity sensor or servo motor against the machine it belongs to. Gaps are visible.
- Assembly and wiring stages. Plan frame build, station assembly, air piping, panel wiring and PLC programming as stages, each with named fitters, dates and booked hours. A stage closes only on sign-off.
- Project schedule. Lay design, machining, assembly and buy-off on a single timeline, so a late machined plate shows the exact stage it blocks and the fitters it idles. Dates move together.
- Buy-off and punch list. Record run-off tests on the customer’s own parts and log each remark as a punch item with an owner and a closing date. Every item closes before the crate does.
- Machine cost against estimate. Post design hours, workshop time and purchase invoices to the machine and read them beside the estimate while the build is under way. Overruns appear early.
Operational bottlenecks to check
The bill of materials changes during build
Designers revise parts while the workshop is already machining. Plates cut to the old drawing are scrapped and new ones ordered, and the difference sits in no single record, so the true cost of the revision is never read.
Bought-in parts arrive out of sequence
Cylinders arrive on Monday, sensors the week after, and the servo motors only when the supplier clears its own backlog. Fitters wait for a bracket. Or they build around the gap and strip it back later.
Outside machining is tracked by phone
Parts sent to outside machinists have no delivery date on record. Assembly week arrives. The shafts are still out, and the slip goes unseen until a fitter asks.
Buy-off issues are carried in memory
Run-off comments go on paper. Some are lost before the crate is nailed shut. A reject chute that was promised a change ships unchanged.
Real project cost is learned late
Design hours sit in one file, workshop time in another, and bought-in parts in the purchase ledger. Margin shows up after delivery. Every quote is a guess.
Follow the work across teams.
This is a planning flow. Confirm the steps, owners and approval rules against your actual operation.
Roles and responsibility boundaries.
Reports your managers need.
- Machines on the floor by build stage and due date
- Missing catalogue items per machine and supplier
- Outside machining due and overdue by machinist
- Estimate against posted cost by machine
- Open punch items per machine, oldest first
- Warranty expiry by delivered serial number
- Spares sold by machine model
Connections to scope
- Document storage
- Supplier order email
- Accounting export
- SMS
Confirm data access, record ownership and the exchange method for each connection. Inclusion here does not mean every connection is available in a standard package.
Setup decisions and adoption risks.
Use these requirements to plan phases, data migration and user training. Agree the release sequence after reviewing your current systems.
Limitations to settle before implementation
- A firm that builds only electrical control panels is better served by PLC Panel Builder Management Software.
- A plant that makes the same product in high volume is better served by Manufacturing Production Management Software.
Modules to consider first.
These functions connect to the operating model above. Confirm each one against the work your business actually runs.
Choose the operation you want to improve.
Use these activities to explain your scope. Your business does not need every function in the directory.
- Servo and frequency drives
- PLCs and HMIs
- Sensors and encoders
- Power supplies and relays
- Motion control and actuators
- Distributor stocking and training
- Application engineering support
- OEM design-in and repeat supply
- Warranty, repair and replacement handling
Explore the business functions.
Production, stock, fleet and recurring billing functions apply only where your business runs those activities. Read the suitability conditions on each page.
Manufacturing
Bill of Materials
Define the materials and quantities needed for a manufactured item.
View workflow and suitability →Job Work Management
Track material sent to an outside processor and returned after work.
View workflow and suitability →Quality Control
Record specified inspections and the disposition of checked goods.
View workflow and suitability →Work Order Management
Track a production job from material issue to completed output.
View workflow and suitability →
Finance & Accounting
Procurement
Project Management
Helpdesk
Start with the problem your team can describe.
Bring a sample record and show where information is copied, missed or waiting for approval. Scope the first useful change from there.
What happens after you share your requirements
- We review your brief and the systems you already use.
- We clarify the workflow, missing information and the work to consider first.
- The proposed scope sets out the deliverables, responsibilities and dependencies.
- Review the scope and commercial terms before deciding whether to proceed.
Start with your requirements
Describe your current process, the people involved and the change you need. Start with the details you know; we can clarify the rest together.
Share your requirements