Business solutions for CNC machining companies
Explore software for work such as “Five-axis CNC machining”. Review each business function below, including when it fits and what to check before implementation.
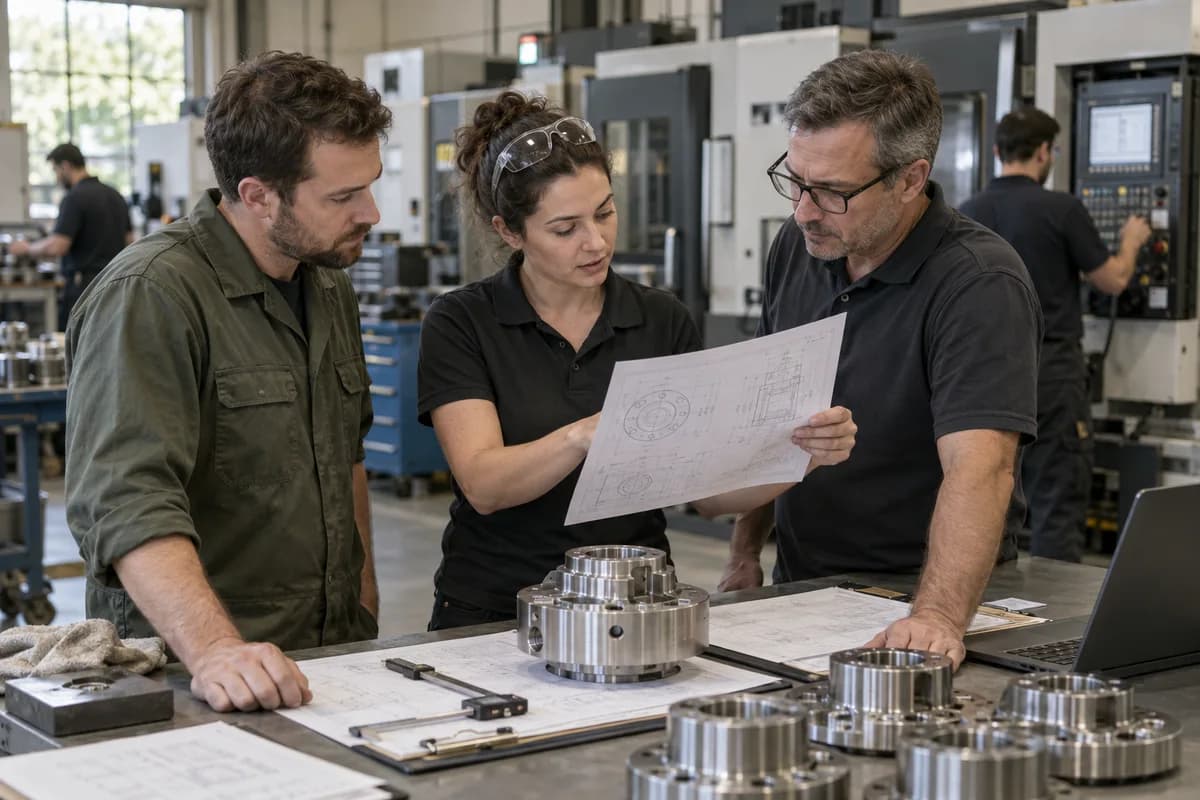
How the business operates.
You run Swiss-type and chucker turning centres, a few VMCs with tombstone fixtures and a centreless grinder, making shafts, trunnions, pinions and hydraulic adaptors to someone else’s drawing. Concentricity, roundness and surface roughness limits are tight. Quantities swing from order to order, and the buyer’s quality engineer reads your first-article approval file and inspection report long before the invoice is looked at.
The records that hold the operation together.
- Enquiries and production quotations. Log buyer enquiries with the drawing or sample attached, then cost bar weight, machine minutes and outside plating before a price goes back to the purchasing desk. Every costing revision is kept.
- Sales orders and delivery commitments. Hold confirmed orders with part number, drawing revision, quantity, rate, schedule and the delivery week promised to the buyer, so a balance after each part delivery is always visible. Late orders stand out.
- Multi-level bill of materials and routing. Keep each part’s material list and stage sequence. Drawing revisions, scrap allowance, the CNC lathe or press brake each stage runs on and the fixture it needs sit beside it. A sub-assembly carries its own list.
- Work orders and batch planning. Release a work order for a batch, set its target date, and see the load already queued on each machine and stage. Planners move dates by hand. Overloaded stages stand out.
- Job cards by production stage. Record quantity passed, rejected and held at sawing, turning, milling, welding, assembly, painting and packing, stage by stage, against the batch quantity on the work order. Each card names the operator and shift.
- Raw material and consumable stock. Count bright bar, billets, sheets, castings, forgings, resin, fasteners, shrink film and consumables by grade and size, with every issue carrying a work order number. Heat numbers stay with their stock.
- Purchase orders and supplier records. Raise orders on material suppliers from the shortage list, receive against them with inspection, and keep the supplier ledger and rate history. Rejected lots show by supplier.
- Quality checks and rejections. Save inspection readings from vernier, bore gauge and torque wrench checks, count rejection, rework and scrap by stage and reason, and hold a batch until it is cleared. First-off approval and final inspection share one record. Each batch traces back to its work order.
Operational bottlenecks to check
The wrong drawing revision reaches the machine
A buyer revises a tolerance by mail, yet the setter still holds last month’s printout beside the control panel and runs the whole lot of pinions to it. The gauge disagrees at the gate.
Setup and first-piece time go uncounted
Quotes assume a cycle time, but changeovers, first-piece approval, a worn collet, a blunt reamer, swarf clearing and the wait for a thread ring gauge use up whole shifts. Those hours go uncounted.
Rejections surface only at month end
Pieces fail on a bore diameter, ovality, an undercut, a chamfer or a thread at in-process checks, final inspection or the buyer’s gate, and the reason is rarely written. Month end shows only a total.
A failed lot cannot be traced to its bar
The buyer asks which bar went into a lot that failed, and the mill certificate for that heat is somewhere in a file box. Tracing it takes hours.
Job work quantities never reconcile
Shafts go out for induction hardening and come back short, or with a few pieces bent past straightening, and the dispatch book cannot say which. The vendor disputes the count.
Follow the work across teams.
This is a planning flow. Confirm the steps, owners and approval rules against your actual operation.
Roles and responsibility boundaries.
Reports your managers need.
- Work orders still open, grouped by stage and promised week
- Production by stage, machine and operator each shift
- Material consumed against the bill of materials
- Rejection and scrap by stage and reason
- Job work out, returned and short, by job worker
- Bar, sheet and resin stock against shortages
- Dispatches and buyer outstanding by order
Connections to scope
- SMS
- Payment links and gateways
- Accounting software export (quoted separately)
- Barcode or label printers
- Weighing scales
- Biometric attendance devices
Confirm data access, record ownership and the exchange method for each connection. Inclusion here does not mean every connection is available in a standard package.
Setup decisions and adoption risks.
Use these requirements to plan phases, data migration and user training. Agree the release sequence after reviewing your current systems.
Limitations to settle before implementation
- A firm that only buys and resells, with no making at all, should look at our wholesale ordering product instead.
- A single craftsman working to order with no stages, store or job work may find a notebook and a basic invoicing app enough.
- A plant that runs continuous process control from instruments, with loops tuned on a control panel, needs plant automation rather than a production record system.
Modules to consider first.
These functions connect to the operating model above. Confirm each one against the work your business actually runs.
Choose the operation you want to improve.
Use these activities to explain your scope. Your business does not need every function in the directory.
- Five-axis CNC machining
- Precision turned components
- Prototype and low-volume runs
- Titanium and exotic alloy machining
- Sheet metal fabrication
- Export orders and international buyers
- Auto ancillary contract manufacturing
- Quality certification and inspection reporting
Explore the business functions.
Production, stock, fleet and recurring billing functions apply only where your business runs those activities. Read the suitability conditions on each page.
Manufacturing
Bill of Materials
Define the materials and quantities needed for a manufactured item.
View workflow and suitability →Job Work Management
Track material sent to an outside processor and returned after work.
View workflow and suitability →Production Planning
Plan manufacturing quantities against demand, materials and capacity.
View workflow and suitability →Quality Control
Record specified inspections and the disposition of checked goods.
View workflow and suitability →Work Order Management
Track a production job from material issue to completed output.
View workflow and suitability →
CRM
Inventory Management
Start with the problem your team can describe.
Bring a sample record and show where information is copied, missed or waiting for approval. Scope the first useful change from there.
What happens after you share your requirements
- We review your brief and the systems you already use.
- We clarify the workflow, missing information and the work to consider first.
- The proposed scope sets out the deliverables, responsibilities and dependencies.
- Review the scope and commercial terms before deciding whether to proceed.
Start with your requirements
Describe your current process, the people involved and the change you need. Start with the details you know; we can clarify the rest together.
Share your requirements