Stock Tracking and Alerts for PCB assembly companies
Record stock movements and flag items reaching configured levels.
Does this function belong in your operation?
Use when the business holds physical stock or consumables requiring quantity control.
Goods are received, issued, transferred or counted.
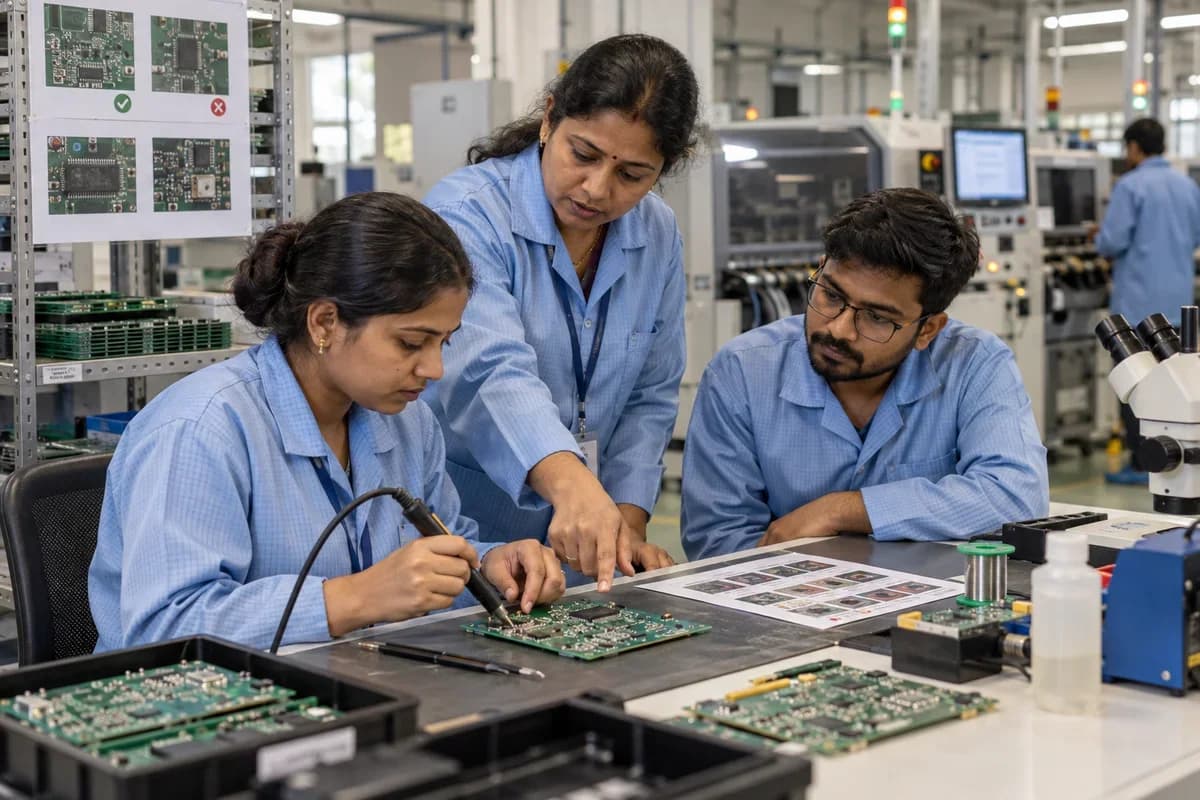
Resistors, capacitors and ICs are counted by reel, tray and loose cut tape. A reel started on the line keeps its remaining count. Shortfalls for coming builds show early.
Bring the records the workflow depends on.
- Item and location list
- Opening quantities
- Reorder and movement rules
Outputs to check
- Item-location balance register
- Movement and count-adjustment history
- Replenishment exception list
Follow the stock tracking and alerts workflow.
Use this sequence to compare your current process with the proposed module. Agree the owner, permission and exception at each step.
Who uses the module, and who approves?
Keep responsibilities distinct even when one person holds more than one role.
Decide how exceptions are handled.
These business rules belong in configuration and testing. A normal transaction alone does not demonstrate that the workflow is ready.
Can this work independently?
Stock tracking can run from entered receipts and issues, but every physical movement needs a record. Purchase, sales, production and warehouse connections provide those movements. Reorder alerts signal a threshold; purchasing still decides quantity, supplier and approval.
Systems and records it connects with
- Purchase order management: Authorised supplier commitments and open line balances.
- Goods receipt: Counted, accepted and rejected supplier-delivery quantities.
- Point of sale billing: Counter sales, tender records and authorised returns.
- Multi-outlet stock: Outlet quantities and acknowledged transfer movements.
Configure, test and introduce the workflow.
- Show us the godown and the counters. A note lists the locations and the item groups.
- Supply levels per item and place, or ask for suggestions from history. Balances and alerts then appear for trial. A count is taken and loaded as the opening balance. The team checks a sample against the shelf.
- Each group practises receipts, issues and transfers. Short cards for the shelves follow. Alerts reach named people. A review once the opening season ends lists slow stock.
Check the result before rollout.
Apply these checks to a sample from the agreed workflow, then repeat with an exception. Keep the expected result beside the test record.
- Movements reconcile with location balances.
- Count adjustments retain approval.
- Alerts use the correct item and location threshold.
How the business operates.
An assembly job is won or lost on small things. A reel with the wrong resistor value. Solder paste past its jar life. A moisture-sensitive BGA left out of the bake cycle. Each one is cheap to prevent and costly once boards are reflowed, tested and packed for a customer who expects them on Friday.
The records that hold the operation together.
- Enquiries and quotations. Price an assembly from bill of materials cost, stencil, feeder setup, line time, test and assumed first-pass yield, and keep every revision of the quote for the next repeat order.
- Board BOMs and alternate parts. Hold reference designators, quantity per board, approved alternates and revision letter, and flag a substitution that the customer has not approved before the kit is pulled.
- Component purchase and receipt. Raise orders for shortages, record reels received with supplier lot, date code and moisture class, and send sensitive parts to the bake oven before they reach a shelf.
- Reel and lot traceability. Link each reel to the assembly lot that consumed it, so a field return leads to the exact supplier lots and date codes on that board.
Operational bottlenecks to check
Reels are not tied to the boards
A reel of 10 kilo-ohm resistors is loaded on feeder 14 with no lot number noted. When a board comes back dead from a customer, the paper trail stops at the feeder bank.
Paste and stencils are managed by feel
Solder paste has a shelf life and an open-jar life, and every stencil has a print count, yet neither is logged against the lot that used it. Squeegee wear goes unseen.
How work flows across this business
This module sits within a wider operating process. Use the sequence to identify the other teams and records affected by a change.
1. Enquiry and quotation
The customer’s bill of materials is loaded and priced with component cost, stencil, line time and test. Alternates are flagged for the customer’s approval before the quote goes out.
2. Purchase and receipt
Missing parts are ordered. Reels are received with supplier lot, date code and moisture sensitivity level, and sensitive devices go to the bake queue before they reach a shelf or a feeder.
3. Kitting
A job kit is counted against the bill of materials, line by line, and shortages are listed by reference designator. The job is released only when the kit is complete or the customer approves it short.
4. Print, place and reflow
The stencil, paste jar, feeder setup, placement program and reflow profile are recorded for the lot. Boards pass solder paste inspection before placement. Automated optical inspection checks them again after the oven.
5. Through-hole, test and rework
Hand-inserted and wave-soldered parts are logged against the lot. In-circuit and functional tests record results by board serial, and failures go to the rework bench with a record of the fault.
6. Pack and deliver
Shipping paperwork states boards built, scrapped and shipped, and names the reel lots consumed. The certificate of conformance is printed from the same lot. Nothing is retyped.
Industry reports to connect with
- Kits short, by job and part
- First-pass yield by board type and line
- Reels consumed by assembly lot
- Paste jars and stencils nearing limits
Questions before implementation.
When should pcb assembly companies consider stock tracking and alerts?
Use when the business holds physical stock or consumables requiring quantity control. Goods are received, issued, transferred or counted.
What should we bring to the requirements discussion?
Bring anonymised examples of Item and location list; Opening quantities; Reorder and movement rules. Show who creates, checks and changes each record. Use only records from an activity that meets the suitability conditions above.
Does this replace our existing business software?
The starting point is your current system and the gap you need to close. Record stock movements and flag items reaching configured levels. Configuration, a connected module or a custom build are evaluated against that gap before a replacement is proposed.
What is outside this module?
Recorded balances depend on timely movement entries. Physical availability must be confirmed through the agreed count and reservation process.
How are scope, price and rollout decided?
The proposal follows a review of your records, user roles, branches and existing software. Data migration, connections, training and support are scoped separately where needed. Movements reconcile with location balances. Use this check when reviewing the first working version.
Related functions for pcb assembly companies.
Discuss stock tracking and alerts for your business.
Tell us which workflow needs attention and which systems your team uses. The next step is a requirements discussion and a written scope.
What happens after you share your requirements
- We review your brief and the systems you already use.
- We clarify the workflow, missing information and the work to consider first.
- The proposed scope sets out the deliverables, responsibilities and dependencies.
- Review the scope and commercial terms before deciding whether to proceed.
Start with your requirements
Describe your current process, the people involved and the change you need. Start with the details you know; we can clarify the rest together.
Share your requirements