Business solutions for PCB assembly companies
Explore software for work such as “Prototype and pilot lots for hardware startups”. Review each business function below, including when it fits and what to check before implementation.
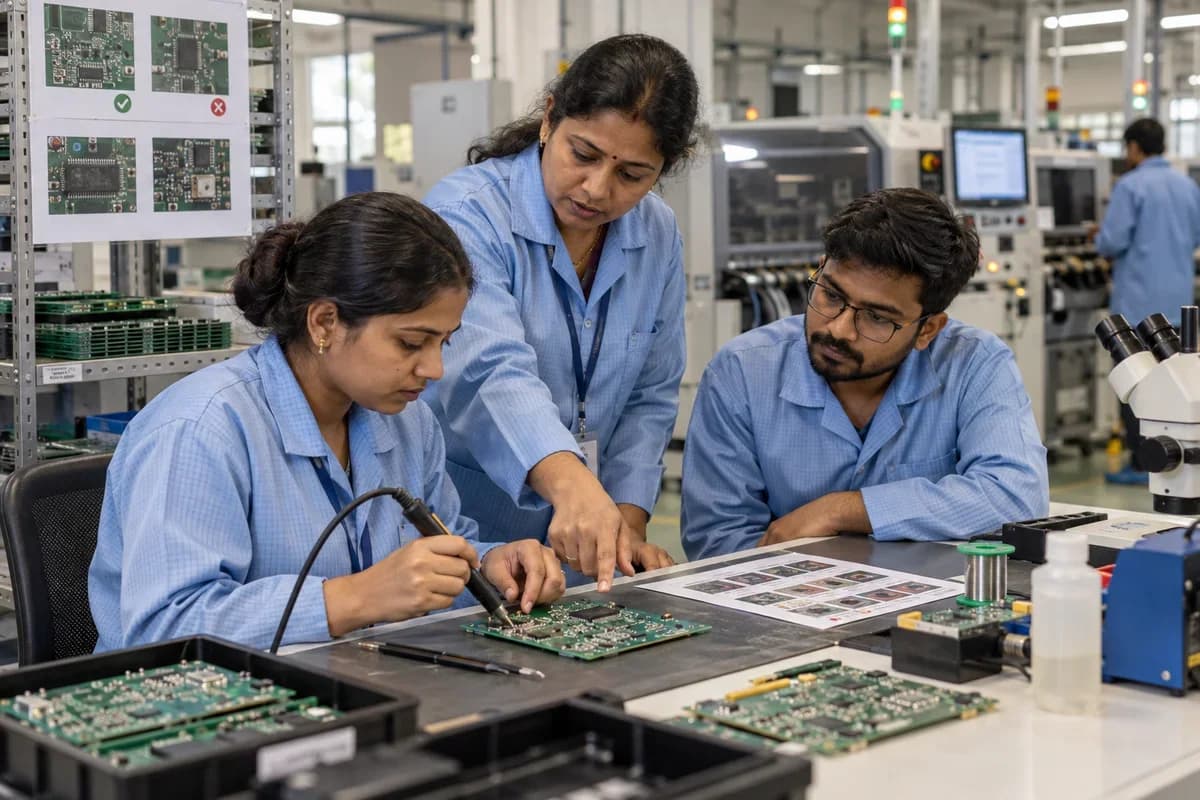
How the business operates.
An assembly job is won or lost on small things. A reel with the wrong resistor value. Solder paste past its jar life. A moisture-sensitive BGA left out of the bake cycle. Each one is cheap to prevent and costly once boards are reflowed, tested and packed for a customer who expects them on Friday.
The records that hold the operation together.
- Enquiries and quotations. Price an assembly from bill of materials cost, stencil, feeder setup, line time, test and assumed first-pass yield, and keep every revision of the quote for the next repeat order.
- Board BOMs and alternate parts. Hold reference designators, quantity per board, approved alternates and revision letter, and flag a substitution that the customer has not approved before the kit is pulled.
- Component purchase and receipt. Raise orders for shortages, record reels received with supplier lot, date code and moisture class, and send sensitive parts to the bake oven before they reach a shelf.
- Reel and lot traceability. Link each reel to the assembly lot that consumed it, so a field return leads to the exact supplier lots and date codes on that board.
- Kitting and shortages. Count a kit against the bill of materials, show which reference designators are short, and hold the job until parts arrive or the customer signs off a short kit.
- Paste, stencil and bake logs. Record paste jar open life, stencil print count and the out-of-bag hours of moisture-sensitive devices against each lot, with a warning as a limit nears.
- Line setup library. Store feeder positions, placement program and reflow profile for each board, so a repeat lot loads the setup already approved instead of a fresh trial-and-error one.
- Inspection, test and rework. Every AOI, X-ray and in-circuit result is filed under the board serial, next to the defect, the part swapped and the technician who reworked it.
Operational bottlenecks to check
Reels are not tied to the boards
A reel of 10 kilo-ohm resistors is loaded on feeder 14 with no lot number noted. When a board comes back dead from a customer, the paper trail stops at the feeder bank.
Paste and stencils are managed by feel
Solder paste has a shelf life and an open-jar life, and every stencil has a print count, yet neither is logged against the lot that used it. Squeegee wear goes unseen.
Moisture-sensitive parts miss their bake
A part sat on the shelf past its floor life, the kitting clerk could not read the humidity indicator card, and the oven run went ahead. Popcorning shows up later.
Shortages are found at the machine
Kitting counts parts by eye, so the job stops mid-run when a reel empties on the feeder while the missing item is still on order with the distributor.
Rework is invisible
Boards touched up with a soldering iron after inspection are not marked in the record, so a repaired board and a first-pass board look identical to the customer. Yield figures lie.
Follow the work across teams.
This is a planning flow. Confirm the steps, owners and approval rules against your actual operation.
Roles and responsibility boundaries.
Reports your managers need.
- Kits short, by job and part
- First-pass yield by board type and line
- Reels consumed by assembly lot
- Paste jars and stencils nearing limits
- Moisture-sensitive parts by remaining floor life
- Rework by defect type and operator
- Consigned stock held, by customer
Connections to scope
- Component distributor quotation files
- Test equipment result files
- Accounting export
Confirm data access, record ownership and the exchange method for each connection. Inclusion here does not mean every connection is available in a standard package.
Setup decisions and adoption risks.
Use these requirements to plan phases, data migration and user training. Agree the release sequence after reviewing your current systems.
Limitations to settle before implementation
- Makers of the bare boards themselves will find PCB Manufacturer Management Software closer.
- Providers that also source components, build whole products and manage customer forecasts will find Electronic Manufacturing Services Provider Management Software closer.
Modules to consider first.
These functions connect to the operating model above. Confirm each one against the work your business actually runs.
Choose the operation you want to improve.
Use these activities to explain your scope. Your business does not need every function in the directory.
- Prototype and pilot lots for hardware startups
- Turnkey assembly with component sourcing
- Industrial controller and power electronics boards
- IoT and smart meter assembly
- Automotive and EV board assembly
- Functional testing and programming
- Box build with enclosures and wiring
- Long-run production for repeat customers
Explore the business functions.
Production, stock, fleet and recurring billing functions apply only where your business runs those activities. Read the suitability conditions on each page.
Manufacturing
Batch and Serial Tracking
Trace goods using batch identifiers or individual serial numbers.
View workflow and suitability →Bill of Materials
Define the materials and quantities needed for a manufactured item.
View workflow and suitability →Quality Control
Record specified inspections and the disposition of checked goods.
View workflow and suitability →Work Order Management
Track a production job from material issue to completed output.
View workflow and suitability →
Finance & Accounting
Procurement
Inventory Management
Start with the problem your team can describe.
Bring a sample record and show where information is copied, missed or waiting for approval. Scope the first useful change from there.
What happens after you share your requirements
- We review your brief and the systems you already use.
- We clarify the workflow, missing information and the work to consider first.
- The proposed scope sets out the deliverables, responsibilities and dependencies.
- Review the scope and commercial terms before deciding whether to proceed.
Start with your requirements
Describe your current process, the people involved and the change you need. Start with the details you know; we can clarify the rest together.
Share your requirements