Business solutions for Rubber moulding companies
Explore software for work such as “Every drawing answered with a question about the parting line or the tolerance”. Review each business function below, including when it fits and what to check before implementation.
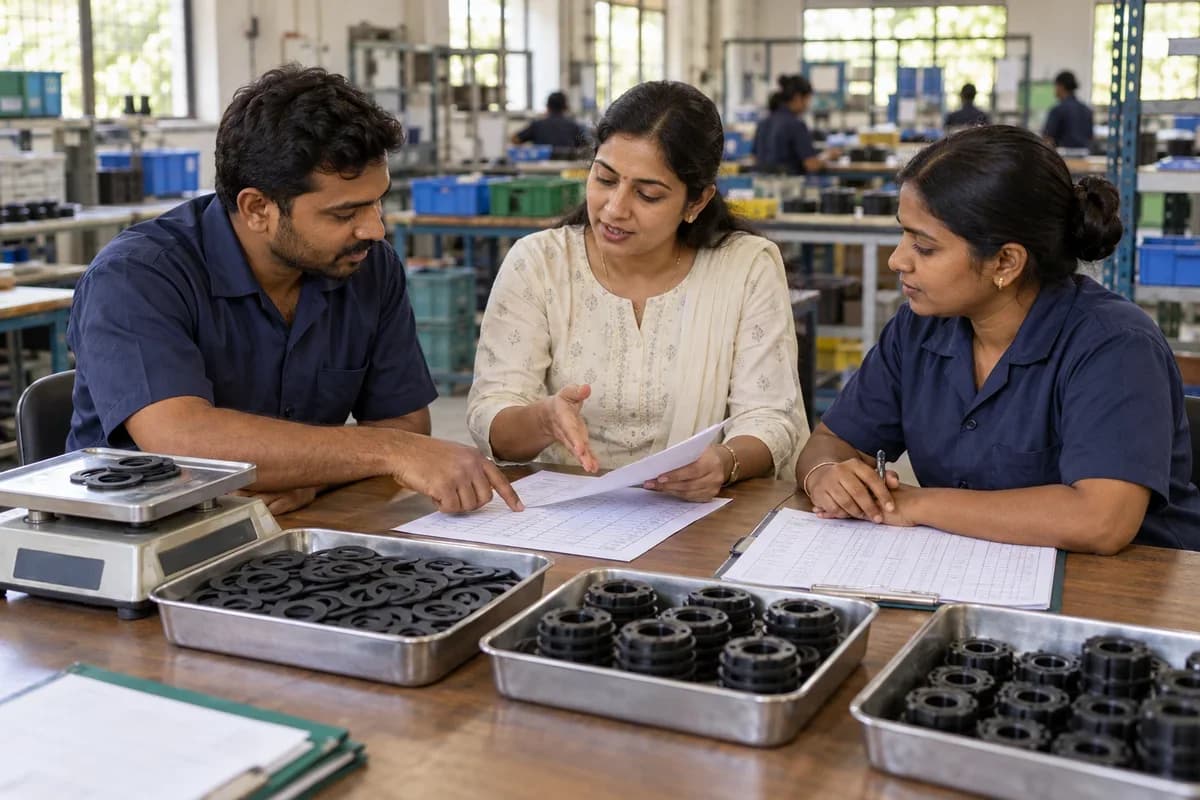
How the business operates.
A rubber moulding shop makes bushes, grommets, bellows, mounts and bonded rubber-to-metal parts. Raw rubber and fillers are mixed into compound on a mill or an internal mixer. Strips or preforms are cut to weight, loaded into a heated mould and cured under pressure. What decides quality is the mix that went in, the cavity that shaped it and how long it sat under heat and pressure.
The records that hold the operation together.
- Enquiries and drawing quotations. Log each buyer drawing and price it from compound cost, preform weight, cure time and cavity count. Every revision of the quote is kept.
- Compound recipes and batches. Hold recipes with polymer, carbon black, filler and curative shares. Record each mix with its rheometer curve, scorch time, hardness and release status.
- Mould and cavity register. Track every mould with cavity count, press fit, shot count since cleaning and repair history. Plating, venting and dowel pin work is logged too.
- Press cure settings. Store time, temperature and pressure for each mould and compound pair, then show them at the press, so the tag on the wall is no longer the record.
- Preform cutting and weights. Record preform weight limits per part. The cutter operator logs checks at the bench scale, and a drifting weight is flagged before short fills reach the cavities.
- Press scheduling and run sheets. Plan orders by press, mould change and compound availability. Log shots, good parts and rejects per cavity on the run sheet.
- Rubber-to-metal bonding records. Record insert type, bonding agent lot and bond test results, such as peel strength, against each batch of bonded parts.
- Trimming and post-cure tracking. Follow parts through deflashing and post-cure oven loads, with times and inspector release.
Operational bottlenecks to check
Compound batches and parts are separate worlds
The mixing room keeps batch sheets and the press operator keeps a shot count, so a rejected bag of bushes has no batch behind it.
Cure settings are chalked on the press
Time and temperature for each mould are written on a tag or in the operator’s head. A new operator runs a different cure and the parts come out under-cured or burnt.
Cavity faults hide in the mix
A damaged cavity makes bad parts in every shot, yet the output from all cavities goes into one bin, so rejects are counted and the cavity behind them is not. Cavities wear out quietly.
Preform weight drifts
Strips are cut by hand or on a cutter and weighed on a bench scale. Too light gives short fills. Too heavy gives flash, extra trimming and wasted compound.
First-off approvals are lost
The buyer’s signed sample and its measurements go into a drawer. A later run is judged against memory rather than the approved piece.
Follow the work across teams.
This is a planning flow. Confirm the steps, owners and approval rules against your actual operation.
Roles and responsibility boundaries.
Reports your managers need.
- Orders by press with compound batch and cure
- Batches released, held and rejected
- Scrap by cause, mould and cavity
- Shots since cleaning by mould
- Compound used against parts moulded
- Bonded part test results by batch
- Buyer balances, oldest due first
Connections to scope
- Rheometer result file import
- Weighing scale input
- Barcode and bag label printing
- WhatsApp or other messaging
- Accounting software export
Confirm data access, record ownership and the exchange method for each connection. Inclusion here does not mean every connection is available in a standard package.
Setup decisions and adoption risks.
Use these requirements to plan phases, data migration and user training. Agree the release sequence after reviewing your current systems.
Limitations to settle before implementation
- A shop that moulds a few samples a month on one press can work from a job book.
- Cutters of gaskets from sheet will find Rubber Gasket Manufacturer Management Software closer, and makers of O-rings and seals may prefer Seal and O-ring Manufacturer Management Software.
Modules to consider first.
These functions connect to the operating model above. Confirm each one against the work your business actually runs.
Choose the operation you want to improve.
Use these activities to explain your scope. Your business does not need every function in the directory.
- Every drawing answered with a question about the parting line or the tolerance
- Tool cost and piece price explained in one clear sheet
- Vendor registration with auto, appliance and pump makers
- First article and sample approval chased with the customer's quality team
- Rubber-to-metal bonding shown as a second family beside plain moulded parts
- Customer-owned tools in your shop turned into a second part family
- Overseas buyers who source rubber parts from India
- Tool room and mould repair offered as its own service
Explore the business functions.
Production, stock, fleet and recurring billing functions apply only where your business runs those activities. Read the suitability conditions on each page.
Manufacturing
Batch and Serial Tracking
Trace goods using batch identifiers or individual serial numbers.
View workflow and suitability →Bill of Materials
Define the materials and quantities needed for a manufactured item.
View workflow and suitability →Production Planning
Plan manufacturing quantities against demand, materials and capacity.
View workflow and suitability →Quality Control
Record specified inspections and the disposition of checked goods.
View workflow and suitability →Work Order Management
Track a production job from material issue to completed output.
View workflow and suitability →
Assets and Fleet
CRM
Inventory Management
Start with the problem your team can describe.
Bring a sample record and show where information is copied, missed or waiting for approval. Scope the first useful change from there.
What happens after you share your requirements
- We review your brief and the systems you already use.
- We clarify the workflow, missing information and the work to consider first.
- The proposed scope sets out the deliverables, responsibilities and dependencies.
- Review the scope and commercial terms before deciding whether to proceed.
Start with your requirements
Describe your current process, the people involved and the change you need. Start with the details you know; we can clarify the rest together.
Share your requirements